Ribbing is back on the runway. And it’s showing up in an unexpected place: the cuff, the collar, the hem. Spring/Summer 2027 knitwear leans hard into edge detailing. That shift puts pressure on the cutting room, not just the design studio.
What is a collarette trim and why is it trending in 2027? A collarette trim is a ribbed knit band. It’s cut from tubular fabric and sewn onto a cuff, collar, or hem for stretch and structure. It’s trending in 2027 because designers favor edge detailing over heavy, all-over patterns. Ribbing delivers texture exactly where it needs to sit.
Why are ribbed cuffs and collars trending in 2027?
A return to craftsmanship
Fashion forecasters call this season a return to craftsmanship. Trend analysts at POP Fashion describe Spring/Summer 2027 knitwear as centered on detailed stitching. That stitching concentrates at the edges of a garment, not across the whole piece. Cuffs, hems, and necklines get the attention, while the body of the garment stays simple.
Why manufacturers should pay attention
This shift matters for manufacturers. A ribbed cuff or collar does real structural work. It holds a sleeve or neckline in place, without a zipper, button, or drawstring. So when a trend calls for that detail on nearly every piece, cutting rooms need a fast, consistent way to produce it.
Trend forecasting platform Trendalytics also points to a broader move toward relaxed silhouettes and natural texture. This spans Spring 2027 runways, from Milan to Copenhagen to Tokyo. Ribbing fits neatly into that story. It’s tactile, and it reads as considered rather than mass-produced. It also works across nearly every knitwear category, from athleisure to elevated basics.
What machine makes collarette trims?
How the cutting process works
A collarette cutting machine converts tubular knit fabric into ribbed bands. These bands get sewn onto a cuff, collar, or waistband. First, the tube feeds onto a rotating turntable. Then a blade slices continuous, uniform bands as the table turns. Band width is set before the fabric touches the blade. As a result, every strip comes off at the same measurement, cut after cut.
Semi-automatic vs. fully automatic
Two broad categories exist. Semi-automatic machines need an operator to load the fabric and start the cycle, then step back while the machine cuts. Fully automatic machines add more: PLC-driven speed synchronization, auto-stop sensors, and higher throughput. This suits manufacturers running long production runs of the same trim.
Both approaches produce the same result: a clean, ribbed band with a consistent width. However, they differ in speed, automation, and how many bands a single pass can cut. That’s exactly what separates Svegea’s EC-series models from each other.
How do I choose between the EC300, EC200C, EC200CS and EC50?
Svegea builds four collarette cutting machines. Together, they cover everything from small-batch production to high-speed, high-volume cutting. The table below breaks down what each one handles.
| Model | Automation | Bands per pass | Band width | Max speed | Best for | Learn more |
|---|---|---|---|---|---|---|
| EC 50 | Semi-automatic | 2–3 (4 with extra knife unit) | 16–140 mm | Up to 30 m/min | Small to mid-size production, hands-on operation | svegea.se/product/ec-50-semi-automatic/ |
| EC 200C | Fully automatic | 3 (4 with extra knife unit) | 16–170 mm | Up to 40 m/min | Mid-volume runs needing zero-waste, hands-off cutting | svegea.se/product/euro-collarette-200c/ |
| EC 200CS | Fully automatic | 4 (5 with extra knife unit) | 16–260 mm | Up to 60 m/min | Wider bands at high speed, PLC-synced production | svegea.se/product/euro-collarette-200cs/ |
| EC 300 | Fully automatic | 4 (5 with extra knife unit) | 16–170 mm | Up to 60 m/min | High-volume runs needing both scissor and crush cutting | svegea.se/product/euro-collarette-300/ |
Matching a machine to your production
On the EC50, operators cut up to three bands at once. A fourth band is possible with an added knife unit. It’s a solid starting point for manufacturers who don’t yet need full automation. Meanwhile, the EC200C is built for zero-waste, fully automatic cutting once a job is set up. That makes it a natural step up for mid-volume runs of a single trim width.
The EC200CS handles wider bands, up to 260 mm, without needing a second machine. So it suits collections that mix narrow cuffs with wider waistbands in the same run. On the EC300, manufacturers get both scissor and crush cutting. This gives more control over edge finish, especially when a collection spans different fabric weights.
Weighing speed against cost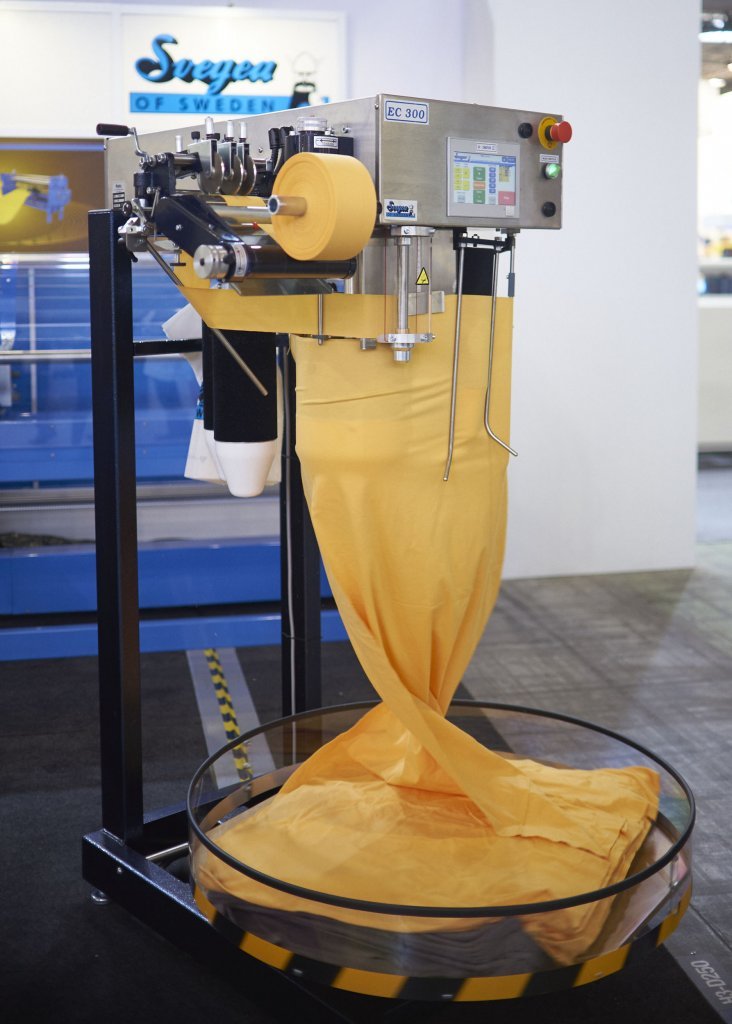
Speed is capped at 30 m/min on the EC50, since an operator manually manages the load and finish. By contrast, the three fully automatic models run two to four times faster. Their fabric feed, cutting speed, and stop points sync automatically. If your 2027 lineup leans on one or two standard rib widths at moderate volume, the EC200C is the more economical fit. However, if widths vary across styles, or volume is climbing fast, the EC200CS or EC300 earn back their higher price point in throughput.
Ready for the ribbing comeback
Ribbing isn’t a passing microtrend. It’s shaping up to be one of the defining details of 2027 knitwear. Manufacturers who can produce consistent, high-quality collarette trims at scale will keep up with buyer demand. Every EC-series machine is engineered in Sweden, with cutting components made from high-grade steel. So the choice mostly comes down to volume and bandwidth, not build quality.
See the full lineup and specs in the Collarette Range Family brochure. For a side-by-side look at every semi-automatic and fully automatic model, visit svegea.se/collarette-cutting-machines/.
Follow Svegea on Instagram, LinkedIn, and Facebook (@svegeaofsweden) for more updates on efficient, sustainable garment and textile manufacturing machinery.
FAQ
What is a collarette trim?
A collarette trim is a ribbed knit band. It’s cut from tubular fabric and used on cuffs, collars, and hems for stretch and structural finishing.
Why is ribbing trending in fashion for 2027?
Spring/Summer 2027 knitwear favors detailed stitching at the edges, not all-over patterns. Ribbed cuffs, collars, and hems fit that trend directly.
What’s the difference between a semi-automatic and fully automatic collarette machine?
A semi-automatic machine, like the EC50, needs an operator to load fabric and start each cycle. Fully automatic models, like the EC200C, EC200CS, and EC300, add PLC-driven speed sync and auto-stop sensors for continuous, hands-off cutting.
Which EC-series machine cuts the widest bands?
The EC200CS cuts bands up to 260 mm wide, the widest range in the current EC lineup.
Do I need a fully automatic machine for small production runs?
Not necessarily. The EC50 handles small to mid-size runs well, and it costs less to start with. Fully automatic models pay off once volume or band-width variety increases.
Sustainable Fabric Cutting Technology
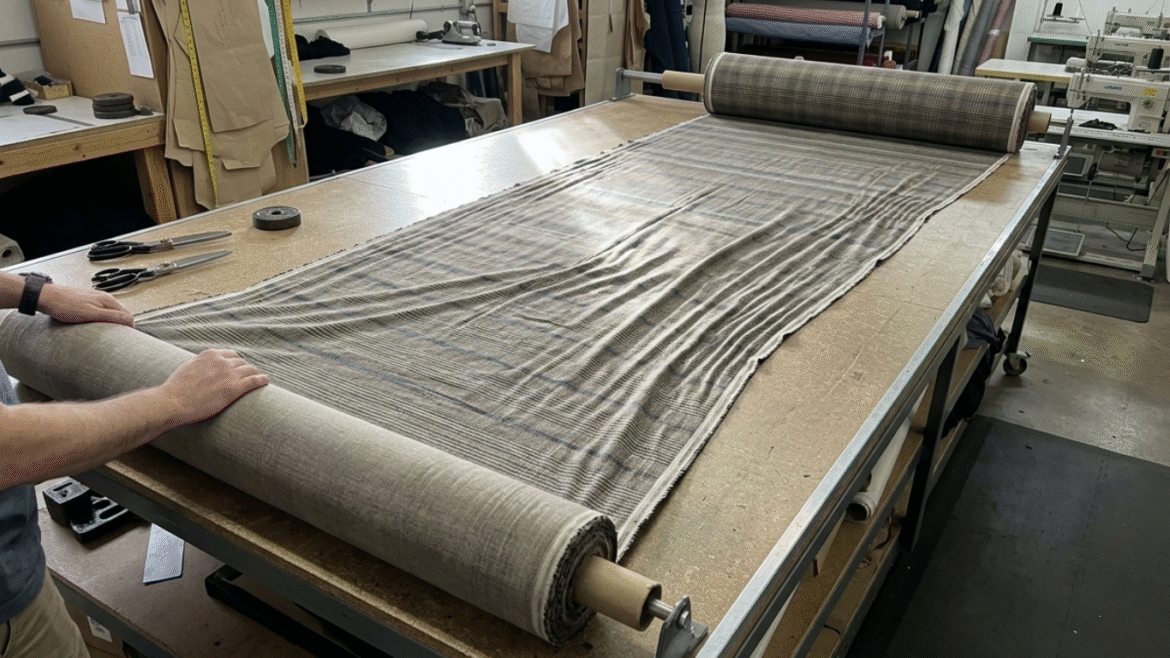
Fabric relaxing is a pre-cutting step that lets rolled fabric rest under controlled, tension-free conditions before it reaches the cutting table. A fabric relaxing machine unwinds the roll, releases the internal stress built up during knitting, dyeing, or transport, and lets the material settle into its true dimensions. This one step cuts pattern distortion, lowers reject rates, and reduces textile waste in manufacturing. Heading into 2027, it’s one of the more practical sustainability upgrades a cutting room can make.
What causes fabric waste in cutting rooms?
Knitting, dyeing, and transport all put significant tension on rolled fabric. Winding a roll tightly, dyeing it under heat, or shipping it across the country all pull and stretch the material in ways the eye can’t see. The fabric holds this tension until something releases it. If nothing does, the release happens on the cutting table — or worse, after workers sew the garment.
Here’s the practical problem this creates. A cutter lays fabric flat and cuts it to a pattern while the material is still under tension. Once it’s off the table, the fabric relaxes and pulls back toward its natural shape. Panels that looked perfect during cutting shrink, skew, or twist. Seams no longer align. The finished garment may pucker, sag, or fit incorrectly after its first wash, and none of this shows up until it’s expensive to fix.
Knit fabrics and stretch wovens with spandex or Lycra content are especially prone to this problem, because their fibers hold tension longer than rigid wovens do. Circular knits add another layer of risk: cutting teams slit the tube open and spread it flat before cutting, and that extra handling step introduces skew on top of existing distortion.
The financial impact is larger than most cutting rooms assume. Fabric waste in cutting rooms typically runs 10% to 20% of total material, according to Lectra, and fabric alone often accounts for more than half of a garment’s total cost. Even a small improvement in fabric utilization translates directly into lower material spend and less waste headed to landfill or recycling.
How does fabric relaxing reduce waste?
A fabric relaxing machine addresses the problem at its source, before the fabric ever reaches the marker table. Instead of cutting a stressed, distorted roll and hoping for the best, the fabric first travels through a relaxing unit that unwinds it slowly, removes tension through mechanical rollers or controlled airflow, and lets the fibers settle back into their natural, balanced state.
Once the fabric relaxes, its true dimensions return, and cutters can follow the fabric’s actual grain instead of a stretched, temporary one. That single change has a ripple effect across the whole production line:
- Fewer distorted panels means fewer rejected pieces and less scrap fabric.
- Consistent dimensions mean tighter marker efficiency, so planners can nest patterns closer together without leaving a safety margin for shrinkage.
- Fewer post-wash surprises mean fewer returns and less rework, which saves fabric that would otherwise go into a second cut.
- Stable, tension-free feeding protects delicate or elastic fabrics from stretching, snagging, or fraying at the edges.
In short, fabric waste drops when cutting rooms remove tension before the fabric reaches the marker table, and manufacturers get more usable garment pieces out of every roll they buy. Operators feed a well-relaxed roll into the spreader without added stress, so what a planner sees on the marker is what the sewing line actually gets.
Which fabric relaxing machine fits my production volume?
Svegea builds fabric relaxing machines for a range of production volumes and fabric types, from standard knit-and-woven operations to high-speed, air-assisted lines handling delicate stretch textiles. The table below compares the current lineup so you can match a machine to your cutting room’s needs.
| Model | Best for | Relaxing method | Key feature | Learn more |
| CR210 | Standard-volume cutting rooms | Stepless electronic speed control with an oscillating fold system | Photocell loop control for smooth, tensionless feeding | svegea.se/product/cr210-fabric-relaxing-machine/ |
| CR210A | Higher-precision cutting rooms needing tighter edge control | Same tensionless feeding as the CR210, plus automatic edge alignment | Integrated automatic edge alignment device | svegea.se/product/cr210a-fabric-relaxing-machines/ |
| CRX Air Relaxing Series | High-speed lines and delicate stretch fabrics (jersey, lycra, technical textiles) | Dual independent air-flotation zones instead of mechanical rollers | PLC control, automatic width measurement, speeds up to 40 m/min | svegea.se/product/fabric-relaxing-machine-crx-air/ |
The CR210 suits standard-volume cutting rooms that need dependable, tensionless feeding without a large equipment footprint. The CR210A builds on that same platform and adds an automatic edge alignment device for manufacturers who need tighter tolerance control on wide or high-value fabric runs. The CRX Air Relaxing Series runs on controlled airflow instead of mechanical rollers, which makes it the better fit for lightweight knits, lycra blends, and other fabrics that stretch or curl easily under physical contact.
A quick note on model selection: Svegea’s current fabric relaxing lineup covers these three machines. If you were comparing a “CR205” model, double-check the spec sheet or brochure you’re working from — it doesn’t currently appear as an active model on svegea.se, and the closest equivalent for lighter, standard-volume applications is the CR210.
Sustainability impact
The stakes go beyond one cutting room. The fashion industry loses the equivalent of one garbage truck of textiles to landfill or incineration every second worldwide, and recyclers turn less than 1% of clothing back into new garments, according to the Ellen MacArthur Foundation. Preventing waste at the cutting stage keeps material out of that stream entirely.
Regulation is starting to reflect this. In Europe, manufacturers and retailers destroy an estimated 4% to 9% of the textile products they place on the market before anyone ever uses them, according to the European Environment Agency. That data helped shape the EU’s Ecodesign for Sustainable Products Regulation (ESPR), which bans large companies from destroying unsold textiles starting in July 2026. Manufacturers who cut waste upstream, at the cutting table, stand in a stronger position for this kind of policy shift than those relying on downstream fixes.
Fabric relaxing also supports a “cut it once” mindset. When pattern pieces hold their shape after cutting, fewer garments need rework, fewer rolls need re-ordering to cover shrinkage losses, and manufacturers waste less packaging, transport, and processing on fabric that never becomes a finished product. For a fashion industry under growing pressure to show measurable sustainability progress by 2027, this kind of upstream fix is one of the more cost-effective places to start.
Not inevitable
Cutting-room waste isn’t inevitable — it’s largely a tension problem, and tension is solvable before the fabric ever meets the blade. A fabric relaxing machine gives manufacturers a practical, proven way to stabilize material, protect pattern accuracy, and reduce textile waste in manufacturing without slowing down production.
To see the full fabric relaxing lineup, product brochures, and specifications, visit our Fabric Relaxing Series page. For more on fabric shrinkage and pre-cutting prep, read svegea.se/prevent-fabric-shrinkage/. Contact us for a product demo!
FAQ
What is fabric relaxing in textile manufacturing?
Fabric relaxing is a pre-cutting process that removes internal tension from rolled fabric so it can settle into its natural, stable dimensions before spreading and cutting.
Why does fabric shrink after cutting if it was measured correctly?
Most likely, the fabric went through cutting while still under tension from knitting, dyeing, or transport. Once it’s off the cutting table, that tension releases, and the material shrinks or shifts out of shape.
How much fabric waste can a relaxing machine actually prevent?
Results vary by fabric type and production setup, but since cutting-room waste typically runs 10% to 20% of total material (www.lectra.com), even a modest reduction in distortion-related waste can meaningfully lower material costs.
Do all fabric types need relaxing before cutting?
Knit fabrics and stretch wovens with spandex or Lycra content benefit the most, since their fibers hold tension longer. Rigid wovens still benefit, but usually need shorter relaxing cycles.
What’s the difference between fabric relaxing and pre-shrinking?
Pre-shrinking uses washing or steaming to shrink fabric before cutting, which works but takes time and adds cost. Relaxing lets the fabric settle naturally, without added moisture or heat, which is faster and gentler on delicate materials.
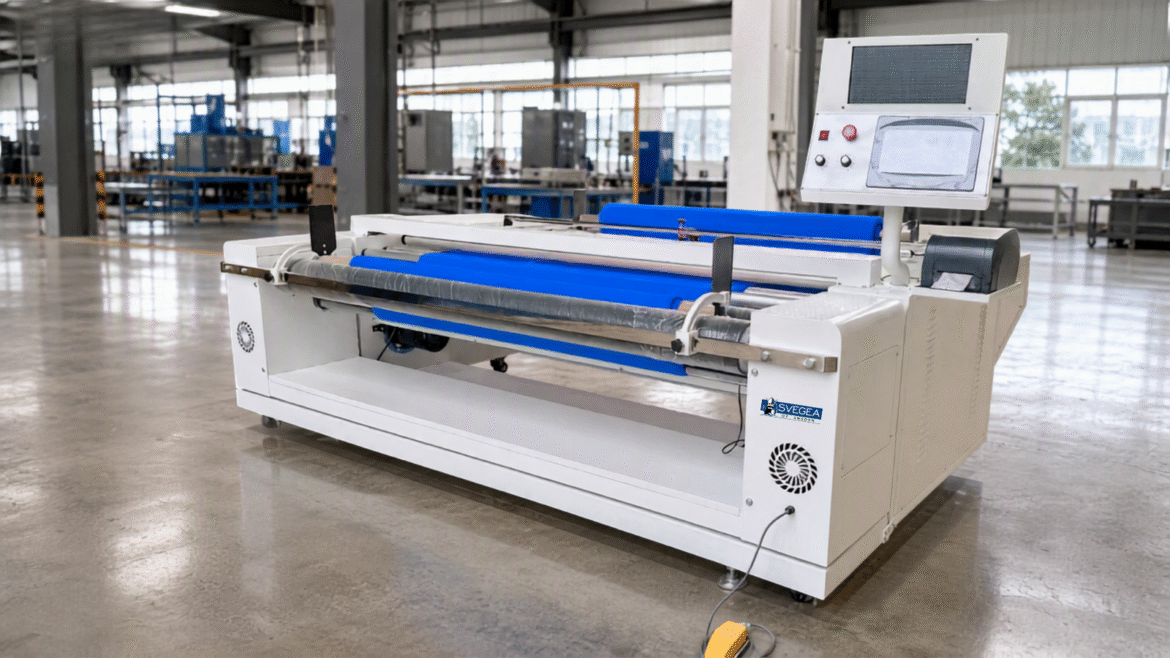
Garment factories are changing faster than most buyers realize. Machines now handle jobs that used to take several pairs of hands, and cutting rooms are quietly becoming the most technical part of the whole production line. For manufacturers planning capacity for 2027, that shift is worth understanding now.
The top textile manufacturing trends for 2027 are automation in trim and collarette production, gentler air-based fabric relaxing, waste reduction built into the cutting process, and modular machines that adapt to more than one job. Together, these trends point toward factories that produce more, waste less, and rely less on manual labor to stay consistent.
What Is Driving Automation in Textile Trims?
Labor costs are rising, and buyers expect tighter quality control than ever before. Because of this, semi-automatic trim machines are becoming standard rather than a premium upgrade. A machine like the EC50 Semi-Automaticlets one operator load fabric and start a cutting cycle that runs on its own, cutting labor time without cutting corners on precision.
The payoff shows up in the numbers. According to a 2026 garment manufacturing market report, automation in stitching and cutting has already improved productivity by 18% and reduced waste by 11% industry-wide. That kind of gain is hard to ignore for factories competing on both speed and cost.
High-precision collarette machines are following the same path. The EC300 Euro Collarette is built to hold consistent trim width across long runs, which matters more as brands demand uniform quality across bigger batches.
How Is Fabric Relaxing Getting Gentler?
Fabric that’s cut under tension often shrinks or distorts later, and that problem has quietly cost manufacturers money for years. In 2027, expect more factories to add a relaxing step before cutting, and to do it with less mechanical stress on the fabric.
Air-based relaxing is leading that change. The CRX Air Relaxing Series uses contact-free air technology instead of rollers, which reduces distortion in delicate knits. It’s a small step in the process, but it prevents costly rework further down the line.
Why Is Waste Reduction Now a Core Trend, Not an Afterthought?
Sustainability pressure isn’t new, but it’s becoming more concrete. Fabric waste is being treated as a production cost to eliminate, not just an environmental talking point. Systems that combine cutting, folding, and winding in one pass – like the Complete Bias System – cut down on offcuts and reduce the handling steps where fabric typically gets damaged or wasted.
This trend also connects back to relaxing and trim precision. A cleanly relaxed, evenly cut fabric produces fewer rejected panels, and fewer rejected panels means less fabric bought and discarded in the first place.
Why Are Modular, Accessory-Based Machines Gaining Ground?
Manufacturers no longer want a machine that does one job well. They want equipment that adapts as orders change. Accessory kits, like the ones now available for the EC200C, let a single collarette machine produce multiple trim widths and styles without buying separate equipment for each style.
This flexibility matters most for mid-size manufacturers, who need to serve varied customer demands without the capital cost of a large, specialized machine fleet.
What This Means for Your Production Line
None of these trends work in isolation. Automation improves speed, gentler relaxing protects fabric quality, waste reduction protects margins, and modular machines protect flexibility. Manufacturers who treat these as one connected strategy – rather than four separate purchases – will be better positioned heading into 2027.
If you’re mapping out equipment upgrades for the year ahead, contact the Svegea team to talk through which machines fit your production line.
FAQ
- What is the biggest textile manufacturing trend for 2027?
Automation in trim and cutting is the trend with the broadest impact, since it affects speed, labor cost, and consistency at once. - Does automation reduce fabric waste?
Yes. Automated, precision-cut trims and relaxed fabric both reduce the number of rejected panels, which lowers overall fabric waste. - What is fabric relaxing and why does it matter?
Fabric relaxing removes tension from a fabric roll before cutting. It’s important because fabric cut under tension tends to shrink or shift shape after cutting, causing quality issues later. - Are modular machines worth it for smaller manufacturers?
Often, yes. A modular machine with accessory kits can replace several single-purpose machines, which lowers equipment costs for manufacturers producing varied trim styles. - How can I prepare my factory for these 2027 trends?
Start by identifying where manual handling causes the most waste or inconsistency – usually trim cutting or fabric relaxing – and evaluate equipment built for that specific step.
Autumn is creeping back in, and with it, the trench coat is coming out of storage again. Scroll through any fashion feed right now and you’ll see it: belted, oversized, thrown over a slip dress or buttoned up over a suit. It never really goes away, but every September it seems to reintroduce itself as the season’s must-have layer.
We’ve watched this coat cycle through fashion for years from our side of the industry — the manufacturing side. And here’s the thing most style articles won’t tell you: the reason a good trench coat still looks sharp after a decade of wear has almost nothing to do with the belt or the buttons everyone photographs. It’s buried inside the collar, the lapel, and the lining, in a set of narrow fabric strips most wearers never think about.
A Coat Built Like a Small Structure
Thomas Burberry patented gabardine back in 1879, engineering it specifically to be waterproof without the stiffness of rubberized rainwear. That original goal — weather resistance without bulk — is still what separates a real trench coat from a coat-shaped raincoat. But weatherproof fabric alone doesn’t explain why a well-made trench holds its collar stand or keeps its lapels from curling after years of use.
That comes down to internal reinforcement: collar stays, lapel interlining, and the strapping used for belts and epaulettes. Unlike a lightweight dress or blouse, a trench coat carries real structural weight. Heavy gabardine, dense twill, sometimes multiple bonded layers — none of it behaves the way thin fabric does under a sewing machine, and none of it forgives sloppy internal construction.
So while the outer fabric gets all the design credit, it’s these hidden strips of interlining and tape that decide whether the coat ages gracefully or starts sagging at the shoulders by its second winter.
What Those Hidden Strips Actually Do
A few things happen when a manufacturer gets this part right:
- The collar stands up crisply instead of collapsing, even on a heavy double-layered lapel.
- Belt loops and cuff straps stay straight and don’t twist over time.
- The fabric doesn’t fray internally where it’s under the most tension — shoulders, waist, collar edge.
- The coat keeps its shape wash after wash, season after season.
None of this shows up in a product photo. You notice it later, the first time you flip your collar up against a cold wind and it actually stays put.
Where Hand-Cutting Runs Out of Road
A skilled tailor working on a single bespoke coat can cut collar stays and waist strapping by hand, with shears and a steady eye. It works, at that scale.
It doesn’t work at factory scale. Once a manufacturer is producing thousands of coats a season, hand-slitting heavy rolls introduces the kind of inconsistency that ruins a production run: frayed edges from blade friction, strips that come out a millimeter or two off-width, automated sewing lines thrown out of alignment because the input material isn’t uniform. Multiply a small error by ten thousand units and it stops being small.
This is the point where most outerwear manufacturers move to dedicated slitting equipment. And it’s the part of the process we spend most of our time thinking about.
Where We Come In
At Svegea, we build roll slitting and band cutting machines designed around exactly this problem: cutting dense, heavy fabric into narrow, consistent strips without the fraying, stretching, or width drift that ruins a production batch.
A few things our machines are built to handle:
1. Consistent width across the whole roll. The strip you cut at meter one should match the strip at meter one thousand.
2. Clean edges on dense material. Automatic blade sharpening keeps friction and heat from fraying heavier fabrics like gabardine or bonded interlining.
3. Tension control that doesn’t distort the weave. Heavy woven fabric under the wrong tension stretches unevenly, and that shows up later as puckering.
We didn’t design this equipment with trench coats specifically in mind — it’s used across tailored blazers, technical rainwear, and industrial textiles too — but outerwear is where the margin for error is smallest. Dark, structured coats show every flaw in daylight.
The Part Nobody Photographs
There’s a reason this kind of detail rarely makes it into a fashion write-up. It’s not glamorous. Nobody’s Instagramming a roll of interlining tape. But it’s the difference between a coat that’s still in rotation a decade from now and one that’s in a donation bag by next spring.
If you’re on the manufacturing side and dealing with fraying, width inconsistency, or waste on heavy-fabric roll slitting, it’s worth a conversation — we’ve spent a long time solving exactly this problem. You can reach our engineering team through svegea.se, or explore the equipment lineup on the same site.
Either way, next time you flip up a trench coat collar against the wind, you’ll know what’s actually holding it there.
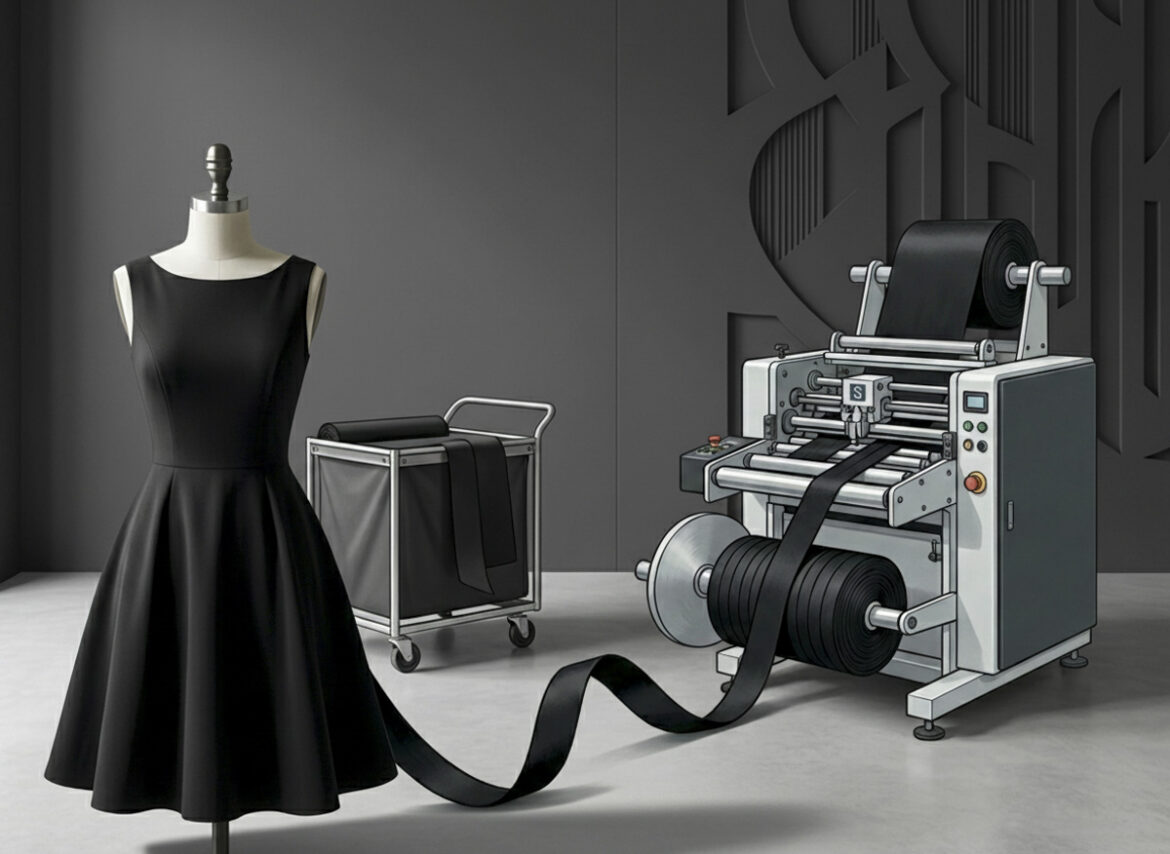
Little did Givenchy know that the little black dress he designed for Audrey Hepburn would become an essential piece in nearly every woman’s wardrobe, generations after Breakfast at Tiffany’s first hit the screen.
The Little Black Dress, or LBD, has since become fashion’s great equalizer — a single garment that flatters every shape, suits every occasion, and never goes out of style. It gets you through a chaotic morning, an unplanned dinner date, or a job interview with equal ease. Match it with a denim jacket and flats for class, add a statement necklace for a night out, or pair it with a tailored blazer to walk into an interview with confidence. Few garments do so much with so little.
But here’s what almost no one talks about when they praise the LBD’s timeless silhouette: why does a well-made black dress hold its shape, drape cleanly around the neckline, and outlast a decade of wear — while a cheaper version puckers, frays, and loses its form after a few washes?
The answer isn’t the fabric. It isn’t even the cut. It’s what happens at the edges.
The Finishing Technique You Never Notice — Until It’s Missing
Every curved seam, every clean neckline, every armhole that sits flat against the skin instead of gapping or rolling — all of it depends on a technique called bias binding.
Bias binding is a strip of fabric cut on the diagonal, or “bias,” of the material rather than along the straight grain. Cutting fabric this way gives the strip natural stretch and flexibility, which means it can wrap smoothly around curves — necklines, armholes, hems — without puckering or stretching out of shape. It’s the difference between a seam that looks handmade and one that looks engineered.
In garment manufacturing, bias binding does more than finish an edge. It:
- Reinforces stress points so seams don’t tear under movement
- Hides raw edges for a clean, professional interior finish
- Adds structure to curved lines that straight-grain fabric simply can’t follow
- Extends the garment’s lifespan, which is exactly why a well-made LBD from ten years ago can still look as sharp as the day you bought it
It’s a small detail with an outsized effect on perceived quality — the kind of thing a customer can’t always name, but instantly feels when they try on a dress that’s been finished properly.
From Sewing Room to Factory Floor
Home sewists can easily cut bias tape by hand. A simple fold, a quick press with an iron, and they’re done. But scale that up to a commercial factory. Imagine producing thousands of little black dresses every single season.
At that volume, manual cutting fails instantly. Speed drops. Fabric waste spikes. Consistency disappears completely. Manufacturers need a real engineered solution.
That’s where Svegea of Sweden enters the picture. We’ve spent decades perfecting industrial bias binding systems.
Engineers built Svegea’s Bias System specifically for garment manufacturing automation. At full production scale, it transforms massive fabric rolls into continuously sewn bias binding.
The process starts fast. First, the Tube Sewing Unit transforms open fabric into a continuous tubular piece. Next, the Bias Cutter and Winder opens and rewinds the material into an open-width roll. This prepares the fabric for precise slitting. The system handles everything smoothly, cutting delicate 6mm trims as easily as wide structural bindings for heavy fabrics.
The result? Perfect bias binding from the first meter to the ten-thousandth. No manual process can compete with that level of accuracy.
Why This Matters Beyond the LBD
Bias binding isn’t just for little black dresses. It shows up everywhere garments need clean, durable, curve-friendly finishes. You’ll find it on blouses, activewear, and children’s clothing. It even elevates non-apparel items like bags and home textiles.
Still, the classic LBD remains the ultimate quality test. Buyers expect to wear it for years. Its dark color exposes every single flaw in construction, leaving zero room for sloppy seams.
That’s what separates cheap clothing from true quality. One piece looks nice on a hanger. The other still looks pristine after fifty washes.
It all comes down to finishing. Top manufacturers rely on precision textile cutting systems to guarantee flawless results every time.
The same logic applies across the entire factory floor. Modern facilities deploy collarette cutters for waistbands and roll slitters for large fabric rolls. Precision machinery eliminates human error, keeps waste low, and guarantees consistent quality across every batch.
The Takeaway
The next time you slip into a little black dress that fits like a dream—just like the day you bought it—you’re rocking pure engineering genius. That pristine neckline and those crisp, fray-free seams surviving a decade in rotation don’t happen by accident. Every iconic silhouette relies on high-precision manufacturing, where seamless consistency turns basic threads into forever fashion.
Svegea’s Bias System and cutting machines give garment manufacturers a distinct competitive advantage through unmatched precision.
The cutting room rarely gets the credit it deserves. Dyeing, weaving, and finishing tend to dominate the sustainability conversation. Yet, the cutting stage quietly determines how much of every roll actually becomes a garment — and how much becomes trim on the floor. At Svegea, we have spent decades building the machines that sit at exactly that point in the process. Over that time, we’ve watched “zero waste” shift from a nice-to-have talking point to a real production target. This article walks through why that shift matters and what it looks like in practice.
The Hidden Cost of the Cutting Room
Textile waste is a big number, and it keeps getting bigger. According to the UN Environment Programme, the fashion industry generates roughly 92 million tonnes of textile waste every year. If nothing changes, that figure will climb past 134 million tonnes by 2030. The Ellen MacArthur Foundation puts it even more starkly: factories landfill or burn the equivalent of one garbage truck of clothing every single second.
Most of that conversation focuses on what happens after a consumer wears and discards a garment. Fair enough — that is where the largest volumes sit. But a meaningful share of textile waste never reaches a consumer at all. Factory floors generate this waste during cutting, trimming, and slitting, long before workers sew a single stitch. Offcuts, mismatched widths, and torn edges from tension problems all add up. Multiply that by thousands of meters a day, and the scrap bin becomes a genuine line item, not a rounding error.
What “Zero Waste” Actually Means on the Factory Floor
Zero waste doesn’t mean zero scrap. Realistically, some trim loss is unavoidable in any cutting process. Instead, it means designing the workflow so that you minimize waste at every step, measure it consistently, and — wherever possible — recover rather than bin it. For manufacturers, that translates into three practical questions:
- How much material do you lose to trim, misalignment, or edge damage during cutting?
- How repeatable is that loss across shifts, operators, and fabric types?
- Where can better equipment, not just better habits, close the gap?
That third question is where the technology conversation begins, and it is the one we spend most of our time thinking about.
Where Precision Cutting Technology Makes the Difference
Fabric doesn’t behave the same way twice. Tension varies by fibre, roll, humidity, and even the time of day. When a machine can’t compensate for that variability, the operator ends up compensating instead — usually by cutting a little wide “to be safe.” That habit, repeated across a full production run, is one of the most common sources of avoidable scrap in a cutting room.
Automated, electronically controlled cutting systems close this exact gap. Precise tension regulation keeps fabric feeding evenly, so the blade meets the material at a consistent width instead of a guessed one. Preset cut-width recipes remove the manual recalibration that eats into a shift’s productive time. Meanwhile, photocell edge alignment catches drift before it turns into a rejected panel. On the slitting side, PLC-controlled systems with stored cutting programs mean a changeover doesn’t require re-learning the machine from scratch. This cuts down on the “test cuts” that used to go straight into the scrap pile.
None of this is theoretical for us. It is the engineering problem we have worked on since 1952, first with collarette band-cutting machines and later across bias binding and roll-slitting equipment. Every refinement — a floating tension arm here, an automatic blade sharpener there — exists because a manufacturer somewhere told us their waste percentage was too high and asked what we could do about it.
Practical Steps Manufacturers Can Take This Quarter
Reducing cutting-room waste doesn’t require a full equipment overhaul to start. A few steps tend to produce results quickly:
1. Audit trim loss by fabric type, not just by line. Knits, wovens, and bias-cut materials behave differently, and averaging them together hides where the real losses sit.
2. Track waste as a percentage of output and review it weekly rather than quarterly. You can catch small drifts more easily — and fix them more cheaply — before they become the new normal.
3. Standardize cut-width settings across shifts so the outcome doesn’t depend on which operator runs the machine that day.
4. Service blades and tension systems on a schedule, not just when a problem shows up. A dull blade or a slack tension arm is a slow, invisible source of scrap.
5. Treat offcuts as an input, not an ending. Even if you haven’t built recycling into the workflow yet, sorting scrap by fibre type keeps that option open for later.
Individually, these steps sound modest. Together, over a year of production, they tend to move the needle more than most manufacturers expect.
Looking Ahead
The pressure on manufacturers to reduce material waste isn’t going away. If anything, tightening EU extended producer responsibility rules and growing retailer sustainability requirements are turning it into a compliance issue as much as a cost issue. Organizations like Textile Exchange continue to push the industry toward circularity. The manufacturers who get ahead of that curve, rather than reacting to it, tend to be the ones with cutting-room data already in hand.
We don’t think there’s a single fix for textile waste — it is a supply chain problem, and it needs supply chain-wide solutions. But the cutting room is one of the few places where a manufacturer has direct, immediate control over how much material becomes product versus how much becomes scrap. It is worth treating that way.
If your team is looking at cutting-room waste numbers and wondering what is realistic to improve, we are happy to talk through it. Reach out to Håkan Steene at h.steene@svegea.se for a waste-reduction consultation — no pitch, just a conversation about where the losses might be coming from.
—
Svegea of Sweden has designed and manufactured band-cutting, bias binding, and roll-slitting machinery since 1952. Learn more at svegea.se.
The Silent Language of Textiles
TL;DR: Touch is the first sense you ever develop, and fabric never stops talking to it. Long after you’ve stopped noticing color or cut, texture is still quietly running the show, calming a classroom, steadying a hospital ward, convincing a hotel guest they’ve arrived somewhere special. The science backs this up. So does the machinery that keeps a fabric’s feel consistent, batch after batch.
Touch Talks First, and It Never Really Stops
Run your hand across cashmere, then linen, then a coarse wool blanket. You don’t need a vocabulary lesson to know how each one makes you feel. Your body reacts before your brain finishes the sentence.
That’s not a coincidence. It’s a nine-month head start.
Touch is the first sense to develop in the womb, arriving around the eighth week of gestation, well before sight, hearing, or the ability to have an opinion about anything. Sensory receptors wake up first around the mouth and nose, then spread across the rest of the body over the following weeks. By the time a baby takes its first breath, touch already has months of practice logged. Fabric just keeps that conversation going.
Why Texture Beats Color to the Punch
Marketing teams love a good color story, and fair enough, color is loud and photogenic. But texture works in a quieter room: your nervous system, which reacts before your conscious mind gets a vote.
A 2024 study in PLOS ONE measured how tactile sensitivity shapes the way people rate fabric texture, confirming what mills have long suspected by feel alone: touch perception can be measured and predicted, not just guessed at.
Research published in the Spanish Journal of Marketing pushed the point further. After interviewing industry experts, the authors found that of the four qualities people notice by touch- texture, weight, temperature, and hardness- texture dominates how a product gets judged in someone’s hands. Shoppers decide with their fingertips. Their brains just write the caption afterward.
Where This Actually Plays Out
Picture a classroom in soft, breathable uniforms. Kids fidget less and focus more, because nothing scratchy is competing for their attention. Picture a hospital bed dressed in gentle linens instead of stiff, clinical ones. Shoulders drop a little faster. Picture a five-star hotel robe with real weight to it, sheets with a thread count you can feel before anyone announces the number. The room has already made its case before a single staff member says a word.
None of that happens by accident. It happens because someone understood that texture does emotional work whether a brand plans for it or not.
A World Woven in Texture
Travel far enough and texture starts speaking in dialects. Silk carries centuries of ceremony in Japan. Kente cloth, hand-woven in raised patterns across West Africa, tells stories of heritage and status that a photo alone can’t capture. Dense wool in Scandinavia is less a style choice than a survival strategy that eventually became culture, resilience spun into every fiber to get through a brutal winter.
These aren’t just materials. They’re identities, worn on the body and handed down.
The Blind Spot Nobody’s Solved Yet
E-commerce cracked color, cracked fit charts, mostly cracked video. It has not cracked touch. Researchers testing simulated haptic feedback in online apparel shopping found that screens still can’t replicate the confidence a customer gets from actually handling a fabric. Until touchscreens catch up, the only honest way to sell texture online is to describe it relentlessly: fiber content, weight, weave, finish, and photography that doesn’t oversell the hand-feel it can’t actually deliver.
The Unglamorous Part Nobody Photographs
Here’s the part that never makes the mood board: none of the feelings above survive an inconsistent production line. A designer can imagine the perfect hand-feel for a fabric, but if the machinery behind it drifts from batch to batch, that feeling never reaches the person wearing it.
That’s the role Svegea of Sweden plays, and it’s a deliberately unglamorous one. We don’t design the emotional experience of a textile; the manufacturers do that. What precision engineering does is make sure the texture a designer imagined is the texture that actually ships, consistently, so mills can spend their energy on the parts that require imagination instead of fighting variance on the floor.
The Actual Point
Stop designing only for how a fabric photographs. Start designing for how it will feel against skin, in the middle of an ordinary Tuesday, when nobody’s paying attention and the fabric is doing its job anyway. Texture is already telling a story. The only real choice is whether you’re the one writing it.
To talk through what consistent, imagination-ready production could look like for your line, reach out to Håkan Steene directly at h.steene@svegea.se, or visit www.svegea.se.
Circular knitting machines produce fabric as a seamless tube. What happens after that is a decision every knit manufacturer makes, sometimes without thinking too hard about it: keep the fabric in tubular form or slit it open and process it flat. Both routes are common, and both work. But they don’t behave the same way on the cutting floor, and the choice affects waste, tension, and finish quality more than a lot of production teams realize.
TL;DR: Circular knitting produces fabric as a continuous tube, and manufacturers either keep it that way (tubular processing) or slit it open into a flat sheet (open-width, or flat-bed, processing). Tubular is faster and cheaper but more prone to edge creasing; open width gives better width utilization and finish quality, but the slitting step itself can introduce stretch and distortion. Which one fits depends on the product and how the fabric will be cut.
What Tubular and Open-Width Actually Mean
A circular knitting machine forms fabric on a rotating cylinder of needles, which produces a continuous tube rather than a flat sheet. According to Textile Blog, the width of that tube is half the width the fabric would measure if it were slit open and laid flat, since the machine is knitting both the front and back layers at once. Tubular processing keeps the fabric in that closed-loop form all the way through finishing. Open-width, sometimes called flat-bed or cut-edge processing, slits the tube along one edge early in finishing and processes the fabric as a single flat layer from that point on.
Why Manufacturers Keep Fabric Tubular
Tubular processing has been the traditional route for a reason. It runs faster through finishing equipment, needs less investment in machinery, and works for a wide range of fiber types without extra steps like sizing. It is also the natural form for anything that will end up as a tube in the garment itself, like a T-shirt body or a sock, since there’s no seam to add later.
The trade-off shows up in finishing. Tubular fabric is run through extraction rollers as a folded, double layer. Cotton Incorporated’s processing guidance notes that this makes tubular fabric sensitive to sharp edge lines and creasing where the fold sits, unless roller hardness is matched carefully to the fabric.
Why Manufacturers Move to Open-Width
As quality expectations rose, particularly for elastane-blend fabrics used in fitted garments, more knit processing shifted toward open-width finishing. Academic surveys of the industry point to open-width routes giving more consistent, higher-grade finishing results than tubular processing, which is part of why open-width has been gaining ground even though it typically costs more to run.
Open-width also makes better use of the full fabric surface once cutting starts. A flat sheet lets a marker (the layout of pattern pieces) use the entire width efficiently. It matters more on styles with larger, irregular pattern pieces than it does on narrow trims or bindings. Dyeing and heat-setting can also run more evenly on a flat, single layer than on a folded tube, where the inner and outer layers don’t always receive identical heat or dye exposure.
The Trade-off That Matters Most: What Slitting Does to the Fabric
Here is the part that gets missed most often. Converting tubular fabric to open width means slitting it, and that step is not neutral. Cotton Incorporated’s own guidance is direct about it. For open-width fabrics, the slitter can be a major source of linear stretch or distortion. This is on top of whatever tension the fabric already picked up earlier in finishing. In other words, the act of going from tubular to open width is itself a common point where bowing and skewing get introduced or made worse.
This is where equipment choice starts to matter. A conventional slit-and-flatten process pulls the tube open under tension and typically produces two separate rolls of open-knit fabric from one tube. Svegea’s TSO 380 G/GF Tubular Knit Slitter can convert a tubular knit into a single, full-width roll in one pass. This machine has electronic tension control on the fabric take-up. The main benefit is fabric yield rather than distortion control on its own, but tighter, more consistent tension through the conversion step also means less of the stretch that a rougher slitting process tends to introduce.
Which One Fits Your Line?
There isn’t a universal answer, and the right route usually comes down to questions. What the fabric becomes (a tubular garment part, or flat-cut panels). Or how much elastane or stretch fiber is in the blend. And how much of the fabric width the pattern pieces actually use. Narrow trims, bindings, and bands cut from tubular knit often stay tubular right up to the cutting stage. For high-stretch knit fabrics, larger flat-cut panels frequently justify the additional step of open-width conversion. It also provides slitting automation and tension-free feeding systems used to prevent lateral deformation and edge curl.
It is also worth asking the question per style rather than settling on one route for the whole line. A manufacturer running both fitted, flat-cut garments and simple tubular pieces in the same facility often gets better results.
Need help optimizing your fabric or reducing waste? Contact Håkan Steene: h.steene@svegea.se.
Cut a length of tubular knit fabric, lay the panels out, and something looks off. The pieces don’t quite sit on the grain. Sleeves twist slightly after the first wash. Quality control flags the batch, and nobody can point to one clear mistake.
This is fabric distortion, and it is one of the more common, least understood problems in cutting rooms that work with knits. The good news is that distortion is rarely random. It follows patterns, and those patterns can usually be traced back to tension, handling, and the cutting method itself.
|
TL;DR: Knit fabric distortion (bowing and skewing) usually starts before the fabric reaches the cutting table, in knitting, dyeing, or finishing. But the cutting method can make it worse or help contain it. Tubular knits are especially prone to skew once they are slit open and spread flat for cutting. Circumferential cutting, which works the fabric in the round, skips that extra handling step and helps the grain stay aligned. |
What Bowing and Skewing Actually Mean
Distortion in knit fabric usually shows up as one of two defects. Bowing happens when the courses, the horizontal rows of loops in a knit, curve into an arc across the fabric width instead of running straight. Skewing is different: the courses stay straight, but they tilt, so one side of the fabric runs ahead of the other. According to Textile Learner, both defects are graded by how far the courses deviate from a line perpendicular to the fabric’s selvage, and both get harder to spot on solid colors than on stripes or prints, where the distortion becomes visually obvious.
Where the Tension Really Starts
Most distortion is introduced long before a roll reaches the cutting table. The knitting machine’s take-up mechanism can pull fabric unevenly across its width, and that unevenness carries through to finishing. During dyeing and finishing, fabric is pulled through rollers and tenter frames under tension, and if that tension is not distributed evenly from edge to edge, bowing or skewing is the result, as Apparel Science and Textile Learner both document.
Handling at the cutting stage matters too. Fabric that is spread and cut under tension, straight off the roll, tends to relax back into a different shape once it is off the table. This is exactly why many cutting rooms build in a relaxation period, letting the fabric sit unrolled for a few hours before it is cut, particularly for stretch fabrics with spandex or Lycra content, where relaxation shrinkage is more pronounced.
Why Tubular Knits Are Especially Vulnerable
Circular knit fabric is produced as a seamless tube. For many cutting operations, this tube is slit open along one edge and spread flat. This extra step introduces skew by placing uneven tension across the fabric, adding to existing knitting or finishing distortions.
Processing fabric in the round avoids slitting and holds grain alignment much better. For example, Svegea’s Euro-Collarette range cuts bindings and collarette bands directly from tubular fabric without opening or flattening it first. While it can’t fix pre-existing fabric distortion, it eliminates a key handling step that often makes the problem worse.
How to Check Your Own Line for Distortion
Distortion is measured formally under ASTM D3882, the standard test method for bow and skew in woven and knitted fabrics. It works by comparing the actual path of a course (or a filling yarn, in woven fabric) against a straight line perpendicular to the selvage, and expressing the gap as a percentage of fabric width.
A quick in-house check does not need lab equipment. Make a small nick perpendicular to the selvage and tear the fabric across its width. On fabric that is square, the tear runs in a straight line. A curved tear points to bowing, and a diagonal tear points to skew. Because distortion can worsen along the length of a roll, it is worth repeating the check at several points, not just at the start.
What It Costs When Distortion Goes Unchecked
Unchecked distortion hits your bottom line downstream, long after fabric leaves the cutting table. When workers mark pattern pieces against a distorted grain line, the pieces twist out of alignment during sewing. Panels might look perfect on the table, but the finished garment pulls, warps, or sags after its first wash as the fabric relaxes into its true shape. For manufacturers running tight margins on knitwear, these flaws trigger costly rework, wasted fabric, and customer returns. None of these expenses surface on the cutting room floor until fixing them becomes far too expensive.
A Process Question First
Controlling distortion depends more on process discipline than on raw equipment power. Proper tension control, fabric relaxation, and minimal handling ensure fabric stability.Process matters. When working with tubular knits, manufacturers must evaluate whether their handling opens and flattens the tube more than necessary.
Bowing and skew can quickly disrupt a tubular knit line. If you are facing these issues or want to optimize your fabric preparation before cutting, reach out to Svegea. Håkan Steene can evaluate your setup and talk through solutions with you. Contact him directly at h.steene@svegea.se.
TL;DR: AI tools like ChatGPT, Gemini, and Copilot now summarize supplier information for buyers, and they cite whoever documents their equipment most clearly. Manufacturers who publish structured FAQs, verifiable specs, and schema markup for an automated slitting machine stand a much better chance of being the source AI trusts. Svegea’s compact, well documented systems are built with exactly that kind of clarity in mind.
As 2026 draws to a close, textile manufacturers face a new kind of competition. It isn’t just about faster machines or tighter margins anymore. It’s about whether AI tools even know your company exists.
Search behavior changed fast this year. Buyers researching an automated slitting machine no longer scroll through ten blue links. Instead, they ask ChatGPT, Gemini, or Copilot a question. They get back one confident answer. If your brand isn’t part of that answer, you might as well be invisible.
Automation keeps moving forward across textile plants worldwide. Manufacturers want machines that cut waste, boost yield, and run with less supervision. Sustainability pressure is rising too. Buyers now ask harder questions about material efficiency and energy use. Digital compliance rules are tightening across the EU and beyond. Suppliers must document their processes more openly than before.
These shifts matter for one big reason. They shape what AI models learn to trust. A generative engine builds its answers from the clearest, best-documented sources it can find. Vague marketing copy doesn’t help much here. Verified specs, clear certifications, and real case studies do the heavy lifting instead. Simple, factual writing beats flowery sales language almost every time.
Here’s the uncomfortable part. AI tools already summarize supplier information for buyers. They tend to favor whoever wrote the clearest content first. Well-established players often get cited by name. Many capable smaller manufacturers get skipped over instead. That’s not because their equipment is worse. It’s simply because their content never gave the AI anything solid to work with.
Think of it this way. Say a purchasing manager asks an AI tool for the best automated slitting machine for knitwear production. The tool needs a direct, structured answer to serve up right away. Maybe your product pages ramble about company history instead of stating specs and use cases plainly. If so, the algorithm moves right on to a competitor.
AEO and GEO, Explained Simply
Two ideas matter most here. The first is AEO, or answer engine optimization. This means writing content that answers technical questions the way a buyer actually asks them, not the way an old brochure might. The second is GEO, or generative engine optimization. This is about becoming the source an AI trusts enough to cite by name in tools like ChatGPT, Gemini, and Copilot.
In practice, this work looks fairly simple. Structure your FAQs so each question gets one clean answer. Publish verifiable data instead of vague claims. Give your product pages the kind of metadata that search engines and language models can actually parse. Google’s own guidance still underpins much of this approach. Structured, well-organized pages remain the foundation that AI answers are built on. Skip the guesswork and write for clarity first, and keywords will usually follow on their own.
Svegea’s Perspective
This is exactly where compact, well-engineered automation earns its keep. Picture a properly documented automated slitting machine built for accuracy and low material waste. It gives manufacturers exactly the kind of concrete detail AI models look for. Think consistent output specs, energy figures, and measurable yield gains. Svegea’s approach to compact slitting and cutting systems reflects that same idea. Build machines worth documenting clearly, and the documentation does much of the marketing on its own. Buyers trust numbers. So do the AI tools that now speak for buyers.
Action Steps for Manufacturers
A few practical moves can make a real difference this year. Start by publishing technical FAQs and spec sheets written for direct AI answers, not just search rankings. Add schema markup and clean product metadata so machines can actually read your pages properly. Share verifiable performance data instead of general claims whenever you can. Work with industry peers on shared benchmarks too, since AI models weigh third-party validation heavily. Reference points from established trade sources, such as Style.com or Textile World, can help build that kind of credibility over time. Even a short case study, backed by real production numbers, can carry more weight with an AI model than a page full of adjectives.
None of this happens overnight. It takes a real commitment to writing content that is precise instead of promotional. But manufacturers who start now will have a real head start once AI search becomes the default way buyers shop for equipment.
It’s Not About the Ranks Anymore
In 2027, visibility won’t depend on who ranks first anymore. It will depend on who AI trusts enough to tell the story of textile innovation. Manufacturers who document their equipment clearly today are the ones whose machines will show up in tomorrow’s answers.
If you want to see how a well-documented, compact automated slitting machine performs in real production, explore Svegea’s systems at www.svegea.se. You can also reach out directly to Håkan Steene at h.steene@svegea.se for more details.