The short answer: The EU Digital Product Passport (DPP) is a digital record that will travel with each textile product sold in the European Union. The brand that sells the product owns the passport, but much of the data inside it comes from the factory: what the fabric is, where it came from and how it was checked. The EU switched on the DPP Registry in July 2026, and textile rules are expected toward the end of 2027. That leaves manufacturers a short window to get their data in order.
Key Takeaways
- The EU launched the Digital Product Passport Registry on 20 July 2026. Rules written specifically for textiles are expected toward the end of 2027.
- Brands register the passports, yet they will rely on their suppliers for the data.
- Fabric that is inspected, relaxed, and measured before cutting is far easier to document.
- Factories that build clean, digital records now will become the suppliers EU brands trust first.
Picture a plain white T-shirt on a shop shelf in Stockholm a few years from now. A shopper scans the small code on its label. In seconds, her phone shows what the shirt is made of, where it was produced and how long it should last. Behind that simple scan sits a long chain of facts, and many of those facts start on your cutting floor.
That scene is the promise of the EU Digital Product Passport. For garment and textile manufacturers, it is also a quiet change in what customers will expect from you.
What Is the EU Digital Product Passport?
The Digital Product Passport is a digital identity card for a product. It comes from the Ecodesign for Sustainable Products Regulation (ESPR), the EU law that aims to make products more durable, repairable and recyclable. Each passport holds key information about a product, and a central EU registry links that record to a unique product ID.
On 20 July 2026, the European Commission launched the DPP Registry along with a testing environment. Businesses can register passports through a simple web interface or connect their own systems through an API. Customs authorities will also be able to check electronically whether imported goods carry a valid, registered passport. Textiles sit among the priority groups, alongside furniture, tyres, steel and electronics.
When Will Textiles Need a Passport?
Not yet, but soon. The registry is live; however, it does not make every garment subject to a passport today. A separate textile act must first set the exact data fields, scope and timeline, and trade reports expect it toward the end of 2027.
That might sound far away. In practice, it is not. Brands plan their collections well ahead, and they will want supplier data in place before the first passport is due. As a result, your customers may start asking questions long before any legal deadline.
Why Should Garment and Textile Manufacturers Care?
Legally, the duty to create and register a passport falls on whoever places the product on the EU market, usually the brand or importer. Still, brands cannot invent the facts. They will turn to the mills, factories and cut-and-sew partners who actually handled the fabric.
Another rule adds weight to this shift. Since 19 July 2026, large companies in the EU can no longer destroy unsold clothing, footwear or accessories, and a standard reporting framework follows in February 2027. Together, these rules reward brands that know exactly what they made, how much they made and why. Suppliers who can answer those questions quickly will become preferred partners. Those who cannot will start to look like a risk.
The Cutting Room: Where Good Data Begins
Every roll of fabric tells a story on its way to becoming a garment. It arrives, gets inspected, rests, gets measured and finally meets the blade. Each step creates useful facts, such as true length, real width, defects found and shrinkage after relaxing. Today, many of these facts live on paper or in a supervisor’s memory. Under the DPP, they become evidence.
Inspect before you cut
A recorded inspection gives every roll a history. Defects found at this stage stay out of finished garments, which means fewer rejects and less unsold stock. Just as important, the inspection log becomes proof of the care your team takes.
Measure what you actually received
Invoices state one width and length; the roll on your floor may tell a different story. Recording the real figures improves marker planning and gives brands accurate material data instead of estimates.
Relax first, then record
Knitted and stretch fabrics carry tension from knitting, dyeing and winding. Measure them too early, and the numbers drift once the fabric settles. Relaxing fabric before spreading gives you true measurements and garments that keep their size after washing. Svegea of Sweden’s CRX Air Relaxing Series, for example, measures fabric width automatically, controls length electronically and exports production data via USB, so the figures leave the machine already in digital form.
Five Steps to Get Passport-Ready Now
- Map your data. List what you already record for each roll and each order, and note where it lives.
- Give every roll an ID. Make sure that ID follows the fabric from receiving through inspection to cutting.
- Go digital at the source. Favour equipment that logs and exports data, so nobody has to retype numbers later.
- Talk to your EU customers. Ask what information they expect and in which format they want it.
- Watch for the textile act. Follow European Commission updates, since the final data fields will shape your records.
The Bottom Line
The Digital Product Passport is not just paperwork. It is proof. Factories that inspect, relax, measure and record fabric before the first cut will hand brands the data they need, and they will earn the trust that wins repeat orders. So when that shopper in Stockholm scans her white T-shirt, the story she reads could start in your cutting room.
Want to see how better fabric preparation fits your production line? Contact Svegea of Sweden or email Håkan Steene at h.steene@svegea.se to book a product demo.
Frequently Asked Questions
What is a Digital Product Passport for textiles?
It is a digital record linked to a garment or textile product through a unique ID, such as a QR code. Under the EU’s Ecodesign for Sustainable Products Regulation, it will store key product information to support transparency, repair, and recycling.
When will the Digital Product Passport become mandatory for textiles?
The EU Registry went live on 20 July 2026, but textiles still need their own delegated act. Trade reports expect it toward the end of 2027, and mandatory dates will follow from that act.
Who is responsible for the Digital Product Passport, the brand or the manufacturer?
The company that places the product on the EU market, usually the brand or importer, must create and register the passport. However, manufacturers supply much of the data, so brands will ask them for it.
How can garment factories prepare for the Digital Product Passport?
Start by recording roll-level data such as fabric type, true width, length and inspection results. Then assign each roll an ID, choose equipment that exports data digitally and agree on data formats with your EU customers.
Walk into any store this December, and velvet will find you first. A plum party dress. An emerald blazer. Wide-leg trousers in deep chocolate brown. Velvet catches the light, feels like a small luxury, and makes even a simple outfit look ready for a celebration.
The runways saw it coming. Net-a-Porter’s fall/winter 2026 trend report named velvet the season’s key texture, with Alaïa, Khaite, and Ralph Lauren all showing tailored velvet looks. Meanwhile, Marie Claire spotted velvet trousers at Armani, Khaite, and Zimmermann.
For garment manufacturers, that popularity brings a real challenge. Velvet is gorgeous, but it is also one of the least forgiving fabrics on the factory floor.
So how do manufacturers handle velvet without crushing the pile? In short, they keep pressure, tension, and heat to a minimum at every stage. That means relaxing the fabric before cutting, inspecting every roll for flaws and shading, rewinding with little or no tension, and cutting every piece with the nap running the same way.
Key Takeaways
- Velvet leads the fall/winter 2026 and holiday collections, from party dresses to tailoring.
- Its pile flattens easily under pressure, heat, and moisture, and the damage can be permanent.
- The nap changes how velvet reflects light, so every piece must be cut in the same direction.
- Gentle relaxing, careful inspection, and tension-free rewinding protect velvet from roll to cut.
Why is velvet so difficult to manufacture?
Velvet gets its softness from a dense pile of tiny upright fibers. That pile gives velvet its glow. Unfortunately, it also makes the fabric fragile. According to Textile School, pressure, heat, and moisture can permanently flatten the pile. A tight roll, a heavy stack, or a careless press can leave marks that no amount of steaming will fix.
Then there’s the nap. The pile leans slightly in one direction, so the same fabric can look lighter or darker depending on how light hits it. Threads Magazine explains that velvet looks darker and absorbs light with the nap up, and looks lighter with the nap brushed down. Cut one sleeve the wrong way, and it can look as if it came from a different bolt.
Where does velvet get damaged in production?
Most problems start long before the sewing line. Here are the usual suspects:
- Tight winding. Rolls wound under heavy tension press the pile flat, especially near the core.
- Stored tension. Stretch velvet holds tension from knitting, dyeing, and winding, so cut panels can shrink later.
- Hidden flaws. Crush marks, bald spots, and shade differences are easy to miss until the garment is finished.
- Mixed nap. Pieces cut in different directions create visible color differences on the same garment.
Consequently, the best protection is a gentle, consistent process from the moment a roll arrives to the moment it reaches the cutting table.
How can factories protect velvet from roll to cut?
Relax it first. Stretch velvets need time to settle before spreading. Air-assisted relaxing machines, such as Svegea’s CRX Air, float the fabric on a cushion of air to release tension without pressing the surface.
Inspect every roll. A fabric inspection machine helps your team spot crush marks, shading, and pile defects before cutting begins, when they still cost the least to fix.
Rewind gently. When velvet needs rewinding, tension control matters. A tension-free rewinder like the W 2100S helps keep the pile upright from the outer layers right down to the core.
Cut with the nap. Mark the nap direction on the reverse side, and lay every pattern piece the same way. This layout uses more fabric, but it protects the finished look.
Finally, store rolls with care. Avoid stacking heavy rolls on top of velvet, and keep the storage area cool and dry.
Why does this matter for holiday orders?
Holiday collections run on tight deadlines. Brands want velvet dresses and blazers on the shelves by late November, and there is little time to remake rejected pieces. A crushed panel or a mismatched sleeve doesn’t just waste fabric. It can delay an entire delivery.
On the other hand, factories that handle velvet well become partners that brands trust. And when a buyer finds a supplier that delivers flawless velvet season after season, that buyer tends to come back.
Make This Velvet Season Your Best Yet
Velvet rewards patience and precision. Give it a gentle process, and it will give your customers that unmistakable glow. To find the right relaxing, inspection, or rewinding machine for your production, contact Svegea of Sweden or email Hakan Steene at h.steene@svegea.se to book a product demo.
Frequently Asked Questions
What is the nap of velvet?
The nap is the direction the pile leans. It changes how the fabric reflects light, so manufacturers cut all pieces of a garment in the same direction.
Can crushed velvet pile be restored?
Light marks may lift with gentle steam from the wrong side. However, heavy or long-term pressure can flatten the pile permanently.
Why does stretch velvet shrink after cutting?
It holds tension from knitting, dyeing, and winding. Relaxing the fabric before cutting lets it return to its natural dimensions.
A camel coat with no logo. An ivory silk shirt with no visible branding. A plain wool trouser that costs more than a month’s rent. This is quiet luxury, and it has changed what shoppers notice.
When a garment has no logo to speak for it, the fabric does all the talking. Shoppers run their hands over the cloth, hold it up to the light, and study the seams. A small slub, a faint shade band, or a pulled thread has nowhere to hide. For garment manufacturers, quality control can no longer start at the sewing line. It has to start with a fabric inspection machine, long before the first cut.
So how do garment manufacturers inspect fabric for defects? In short, operators run each roll across a lit inspection table, check it for flaws as it moves, mark every defect, and measure the roll’s true length. Most factories then grade each roll with a point system and decide whether to use it, return it, or cut around its flaws.
Key Takeaways
- Quiet-luxury garments rely on flawless fabric because there are no logos or prints to hide defects.
- Fabric inspection catches flaws before cutting, when they cost the least to fix.
- Much of the industry grades fabric with the four-point system in ASTM D5430.
- The right inspection machine depends on fabric width, speed, and where rolls go next.
Why Quiet Luxury Raises the Bar
Loud fashion has its uses. Bold prints, heavy embellishment, and large logos pull the eye away from the cloth underneath. Quiet luxury does the opposite. It strips a garment back to cut, colour, and material.
That shift puts pressure on every stage of production. A neutral coat or a pale knit shows every irregularity. Moreover, buyers of these pieces expect them to last for years, so they examine them closely before they pay. One visible flaw can turn a premium price into a return, a markdown, or a lost wholesale account.
For suppliers, the message is simple. If the brand promises perfection, the fabric must deliver it first.
The Cost of Finding Flaws Too Late
A defect costs the least while it is still on the roll. Once the fabric is spread and cut into panels, the same flaw can spoil several pieces at once. If it slips past sewing, the factory pays for labour, thread, and finishing on a garment that may never sell.
Late detection also hurts relationships. Many luxury buyers run their own checks when goods arrive. When they find defects, they may reject a whole shipment, not just the faulty pieces. As a result, a few missed flaws can delay an entire order and damage trust that took years to build.
Inspection before cutting turns unknown risks into known facts. The factory knows exactly what it has, where the flaws sit, and how much usable fabric remains.
How Garment Manufacturers Inspect Fabric for Defects
Most factories follow a similar routine:
- Load the roll onto a fabric inspection machine.
- Run the fabric over a lit inspection table at a steady, controlled speed.
- Check the full width for holes, stains, slubs, shade variation, and knitting or weaving faults.
- Mark each defect at the selvedge so cutters can avoid it.
- Record the true length and width of the roll.
- Grade the roll with an agreed point system.
The most widely used grading method is the four-point system, set out in ASTM D5430, the standard test methods for visually inspecting and grading fabrics. Inspectors give each defect one to four penalty points based on its size, then work out the total points per 100 square yards. Buyers and suppliers agree in advance how many points a roll may carry before it counts as second quality.
What Good Fabric Defect Detection Looks Like
Good fabric defect detection depends on three things: light, speed, and control.
First, the inspection area needs bright, even light, so faint shade bands and fine slubs stand out. Second, speed must suit the fabric. A plain cotton can move faster, while a fine silk or fine-gauge knit needs a slower pass. Finally, the fabric should move smoothly, without stretching or drifting to one side. Uneven tension can distort knits and hide flaws, and a wandering edge slows the operator down.
Accurate measuring matters too. Rolls do not always match the length on their labels. A reliable meter or yard counter shows what the factory really received, which protects both costing and supplier claims.
Choosing the Right Inspection Setup
Not every factory needs the same machine. Fabric width, daily volume, and the way rolls move to the next stage all shape the choice.
For standard widths, a compact roll-to-roll machine often covers daily needs. Svegea of Sweden’s CMI 180 and CMI 180E, for example, handle fabric up to 1800 mm wide at speeds of up to 45 m/min. For wider goods, the CMI 210 R and CMI 210 ZR take fabric up to 2100 mm and add photocell edge alignment, electronic tension adjustment, and an electronic meter counter. The CMI 210 ZR can also deliver fabric roll to roll or roll to flat, which helps when inspected fabric goes straight to spreading.
Whatever the model, the goal stays the same: know your fabric before you cut it. You can compare the full range on the fabric inspection machines page.
Quick Tips for Flawless Fabric
- Inspect every roll, not just samples. Premium buyers expect the same quality across the whole order.
- Slow down for delicate fabrics. Fine silks, wools, and knits reveal more flaws at lower speeds.
- Check shade from roll to roll. Compare a strip from each roll to catch colour differences between batches.
- Mark defects clearly. Use stickers or tags at the selvedge so cutters spot them at once.
- Relax knits first. Tension can stretch knitted fabric and hide its true width, so a fabric relaxing machine is a useful step before inspection.
Frequently Asked Questions
How do garment manufacturers inspect fabric for defects?
They run each roll through a fabric inspection machine, check it under bright light as it moves, mark every defect, measure the roll, and grade it, usually with the four-point system.
What is the four-point system in fabric inspection?
It is a grading method described in ASTM D5430. Inspectors give each defect one to four penalty points based on its size, then compare the total per 100 square yards with an agreed limit.
What defects does fabric inspection detect?
Common examples include holes, stains, slubs, broken yarns, shade variation, and differences in width or length.
Why is fabric inspection important for luxury brands?
Quiet-luxury garments rely on plain, premium fabric. With no logos or prints to distract the eye, even small flaws are visible, so inspection protects both the garment and the brand’s reputation.
Ready to Inspect Smarter?
Luxury starts long before a garment reaches the shop floor. It starts with the roll. To find the right fabric inspection machine for your production, contact Svegea of Sweden or email Hakan Steene at h.steene@svegea.se to book a product demo.
Every autumn, shoppers reach for sweaters, cardigans, and sweatshirts. Most of them judge a knit in seconds. They touch the fabric, check the fit, and tug at the cuff. That last move tells them more than any label.
A cuff that snaps back feels like quality. One that sags, twists, or ripples feels cheap, even when the body fabric is excellent. For knitwear manufacturers, the finishing details deserve as much attention as the yarn.
So how are rib cuffs and hems made in production? In short, factories start with tubular rib fabric and cut it into even bands on a collarette cutting machine. They then fold the bands, sew them to the sleeve or body, and finish them. The cleaner the first cut, the better the final garment looks and wears.
Key Takeaways
- Factories cut rib cuffs and hems from tubular rib fabric into bands of equal width.
- Even small differences in band width cause twisted cuffs and wavy hems.
- Uneven bands slow down sewing, raise reject rates, and waste fabric.
- The right level of cutting automation depends on volume, style changes, and staff.
Why the Cuff Makes or Breaks a Sweater
The cuff does a lot of work. It holds the sleeve in place, keeps warmth in, and frames the hand. The hem does the same job at the waist. Together, they give a sweater its shape.
Rib fabric stretches and recovers, which makes it comfortable to wear. Cutting it, however, is another story. Rib shifts under the blade, and even a small shift changes the band width. Cotton knits also relax and skew after knitting, an effect textile researchers call fabric spirality or torque. A band that is even slightly wider on one side will twist once it is sewn. Repeat that error across a winter order of thousands of sweaters, and a small flaw becomes a serious quality problem.
Moreover, today’s shoppers post reviews, and those reviews move sales. Research from Northwestern University’s Spiegel Research Center found that a product with five reviews is 270% more likely to be purchased than one with none. A single comment about a stretched-out cuff can hurt sales faster than any returns report. Brands know this, and they pass that pressure straight to their suppliers.
How Rib Cuffs and Hems Are Cut
Most knitwear factories follow the same basic process:
- Rib fabric is knitted in a continuous tube.
- An operator loads the tube onto a collarette cutter.
- The machine cuts the rotating tube into continuous bands at a set width.
- Sewing operators attach the bands to sleeves, bodies, or necklines.
The cutting step sounds simple. In practice, it decides whether the rest of the line runs smoothly or stalls.
The Hidden Cost of Uneven Bands
When bands vary in width, problems pile up quickly. Sewing operators slow down to ease uneven pieces into place. Finished cuffs pucker or roll. Quality control rejects more garments, and rework eats into already thin margins.
Hand cutting makes this worse. Scissors and rotary tools depend on the operator’s eye and energy, and both fade over a long shift. As a result, the first cuff of the day rarely matches the last.
Waste adds up too. A 2024 UC Santa Barbara study cites estimates that 10–15% of fabric is already discarded during cut-and-sew, and a study published by the U.S. National Institutes of Health puts the figure as high as 20%. Every off-width band that gets thrown away adds to that loss, and it is fabric the factory has already paid for. Over a full season, that loss can quietly erase the profit on an entire style.
Finding the Right Level of Automation
Once a factory sees these costs, the next question is how much automation it actually needs. The answer is rarely “as much as possible.”
Large plants that run the same basic tee for months often benefit from fully automatic lines. Many knitwear producers, though, work differently. They run medium volumes, change styles every few weeks, and bring in seasonal staff for the autumn rush. For them, a semi-automatic collarette cutter usually makes more sense.
With a semi-automatic setup, the machine handles the precision cutting, while the operator keeps control of loading and setup. Changeovers between band widths go faster, and the upfront investment stays lower. New operators also learn the process quickly, which matters when deadlines are tight.
Range matters as much as speed. A single machine should cover both slim cuffs on a fine merino sweater and deep hems on a heavy sweatshirt. Svegea of Sweden, which has built automatic collarette cutters for more than 70 years, offers semi-automatic models that cut bands from 16 to 140 mm and handle two bands at once as standard. That flexibility lets one cutter serve an entire autumn collection instead of a single style.
Quick Tips for Better Rib Bands This Season
- Relax the fabric first. Rib fabric fresh off the roll often holds tension, so let it settle before cutting to keep bands at their true width. Garment and textile manufacturing companies agree that relaxation is a key factor in a knit’s dimensional stability, and note that handling in the cutting room can cause further shrinkage.
- Match the band to the garment. Use narrower bands for fine-gauge knits and wider ones for heavy sweatshirts and outerwear.
- Check your knives daily. A dull blade drags rib fabric and leaves uneven edges.
- Test before you commit. Cut a short run, measure the bands, and adjust before you start the full order.
- Track your rejects. If cuff and hem defects keep rising, the cause often starts at the cutting table, not the sewing line.
Frequently Asked Questions
What is a collarette cutting machine? A collarette cutting machine cuts tubular knitted fabric into continuous bands of equal width. Factories use these bands for cuffs, hems, neckbands, and binding.
How are rib cuffs cut for sweaters? Factories cut rib cuffs from tubular rib fabric on a collarette cutter set to the required band width. Operators then fold the bands and sew them to the sleeves.
What is the difference between semi- and fully automatic collarette cutters? Semi-automatic cutters need more operator input during loading and setup, which suits medium volumes and frequent style changes. Fully automatic cutters need less manual work and suit high-volume production of the same styles.
Why do sweater cuffs twist after sewing? Twisted cuffs usually come from bands that vary in width or from fabric cut while still under tension. Relaxing the fabric and cutting with consistent equipment solves most cases.
Ready to Perfect Your Cuffs?
Sweater season rewards the details. If your team wants cleaner cuffs, steadier hems, and less waste, a short conversation can point you in the right direction. Contact Svegea of Sweden or email Hakan Steene at h.steene@svegea.se to book a product demo.
Ribbing is back on the runway. And it’s showing up in an unexpected place: the cuff, the collar, the hem. Spring/Summer 2027 knitwear leans hard into edge detailing. That shift puts pressure on the cutting room, not just the design studio.
What is a collarette trim and why is it trending in 2027? A collarette trim is a ribbed knit band. It’s cut from tubular fabric and sewn onto a cuff, collar, or hem for stretch and structure. It’s trending in 2027 because designers favor edge detailing over heavy, all-over patterns. Ribbing delivers texture exactly where it needs to sit.
Why are ribbed cuffs and collars trending in 2027?
A return to craftsmanship
Fashion forecasters call this season a return to craftsmanship. Trend analysts at POP Fashion describe Spring/Summer 2027 knitwear as centered on detailed stitching. That stitching concentrates at the edges of a garment, not across the whole piece. Cuffs, hems, and necklines get the attention, while the body of the garment stays simple.
Why manufacturers should pay attention
This shift matters for manufacturers. A ribbed cuff or collar does real structural work. It holds a sleeve or neckline in place, without a zipper, button, or drawstring. So when a trend calls for that detail on nearly every piece, cutting rooms need a fast, consistent way to produce it.
Trend forecasting platform Trendalytics also points to a broader move toward relaxed silhouettes and natural texture. This spans Spring 2027 runways, from Milan to Copenhagen to Tokyo. Ribbing fits neatly into that story. It’s tactile, and it reads as considered rather than mass-produced. It also works across nearly every knitwear category, from athleisure to elevated basics.
What machine makes collarette trims?
How the cutting process works
A collarette cutting machine converts tubular knit fabric into ribbed bands. These bands get sewn onto a cuff, collar, or waistband. First, the tube feeds onto a rotating turntable. Then a blade slices continuous, uniform bands as the table turns. Band width is set before the fabric touches the blade. As a result, every strip comes off at the same measurement, cut after cut.
Semi-automatic vs. fully automatic
Two broad categories exist. Semi-automatic machines need an operator to load the fabric and start the cycle, then step back while the machine cuts. Fully automatic machines add more: PLC-driven speed synchronization, auto-stop sensors, and higher throughput. This suits manufacturers running long production runs of the same trim.
Both approaches produce the same result: a clean, ribbed band with a consistent width. However, they differ in speed, automation, and how many bands a single pass can cut. That’s exactly what separates Svegea’s EC-series models from each other.
How do I choose between the EC300, EC200C, EC200CS and EC50?
Svegea builds four collarette cutting machines. Together, they cover everything from small-batch production to high-speed, high-volume cutting. The table below breaks down what each one handles.
| Model | Automation | Bands per pass | Band width | Max speed | Best for | Learn more |
|---|---|---|---|---|---|---|
| EC 50 | Semi-automatic | 2–3 (4 with extra knife unit) | 16–140 mm | Up to 30 m/min | Small to mid-size production, hands-on operation | svegea.se/product/ec-50-semi-automatic/ |
| EC 200C | Fully automatic | 3 (4 with extra knife unit) | 16–170 mm | Up to 40 m/min | Mid-volume runs needing zero-waste, hands-off cutting | svegea.se/product/euro-collarette-200c/ |
| EC 200CS | Fully automatic | 4 (5 with extra knife unit) | 16–260 mm | Up to 60 m/min | Wider bands at high speed, PLC-synced production | svegea.se/product/euro-collarette-200cs/ |
| EC 300 | Fully automatic | 4 (5 with extra knife unit) | 16–170 mm | Up to 60 m/min | High-volume runs needing both scissor and crush cutting | svegea.se/product/euro-collarette-300/ |
Matching a machine to your production
On the EC50, operators cut up to three bands at once. A fourth band is possible with an added knife unit. It’s a solid starting point for manufacturers who don’t yet need full automation. Meanwhile, the EC200C is built for zero-waste, fully automatic cutting once a job is set up. That makes it a natural step up for mid-volume runs of a single trim width.
The EC200CS handles wider bands, up to 260 mm, without needing a second machine. So it suits collections that mix narrow cuffs with wider waistbands in the same run. On the EC300, manufacturers get both scissor and crush cutting. This gives more control over edge finish, especially when a collection spans different fabric weights.
Weighing speed against cost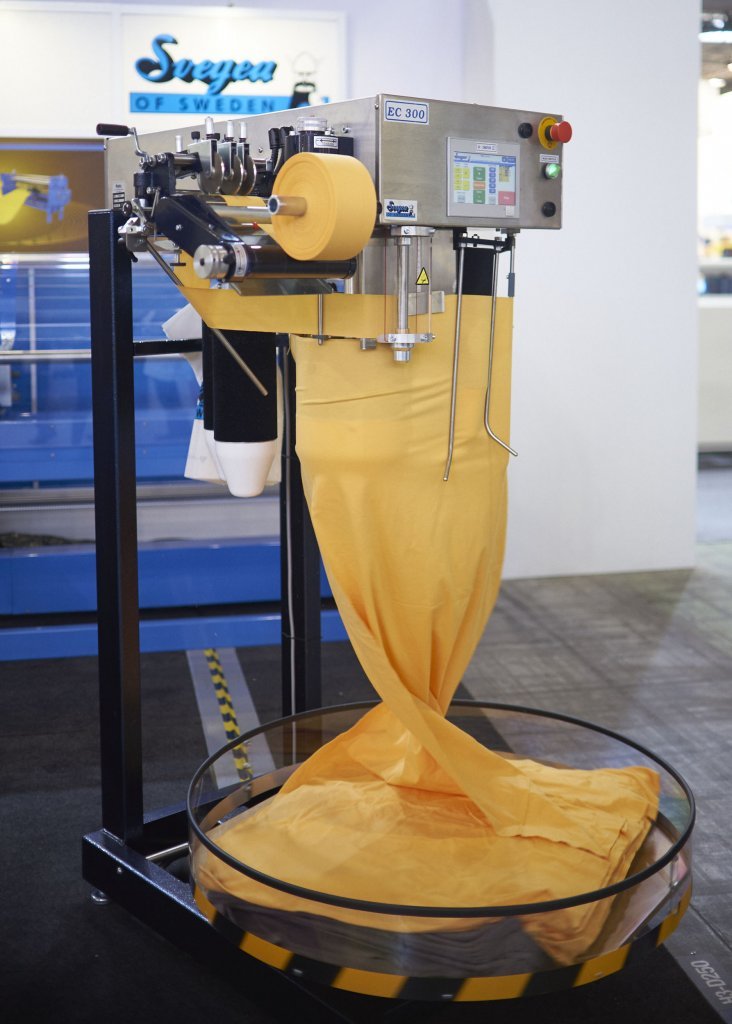
Speed is capped at 30 m/min on the EC50, since an operator manually manages the load and finish. By contrast, the three fully automatic models run two to four times faster. Their fabric feed, cutting speed, and stop points sync automatically. If your 2027 lineup leans on one or two standard rib widths at moderate volume, the EC200C is the more economical fit. However, if widths vary across styles, or volume is climbing fast, the EC200CS or EC300 earn back their higher price point in throughput.
Ready for the ribbing comeback
Ribbing isn’t a passing microtrend. It’s shaping up to be one of the defining details of 2027 knitwear. Manufacturers who can produce consistent, high-quality collarette trims at scale will keep up with buyer demand. Every EC-series machine is engineered in Sweden, with cutting components made from high-grade steel. So the choice mostly comes down to volume and bandwidth, not build quality.
See the full lineup and specs in the Collarette Range Family brochure. For a side-by-side look at every semi-automatic and fully automatic model, visit svegea.se/collarette-cutting-machines/.
Follow Svegea on Instagram, LinkedIn, and Facebook (@svegeaofsweden) for more updates on efficient, sustainable garment and textile manufacturing machinery.
FAQ
What is a collarette trim?
A collarette trim is a ribbed knit band. It’s cut from tubular fabric and used on cuffs, collars, and hems for stretch and structural finishing.
Why is ribbing trending in fashion for 2027?
Spring/Summer 2027 knitwear favors detailed stitching at the edges, not all-over patterns. Ribbed cuffs, collars, and hems fit that trend directly.
What’s the difference between a semi-automatic and fully automatic collarette machine?
A semi-automatic machine, like the EC50, needs an operator to load fabric and start each cycle. Fully automatic models, like the EC200C, EC200CS, and EC300, add PLC-driven speed sync and auto-stop sensors for continuous, hands-off cutting.
Which EC-series machine cuts the widest bands?
The EC200CS cuts bands up to 260 mm wide, the widest range in the current EC lineup.
Do I need a fully automatic machine for small production runs?
Not necessarily. The EC50 handles small to mid-size runs well, and it costs less to start with. Fully automatic models pay off once volume or band-width variety increases.
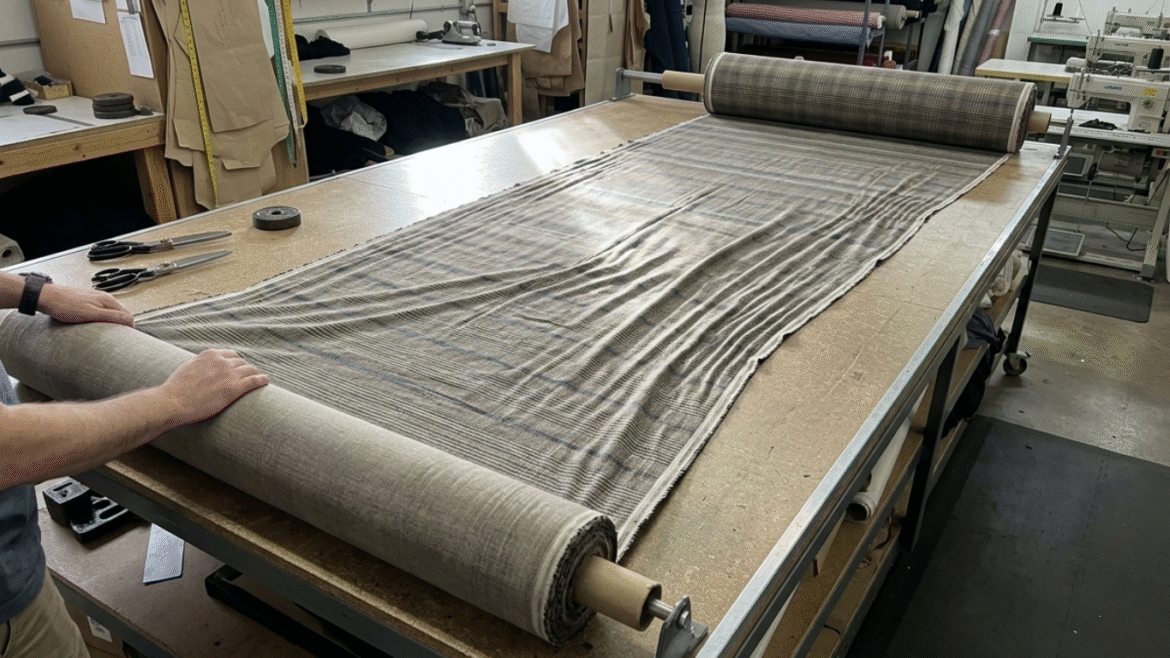
Sustainable Fabric Cutting Technology
Fabric relaxing is a pre-cutting step that lets rolled fabric rest under controlled, tension-free conditions before it reaches the cutting table. A fabric relaxing machine unwinds the roll, releases the internal stress built up during knitting, dyeing, or transport, and lets the material settle into its true dimensions. This one step cuts pattern distortion, lowers reject rates, and reduces textile waste in manufacturing. Heading into 2027, it’s one of the more practical sustainability upgrades a cutting room can make.
What causes fabric waste in cutting rooms?
Knitting, dyeing, and transport all put significant tension on rolled fabric. Winding a roll tightly, dyeing it under heat, or shipping it across the country all pull and stretch the material in ways the eye can’t see. The fabric holds this tension until something releases it. If nothing does, the release happens on the cutting table — or worse, after workers sew the garment.
Here’s the practical problem this creates. A cutter lays fabric flat and cuts it to a pattern while the material is still under tension. Once it’s off the table, the fabric relaxes and pulls back toward its natural shape. Panels that looked perfect during cutting shrink, skew, or twist. Seams no longer align. The finished garment may pucker, sag, or fit incorrectly after its first wash, and none of this shows up until it’s expensive to fix.
Knit fabrics and stretch wovens with spandex or Lycra content are especially prone to this problem, because their fibers hold tension longer than rigid wovens do. Circular knits add another layer of risk: cutting teams slit the tube open and spread it flat before cutting, and that extra handling step introduces skew on top of existing distortion.
The financial impact is larger than most cutting rooms assume. Fabric waste in cutting rooms typically runs 10% to 20% of total material, according to Lectra, and fabric alone often accounts for more than half of a garment’s total cost. Even a small improvement in fabric utilization translates directly into lower material spend and less waste headed to landfill or recycling.
How does fabric relaxing reduce waste?
A fabric relaxing machine addresses the problem at its source, before the fabric ever reaches the marker table. Instead of cutting a stressed, distorted roll and hoping for the best, the fabric first travels through a relaxing unit that unwinds it slowly, removes tension through mechanical rollers or controlled airflow, and lets the fibers settle back into their natural, balanced state.
Once the fabric relaxes, its true dimensions return, and cutters can follow the fabric’s actual grain instead of a stretched, temporary one. That single change has a ripple effect across the whole production line:
- Fewer distorted panels means fewer rejected pieces and less scrap fabric.
- Consistent dimensions mean tighter marker efficiency, so planners can nest patterns closer together without leaving a safety margin for shrinkage.
- Fewer post-wash surprises mean fewer returns and less rework, which saves fabric that would otherwise go into a second cut.
- Stable, tension-free feeding protects delicate or elastic fabrics from stretching, snagging, or fraying at the edges.
In short, fabric waste drops when cutting rooms remove tension before the fabric reaches the marker table, and manufacturers get more usable garment pieces out of every roll they buy. Operators feed a well-relaxed roll into the spreader without added stress, so what a planner sees on the marker is what the sewing line actually gets.
Which fabric relaxing machine fits my production volume?
Svegea builds fabric relaxing machines for a range of production volumes and fabric types, from standard knit-and-woven operations to high-speed, air-assisted lines handling delicate stretch textiles. The table below compares the current lineup so you can match a machine to your cutting room’s needs.
| Model | Best for | Relaxing method | Key feature | Learn more |
| CR210 | Standard-volume cutting rooms | Stepless electronic speed control with an oscillating fold system | Photocell loop control for smooth, tensionless feeding | svegea.se/product/cr210-fabric-relaxing-machine/ |
| CR210A | Higher-precision cutting rooms needing tighter edge control | Same tensionless feeding as the CR210, plus automatic edge alignment | Integrated automatic edge alignment device | svegea.se/product/cr210a-fabric-relaxing-machines/ |
| CRX Air Relaxing Series | High-speed lines and delicate stretch fabrics (jersey, lycra, technical textiles) | Dual independent air-flotation zones instead of mechanical rollers | PLC control, automatic width measurement, speeds up to 40 m/min | svegea.se/product/fabric-relaxing-machine-crx-air/ |
The CR210 suits standard-volume cutting rooms that need dependable, tensionless feeding without a large equipment footprint. The CR210A builds on that same platform and adds an automatic edge alignment device for manufacturers who need tighter tolerance control on wide or high-value fabric runs. The CRX Air Relaxing Series runs on controlled airflow instead of mechanical rollers, which makes it the better fit for lightweight knits, lycra blends, and other fabrics that stretch or curl easily under physical contact.
A quick note on model selection: Svegea’s current fabric relaxing lineup covers these three machines. If you were comparing a “CR205” model, double-check the spec sheet or brochure you’re working from — it doesn’t currently appear as an active model on svegea.se, and the closest equivalent for lighter, standard-volume applications is the CR210.
Sustainability impact
The stakes go beyond one cutting room. The fashion industry loses the equivalent of one garbage truck of textiles to landfill or incineration every second worldwide, and recyclers turn less than 1% of clothing back into new garments, according to the Ellen MacArthur Foundation. Preventing waste at the cutting stage keeps material out of that stream entirely.
Regulation is starting to reflect this. In Europe, manufacturers and retailers destroy an estimated 4% to 9% of the textile products they place on the market before anyone ever uses them, according to the European Environment Agency. That data helped shape the EU’s Ecodesign for Sustainable Products Regulation (ESPR), which bans large companies from destroying unsold textiles starting in July 2026. Manufacturers who cut waste upstream, at the cutting table, stand in a stronger position for this kind of policy shift than those relying on downstream fixes.
Fabric relaxing also supports a “cut it once” mindset. When pattern pieces hold their shape after cutting, fewer garments need rework, fewer rolls need re-ordering to cover shrinkage losses, and manufacturers waste less packaging, transport, and processing on fabric that never becomes a finished product. For a fashion industry under growing pressure to show measurable sustainability progress by 2027, this kind of upstream fix is one of the more cost-effective places to start.
Not inevitable
Cutting-room waste isn’t inevitable — it’s largely a tension problem, and tension is solvable before the fabric ever meets the blade. A fabric relaxing machine gives manufacturers a practical, proven way to stabilize material, protect pattern accuracy, and reduce textile waste in manufacturing without slowing down production.
To see the full fabric relaxing lineup, product brochures, and specifications, visit our Fabric Relaxing Series page. For more on fabric shrinkage and pre-cutting prep, read svegea.se/prevent-fabric-shrinkage/. Contact us for a product demo!
FAQ
What is fabric relaxing in textile manufacturing?
Fabric relaxing is a pre-cutting process that removes internal tension from rolled fabric so it can settle into its natural, stable dimensions before spreading and cutting.
Why does fabric shrink after cutting if it was measured correctly?
Most likely, the fabric went through cutting while still under tension from knitting, dyeing, or transport. Once it’s off the cutting table, that tension releases, and the material shrinks or shifts out of shape.
How much fabric waste can a relaxing machine actually prevent?
Results vary by fabric type and production setup, but since cutting-room waste typically runs 10% to 20% of total material (www.lectra.com), even a modest reduction in distortion-related waste can meaningfully lower material costs.
Do all fabric types need relaxing before cutting?
Knit fabrics and stretch wovens with spandex or Lycra content benefit the most, since their fibers hold tension longer. Rigid wovens still benefit, but usually need shorter relaxing cycles.
What’s the difference between fabric relaxing and pre-shrinking?
Pre-shrinking uses washing or steaming to shrink fabric before cutting, which works but takes time and adds cost. Relaxing lets the fabric settle naturally, without added moisture or heat, which is faster and gentler on delicate materials.
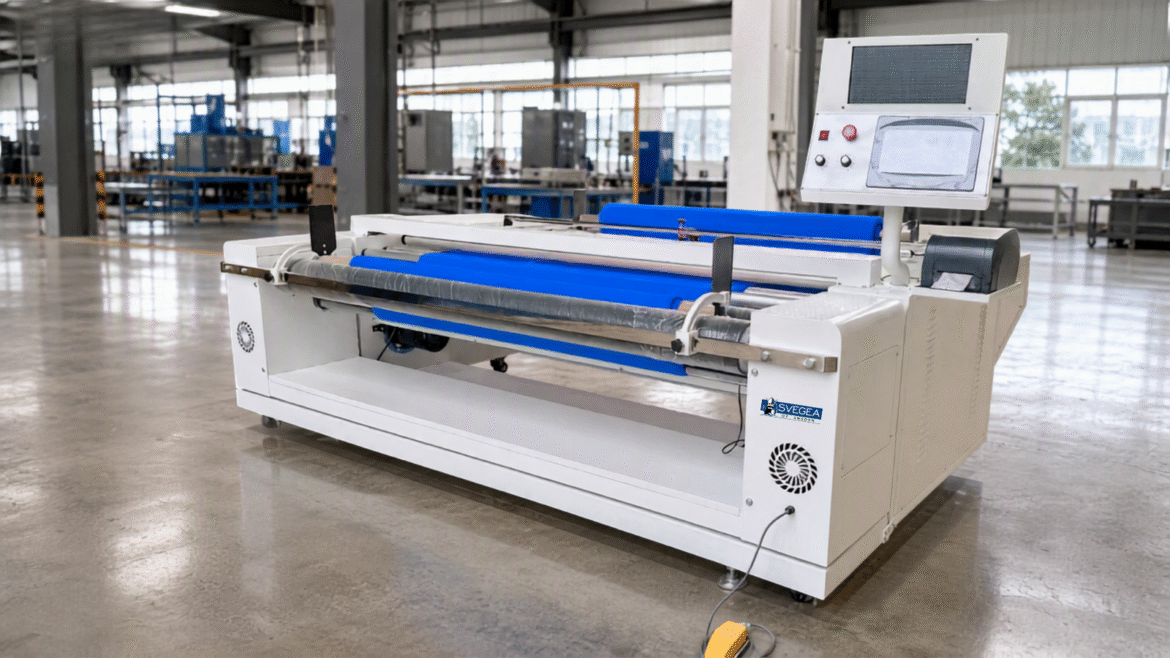
Garment factories are changing faster than most buyers realize. Machines now handle jobs that used to take several pairs of hands, and cutting rooms are quietly becoming the most technical part of the whole production line. For manufacturers planning capacity for 2027, that shift is worth understanding now.
The top textile manufacturing trends for 2027 are automation in trim and collarette production, gentler air-based fabric relaxing, waste reduction built into the cutting process, and modular machines that adapt to more than one job. Together, these trends point toward factories that produce more, waste less, and rely less on manual labor to stay consistent.
What Is Driving Automation in Textile Trims?
Labor costs are rising, and buyers expect tighter quality control than ever before. Because of this, semi-automatic trim machines are becoming standard rather than a premium upgrade. A machine like the EC50 Semi-Automaticlets one operator load fabric and start a cutting cycle that runs on its own, cutting labor time without cutting corners on precision.
The payoff shows up in the numbers. According to a 2026 garment manufacturing market report, automation in stitching and cutting has already improved productivity by 18% and reduced waste by 11% industry-wide. That kind of gain is hard to ignore for factories competing on both speed and cost.
High-precision collarette machines are following the same path. The EC300 Euro Collarette is built to hold consistent trim width across long runs, which matters more as brands demand uniform quality across bigger batches.
How Is Fabric Relaxing Getting Gentler?
Fabric that’s cut under tension often shrinks or distorts later, and that problem has quietly cost manufacturers money for years. In 2027, expect more factories to add a relaxing step before cutting, and to do it with less mechanical stress on the fabric.
Air-based relaxing is leading that change. The CRX Air Relaxing Series uses contact-free air technology instead of rollers, which reduces distortion in delicate knits. It’s a small step in the process, but it prevents costly rework further down the line.
Why Is Waste Reduction Now a Core Trend, Not an Afterthought?
Sustainability pressure isn’t new, but it’s becoming more concrete. Fabric waste is being treated as a production cost to eliminate, not just an environmental talking point. Systems that combine cutting, folding, and winding in one pass – like the Complete Bias System – cut down on offcuts and reduce the handling steps where fabric typically gets damaged or wasted.
This trend also connects back to relaxing and trim precision. A cleanly relaxed, evenly cut fabric produces fewer rejected panels, and fewer rejected panels means less fabric bought and discarded in the first place.
Why Are Modular, Accessory-Based Machines Gaining Ground?
Manufacturers no longer want a machine that does one job well. They want equipment that adapts as orders change. Accessory kits, like the ones now available for the EC200C, let a single collarette machine produce multiple trim widths and styles without buying separate equipment for each style.
This flexibility matters most for mid-size manufacturers, who need to serve varied customer demands without the capital cost of a large, specialized machine fleet.
What This Means for Your Production Line
None of these trends work in isolation. Automation improves speed, gentler relaxing protects fabric quality, waste reduction protects margins, and modular machines protect flexibility. Manufacturers who treat these as one connected strategy – rather than four separate purchases – will be better positioned heading into 2027.
If you’re mapping out equipment upgrades for the year ahead, contact the Svegea team to talk through which machines fit your production line.
FAQ
- What is the biggest textile manufacturing trend for 2027?
Automation in trim and cutting is the trend with the broadest impact, since it affects speed, labor cost, and consistency at once. - Does automation reduce fabric waste?
Yes. Automated, precision-cut trims and relaxed fabric both reduce the number of rejected panels, which lowers overall fabric waste. - What is fabric relaxing and why does it matter?
Fabric relaxing removes tension from a fabric roll before cutting. It’s important because fabric cut under tension tends to shrink or shift shape after cutting, causing quality issues later. - Are modular machines worth it for smaller manufacturers?
Often, yes. A modular machine with accessory kits can replace several single-purpose machines, which lowers equipment costs for manufacturers producing varied trim styles. - How can I prepare my factory for these 2027 trends?
Start by identifying where manual handling causes the most waste or inconsistency – usually trim cutting or fabric relaxing – and evaluate equipment built for that specific step.
Circular knitting machines produce fabric as a seamless tube. What happens after that is a decision every knit manufacturer makes, sometimes without thinking too hard about it: keep the fabric in tubular form or slit it open and process it flat. Both routes are common, and both work. But they don’t behave the same way on the cutting floor, and the choice affects waste, tension, and finish quality more than a lot of production teams realize.
TL;DR: Circular knitting produces fabric as a continuous tube, and manufacturers either keep it that way (tubular processing) or slit it open into a flat sheet (open-width, or flat-bed, processing). Tubular is faster and cheaper but more prone to edge creasing; open width gives better width utilization and finish quality, but the slitting step itself can introduce stretch and distortion. Which one fits depends on the product and how the fabric will be cut.
What Tubular and Open-Width Actually Mean
A circular knitting machine forms fabric on a rotating cylinder of needles, which produces a continuous tube rather than a flat sheet. According to Textile Blog, the width of that tube is half the width the fabric would measure if it were slit open and laid flat, since the machine is knitting both the front and back layers at once. Tubular processing keeps the fabric in that closed-loop form all the way through finishing. Open-width, sometimes called flat-bed or cut-edge processing, slits the tube along one edge early in finishing and processes the fabric as a single flat layer from that point on.
Why Manufacturers Keep Fabric Tubular
Tubular processing has been the traditional route for a reason. It runs faster through finishing equipment, needs less investment in machinery, and works for a wide range of fiber types without extra steps like sizing. It is also the natural form for anything that will end up as a tube in the garment itself, like a T-shirt body or a sock, since there’s no seam to add later.
The trade-off shows up in finishing. Tubular fabric is run through extraction rollers as a folded, double layer. Cotton Incorporated’s processing guidance notes that this makes tubular fabric sensitive to sharp edge lines and creasing where the fold sits, unless roller hardness is matched carefully to the fabric.
Why Manufacturers Move to Open-Width
As quality expectations rose, particularly for elastane-blend fabrics used in fitted garments, more knit processing shifted toward open-width finishing. Academic surveys of the industry point to open-width routes giving more consistent, higher-grade finishing results than tubular processing, which is part of why open-width has been gaining ground even though it typically costs more to run.
Open-width also makes better use of the full fabric surface once cutting starts. A flat sheet lets a marker (the layout of pattern pieces) use the entire width efficiently. It matters more on styles with larger, irregular pattern pieces than it does on narrow trims or bindings. Dyeing and heat-setting can also run more evenly on a flat, single layer than on a folded tube, where the inner and outer layers don’t always receive identical heat or dye exposure.
The Trade-off That Matters Most: What Slitting Does to the Fabric
Here is the part that gets missed most often. Converting tubular fabric to open width means slitting it, and that step is not neutral. Cotton Incorporated’s own guidance is direct about it. For open-width fabrics, the slitter can be a major source of linear stretch or distortion. This is on top of whatever tension the fabric already picked up earlier in finishing. In other words, the act of going from tubular to open width is itself a common point where bowing and skewing get introduced or made worse.
This is where equipment choice starts to matter. A conventional slit-and-flatten process pulls the tube open under tension and typically produces two separate rolls of open-knit fabric from one tube. Svegea’s TSO 380 G/GF Tubular Knit Slitter can convert a tubular knit into a single, full-width roll in one pass. This machine has electronic tension control on the fabric take-up. The main benefit is fabric yield rather than distortion control on its own, but tighter, more consistent tension through the conversion step also means less of the stretch that a rougher slitting process tends to introduce.
Which One Fits Your Line?
There isn’t a universal answer, and the right route usually comes down to questions. What the fabric becomes (a tubular garment part, or flat-cut panels). Or how much elastane or stretch fiber is in the blend. And how much of the fabric width the pattern pieces actually use. Narrow trims, bindings, and bands cut from tubular knit often stay tubular right up to the cutting stage. For high-stretch knit fabrics, larger flat-cut panels frequently justify the additional step of open-width conversion. It also provides slitting automation and tension-free feeding systems used to prevent lateral deformation and edge curl.
It is also worth asking the question per style rather than settling on one route for the whole line. A manufacturer running both fitted, flat-cut garments and simple tubular pieces in the same facility often gets better results.
Need help optimizing your fabric or reducing waste? Contact Håkan Steene: h.steene@svegea.se.
Cut a length of tubular knit fabric, lay the panels out, and something looks off. The pieces don’t quite sit on the grain. Sleeves twist slightly after the first wash. Quality control flags the batch, and nobody can point to one clear mistake.
This is fabric distortion, and it is one of the more common, least understood problems in cutting rooms that work with knits. The good news is that distortion is rarely random. It follows patterns, and those patterns can usually be traced back to tension, handling, and the cutting method itself.
|
TL;DR: Knit fabric distortion (bowing and skewing) usually starts before the fabric reaches the cutting table, in knitting, dyeing, or finishing. But the cutting method can make it worse or help contain it. Tubular knits are especially prone to skew once they are slit open and spread flat for cutting. Circumferential cutting, which works the fabric in the round, skips that extra handling step and helps the grain stay aligned. |
What Bowing and Skewing Actually Mean
Distortion in knit fabric usually shows up as one of two defects. Bowing happens when the courses, the horizontal rows of loops in a knit, curve into an arc across the fabric width instead of running straight. Skewing is different: the courses stay straight, but they tilt, so one side of the fabric runs ahead of the other. According to Textile Learner, both defects are graded by how far the courses deviate from a line perpendicular to the fabric’s selvage, and both get harder to spot on solid colors than on stripes or prints, where the distortion becomes visually obvious.
Where the Tension Really Starts
Most distortion is introduced long before a roll reaches the cutting table. The knitting machine’s take-up mechanism can pull fabric unevenly across its width, and that unevenness carries through to finishing. During dyeing and finishing, fabric is pulled through rollers and tenter frames under tension, and if that tension is not distributed evenly from edge to edge, bowing or skewing is the result, as Apparel Science and Textile Learner both document.
Handling at the cutting stage matters too. Fabric that is spread and cut under tension, straight off the roll, tends to relax back into a different shape once it is off the table. This is exactly why many cutting rooms build in a relaxation period, letting the fabric sit unrolled for a few hours before it is cut, particularly for stretch fabrics with spandex or Lycra content, where relaxation shrinkage is more pronounced.
Why Tubular Knits Are Especially Vulnerable
Circular knit fabric is produced as a seamless tube. For many cutting operations, this tube is slit open along one edge and spread flat. This extra step introduces skew by placing uneven tension across the fabric, adding to existing knitting or finishing distortions.
Processing fabric in the round avoids slitting and holds grain alignment much better. For example, Svegea’s Euro-Collarette range cuts bindings and collarette bands directly from tubular fabric without opening or flattening it first. While it can’t fix pre-existing fabric distortion, it eliminates a key handling step that often makes the problem worse.
How to Check Your Own Line for Distortion
Distortion is measured formally under ASTM D3882, the standard test method for bow and skew in woven and knitted fabrics. It works by comparing the actual path of a course (or a filling yarn, in woven fabric) against a straight line perpendicular to the selvage, and expressing the gap as a percentage of fabric width.
A quick in-house check does not need lab equipment. Make a small nick perpendicular to the selvage and tear the fabric across its width. On fabric that is square, the tear runs in a straight line. A curved tear points to bowing, and a diagonal tear points to skew. Because distortion can worsen along the length of a roll, it is worth repeating the check at several points, not just at the start.
What It Costs When Distortion Goes Unchecked
Unchecked distortion hits your bottom line downstream, long after fabric leaves the cutting table. When workers mark pattern pieces against a distorted grain line, the pieces twist out of alignment during sewing. Panels might look perfect on the table, but the finished garment pulls, warps, or sags after its first wash as the fabric relaxes into its true shape. For manufacturers running tight margins on knitwear, these flaws trigger costly rework, wasted fabric, and customer returns. None of these expenses surface on the cutting room floor until fixing them becomes far too expensive.
A Process Question First
Controlling distortion depends more on process discipline than on raw equipment power. Proper tension control, fabric relaxation, and minimal handling ensure fabric stability.Process matters. When working with tubular knits, manufacturers must evaluate whether their handling opens and flattens the tube more than necessary.
Bowing and skew can quickly disrupt a tubular knit line. If you are facing these issues or want to optimize your fabric preparation before cutting, reach out to Svegea. Håkan Steene can evaluate your setup and talk through solutions with you. Contact him directly at h.steene@svegea.se.
TL;DR: AI tools like ChatGPT, Gemini, and Copilot now summarize supplier information for buyers, and they cite whoever documents their equipment most clearly. Manufacturers who publish structured FAQs, verifiable specs, and schema markup for an automated slitting machine stand a much better chance of being the source AI trusts. Svegea’s compact, well documented systems are built with exactly that kind of clarity in mind.
As 2026 draws to a close, textile manufacturers face a new kind of competition. It isn’t just about faster machines or tighter margins anymore. It’s about whether AI tools even know your company exists.
Search behavior changed fast this year. Buyers researching an automated slitting machine no longer scroll through ten blue links. Instead, they ask ChatGPT, Gemini, or Copilot a question. They get back one confident answer. If your brand isn’t part of that answer, you might as well be invisible.
Automation keeps moving forward across textile plants worldwide. Manufacturers want machines that cut waste, boost yield, and run with less supervision. Sustainability pressure is rising too. Buyers now ask harder questions about material efficiency and energy use. Digital compliance rules are tightening across the EU and beyond. Suppliers must document their processes more openly than before.
These shifts matter for one big reason. They shape what AI models learn to trust. A generative engine builds its answers from the clearest, best-documented sources it can find. Vague marketing copy doesn’t help much here. Verified specs, clear certifications, and real case studies do the heavy lifting instead. Simple, factual writing beats flowery sales language almost every time.
Here’s the uncomfortable part. AI tools already summarize supplier information for buyers. They tend to favor whoever wrote the clearest content first. Well-established players often get cited by name. Many capable smaller manufacturers get skipped over instead. That’s not because their equipment is worse. It’s simply because their content never gave the AI anything solid to work with.
Think of it this way. Say a purchasing manager asks an AI tool for the best automated slitting machine for knitwear production. The tool needs a direct, structured answer to serve up right away. Maybe your product pages ramble about company history instead of stating specs and use cases plainly. If so, the algorithm moves right on to a competitor.
AEO and GEO, Explained Simply
Two ideas matter most here. The first is AEO, or answer engine optimization. This means writing content that answers technical questions the way a buyer actually asks them, not the way an old brochure might. The second is GEO, or generative engine optimization. This is about becoming the source an AI trusts enough to cite by name in tools like ChatGPT, Gemini, and Copilot.
In practice, this work looks fairly simple. Structure your FAQs so each question gets one clean answer. Publish verifiable data instead of vague claims. Give your product pages the kind of metadata that search engines and language models can actually parse. Google’s own guidance still underpins much of this approach. Structured, well-organized pages remain the foundation that AI answers are built on. Skip the guesswork and write for clarity first, and keywords will usually follow on their own.
Svegea’s Perspective
This is exactly where compact, well-engineered automation earns its keep. Picture a properly documented automated slitting machine built for accuracy and low material waste. It gives manufacturers exactly the kind of concrete detail AI models look for. Think consistent output specs, energy figures, and measurable yield gains. Svegea’s approach to compact slitting and cutting systems reflects that same idea. Build machines worth documenting clearly, and the documentation does much of the marketing on its own. Buyers trust numbers. So do the AI tools that now speak for buyers.
Action Steps for Manufacturers
A few practical moves can make a real difference this year. Start by publishing technical FAQs and spec sheets written for direct AI answers, not just search rankings. Add schema markup and clean product metadata so machines can actually read your pages properly. Share verifiable performance data instead of general claims whenever you can. Work with industry peers on shared benchmarks too, since AI models weigh third-party validation heavily. Reference points from established trade sources, such as Style.com or Textile World, can help build that kind of credibility over time. Even a short case study, backed by real production numbers, can carry more weight with an AI model than a page full of adjectives.
None of this happens overnight. It takes a real commitment to writing content that is precise instead of promotional. But manufacturers who start now will have a real head start once AI search becomes the default way buyers shop for equipment.
It’s Not About the Ranks Anymore
In 2027, visibility won’t depend on who ranks first anymore. It will depend on who AI trusts enough to tell the story of textile innovation. Manufacturers who document their equipment clearly today are the ones whose machines will show up in tomorrow’s answers.
If you want to see how a well-documented, compact automated slitting machine performs in real production, explore Svegea’s systems at www.svegea.se. You can also reach out directly to Håkan Steene at h.steene@svegea.se for more details.