Garment factories are changing faster than most buyers realize. Machines now handle jobs that used to take several pairs of hands, and cutting rooms are quietly becoming the most technical part of the whole production line. For manufacturers planning capacity for 2027, that shift is worth understanding now.
The top textile manufacturing trends for 2027 are automation in trim and collarette production, gentler air-based fabric relaxing, waste reduction built into the cutting process, and modular machines that adapt to more than one job. Together, these trends point toward factories that produce more, waste less, and rely less on manual labor to stay consistent.
What Is Driving Automation in Textile Trims?
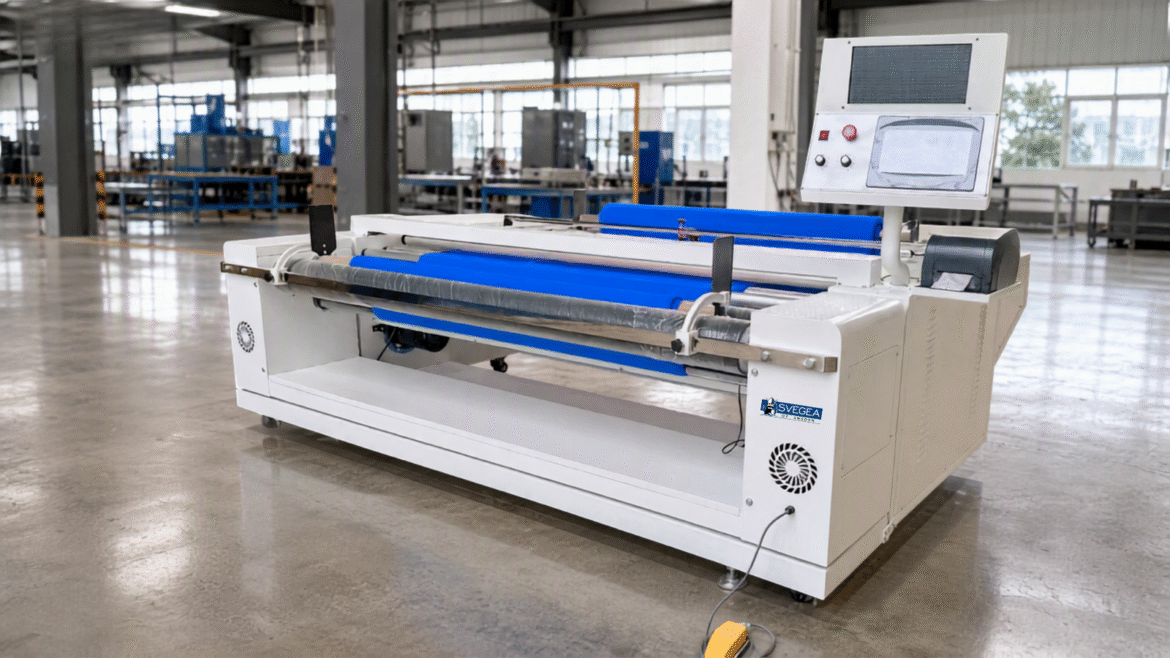
Labor costs are rising, and buyers expect tighter quality control than ever before. Because of this, semi-automatic trim machines are becoming standard rather than a premium upgrade. A machine like the EC50 Semi-Automaticlets one operator load fabric and start a cutting cycle that runs on its own, cutting labor time without cutting corners on precision.
The payoff shows up in the numbers. According to a 2026 garment manufacturing market report, automation in stitching and cutting has already improved productivity by 18% and reduced waste by 11% industry-wide. That kind of gain is hard to ignore for factories competing on both speed and cost.
High-precision collarette machines are following the same path. The EC300 Euro Collarette is built to hold consistent trim width across long runs, which matters more as brands demand uniform quality across bigger batches.
How Is Fabric Relaxing Getting Gentler?
Fabric that’s cut under tension often shrinks or distorts later, and that problem has quietly cost manufacturers money for years. In 2027, expect more factories to add a relaxing step before cutting, and to do it with less mechanical stress on the fabric.
Air-based relaxing is leading that change. The CRX Air Relaxing Series uses contact-free air technology instead of rollers, which reduces distortion in delicate knits. It’s a small step in the process, but it prevents costly rework further down the line.
Why Is Waste Reduction Now a Core Trend, Not an Afterthought?
Sustainability pressure isn’t new, but it’s becoming more concrete. Fabric waste is being treated as a production cost to eliminate, not just an environmental talking point. Systems that combine cutting, folding, and winding in one pass – like the Complete Bias System – cut down on offcuts and reduce the handling steps where fabric typically gets damaged or wasted.
This trend also connects back to relaxing and trim precision. A cleanly relaxed, evenly cut fabric produces fewer rejected panels, and fewer rejected panels means less fabric bought and discarded in the first place.
Why Are Modular, Accessory-Based Machines Gaining Ground?
Manufacturers no longer want a machine that does one job well. They want equipment that adapts as orders change. Accessory kits, like the ones now available for the EC200C, let a single collarette machine produce multiple trim widths and styles without buying separate equipment for each style.
This flexibility matters most for mid-size manufacturers, who need to serve varied customer demands without the capital cost of a large, specialized machine fleet.
What This Means for Your Production Line
None of these trends work in isolation. Automation improves speed, gentler relaxing protects fabric quality, waste reduction protects margins, and modular machines protect flexibility. Manufacturers who treat these as one connected strategy – rather than four separate purchases – will be better positioned heading into 2027.
If you’re mapping out equipment upgrades for the year ahead, contact the Svegea team to talk through which machines fit your production line.
FAQ
- What is the biggest textile manufacturing trend for 2027?
Automation in trim and cutting is the trend with the broadest impact, since it affects speed, labor cost, and consistency at once. - Does automation reduce fabric waste?
Yes. Automated, precision-cut trims and relaxed fabric both reduce the number of rejected panels, which lowers overall fabric waste. - What is fabric relaxing and why does it matter?
Fabric relaxing removes tension from a fabric roll before cutting. It’s important because fabric cut under tension tends to shrink or shift shape after cutting, causing quality issues later. - Are modular machines worth it for smaller manufacturers?
Often, yes. A modular machine with accessory kits can replace several single-purpose machines, which lowers equipment costs for manufacturers producing varied trim styles. - How can I prepare my factory for these 2027 trends?
Start by identifying where manual handling causes the most waste or inconsistency – usually trim cutting or fabric relaxing – and evaluate equipment built for that specific step.
Autumn is creeping back in, and with it, the trench coat is coming out of storage again. Scroll through any fashion feed right now and you’ll see it: belted, oversized, thrown over a slip dress or buttoned up over a suit. It never really goes away, but every September it seems to reintroduce itself as the season’s must-have layer.
We’ve watched this coat cycle through fashion for years from our side of the industry — the manufacturing side. And here’s the thing most style articles won’t tell you: the reason a good trench coat still looks sharp after a decade of wear has almost nothing to do with the belt or the buttons everyone photographs. It’s buried inside the collar, the lapel, and the lining, in a set of narrow fabric strips most wearers never think about.
A Coat Built Like a Small Structure
Thomas Burberry patented gabardine back in 1879, engineering it specifically to be waterproof without the stiffness of rubberized rainwear. That original goal — weather resistance without bulk — is still what separates a real trench coat from a coat-shaped raincoat. But weatherproof fabric alone doesn’t explain why a well-made trench holds its collar stand or keeps its lapels from curling after years of use.
That comes down to internal reinforcement: collar stays, lapel interlining, and the strapping used for belts and epaulettes. Unlike a lightweight dress or blouse, a trench coat carries real structural weight. Heavy gabardine, dense twill, sometimes multiple bonded layers — none of it behaves the way thin fabric does under a sewing machine, and none of it forgives sloppy internal construction.
So while the outer fabric gets all the design credit, it’s these hidden strips of interlining and tape that decide whether the coat ages gracefully or starts sagging at the shoulders by its second winter.
What Those Hidden Strips Actually Do
A few things happen when a manufacturer gets this part right:
- The collar stands up crisply instead of collapsing, even on a heavy double-layered lapel.
- Belt loops and cuff straps stay straight and don’t twist over time.
- The fabric doesn’t fray internally where it’s under the most tension — shoulders, waist, collar edge.
- The coat keeps its shape wash after wash, season after season.
None of this shows up in a product photo. You notice it later, the first time you flip your collar up against a cold wind and it actually stays put.
Where Hand-Cutting Runs Out of Road
A skilled tailor working on a single bespoke coat can cut collar stays and waist strapping by hand, with shears and a steady eye. It works, at that scale.
It doesn’t work at factory scale. Once a manufacturer is producing thousands of coats a season, hand-slitting heavy rolls introduces the kind of inconsistency that ruins a production run: frayed edges from blade friction, strips that come out a millimeter or two off-width, automated sewing lines thrown out of alignment because the input material isn’t uniform. Multiply a small error by ten thousand units and it stops being small.
This is the point where most outerwear manufacturers move to dedicated slitting equipment. And it’s the part of the process we spend most of our time thinking about.
Where We Come In
At Svegea, we build roll slitting and band cutting machines designed around exactly this problem: cutting dense, heavy fabric into narrow, consistent strips without the fraying, stretching, or width drift that ruins a production batch.
A few things our machines are built to handle:
1. Consistent width across the whole roll. The strip you cut at meter one should match the strip at meter one thousand.
2. Clean edges on dense material. Automatic blade sharpening keeps friction and heat from fraying heavier fabrics like gabardine or bonded interlining.
3. Tension control that doesn’t distort the weave. Heavy woven fabric under the wrong tension stretches unevenly, and that shows up later as puckering.
We didn’t design this equipment with trench coats specifically in mind — it’s used across tailored blazers, technical rainwear, and industrial textiles too — but outerwear is where the margin for error is smallest. Dark, structured coats show every flaw in daylight.
The Part Nobody Photographs
There’s a reason this kind of detail rarely makes it into a fashion write-up. It’s not glamorous. Nobody’s Instagramming a roll of interlining tape. But it’s the difference between a coat that’s still in rotation a decade from now and one that’s in a donation bag by next spring.
If you’re on the manufacturing side and dealing with fraying, width inconsistency, or waste on heavy-fabric roll slitting, it’s worth a conversation — we’ve spent a long time solving exactly this problem. You can reach our engineering team through svegea.se, or explore the equipment lineup on the same site.
Either way, next time you flip up a trench coat collar against the wind, you’ll know what’s actually holding it there.
The Silent Language of Textiles
TL;DR: Touch is the first sense you ever develop, and fabric never stops talking to it. Long after you’ve stopped noticing color or cut, texture is still quietly running the show, calming a classroom, steadying a hospital ward, convincing a hotel guest they’ve arrived somewhere special. The science backs this up. So does the machinery that keeps a fabric’s feel consistent, batch after batch.
Touch Talks First, and It Never Really Stops
Run your hand across cashmere, then linen, then a coarse wool blanket. You don’t need a vocabulary lesson to know how each one makes you feel. Your body reacts before your brain finishes the sentence.
That’s not a coincidence. It’s a nine-month head start.
Touch is the first sense to develop in the womb, arriving around the eighth week of gestation, well before sight, hearing, or the ability to have an opinion about anything. Sensory receptors wake up first around the mouth and nose, then spread across the rest of the body over the following weeks. By the time a baby takes its first breath, touch already has months of practice logged. Fabric just keeps that conversation going.
Why Texture Beats Color to the Punch
Marketing teams love a good color story, and fair enough, color is loud and photogenic. But texture works in a quieter room: your nervous system, which reacts before your conscious mind gets a vote.
A 2024 study in PLOS ONE measured how tactile sensitivity shapes the way people rate fabric texture, confirming what mills have long suspected by feel alone: touch perception can be measured and predicted, not just guessed at.
Research published in the Spanish Journal of Marketing pushed the point further. After interviewing industry experts, the authors found that of the four qualities people notice by touch- texture, weight, temperature, and hardness- texture dominates how a product gets judged in someone’s hands. Shoppers decide with their fingertips. Their brains just write the caption afterward.
Where This Actually Plays Out
Picture a classroom in soft, breathable uniforms. Kids fidget less and focus more, because nothing scratchy is competing for their attention. Picture a hospital bed dressed in gentle linens instead of stiff, clinical ones. Shoulders drop a little faster. Picture a five-star hotel robe with real weight to it, sheets with a thread count you can feel before anyone announces the number. The room has already made its case before a single staff member says a word.
None of that happens by accident. It happens because someone understood that texture does emotional work whether a brand plans for it or not.
A World Woven in Texture
Travel far enough and texture starts speaking in dialects. Silk carries centuries of ceremony in Japan. Kente cloth, hand-woven in raised patterns across West Africa, tells stories of heritage and status that a photo alone can’t capture. Dense wool in Scandinavia is less a style choice than a survival strategy that eventually became culture, resilience spun into every fiber to get through a brutal winter.
These aren’t just materials. They’re identities, worn on the body and handed down.
The Blind Spot Nobody’s Solved Yet
E-commerce cracked color, cracked fit charts, mostly cracked video. It has not cracked touch. Researchers testing simulated haptic feedback in online apparel shopping found that screens still can’t replicate the confidence a customer gets from actually handling a fabric. Until touchscreens catch up, the only honest way to sell texture online is to describe it relentlessly: fiber content, weight, weave, finish, and photography that doesn’t oversell the hand-feel it can’t actually deliver.
The Unglamorous Part Nobody Photographs
Here’s the part that never makes the mood board: none of the feelings above survive an inconsistent production line. A designer can imagine the perfect hand-feel for a fabric, but if the machinery behind it drifts from batch to batch, that feeling never reaches the person wearing it.
That’s the role Svegea of Sweden plays, and it’s a deliberately unglamorous one. We don’t design the emotional experience of a textile; the manufacturers do that. What precision engineering does is make sure the texture a designer imagined is the texture that actually ships, consistently, so mills can spend their energy on the parts that require imagination instead of fighting variance on the floor.
The Actual Point
Stop designing only for how a fabric photographs. Start designing for how it will feel against skin, in the middle of an ordinary Tuesday, when nobody’s paying attention and the fabric is doing its job anyway. Texture is already telling a story. The only real choice is whether you’re the one writing it.
To talk through what consistent, imagination-ready production could look like for your line, reach out to Håkan Steene directly at h.steene@svegea.se, or visit www.svegea.se.
Cut a length of tubular knit fabric, lay the panels out, and something looks off. The pieces don’t quite sit on the grain. Sleeves twist slightly after the first wash. Quality control flags the batch, and nobody can point to one clear mistake.
This is fabric distortion, and it is one of the more common, least understood problems in cutting rooms that work with knits. The good news is that distortion is rarely random. It follows patterns, and those patterns can usually be traced back to tension, handling, and the cutting method itself.
|
TL;DR: Knit fabric distortion (bowing and skewing) usually starts before the fabric reaches the cutting table, in knitting, dyeing, or finishing. But the cutting method can make it worse or help contain it. Tubular knits are especially prone to skew once they are slit open and spread flat for cutting. Circumferential cutting, which works the fabric in the round, skips that extra handling step and helps the grain stay aligned. |
What Bowing and Skewing Actually Mean
Distortion in knit fabric usually shows up as one of two defects. Bowing happens when the courses, the horizontal rows of loops in a knit, curve into an arc across the fabric width instead of running straight. Skewing is different: the courses stay straight, but they tilt, so one side of the fabric runs ahead of the other. According to Textile Learner, both defects are graded by how far the courses deviate from a line perpendicular to the fabric’s selvage, and both get harder to spot on solid colors than on stripes or prints, where the distortion becomes visually obvious.
Where the Tension Really Starts
Most distortion is introduced long before a roll reaches the cutting table. The knitting machine’s take-up mechanism can pull fabric unevenly across its width, and that unevenness carries through to finishing. During dyeing and finishing, fabric is pulled through rollers and tenter frames under tension, and if that tension is not distributed evenly from edge to edge, bowing or skewing is the result, as Apparel Science and Textile Learner both document.
Handling at the cutting stage matters too. Fabric that is spread and cut under tension, straight off the roll, tends to relax back into a different shape once it is off the table. This is exactly why many cutting rooms build in a relaxation period, letting the fabric sit unrolled for a few hours before it is cut, particularly for stretch fabrics with spandex or Lycra content, where relaxation shrinkage is more pronounced.
Why Tubular Knits Are Especially Vulnerable
Circular knit fabric is produced as a seamless tube. For many cutting operations, this tube is slit open along one edge and spread flat. This extra step introduces skew by placing uneven tension across the fabric, adding to existing knitting or finishing distortions.
Processing fabric in the round avoids slitting and holds grain alignment much better. For example, Svegea’s Euro-Collarette range cuts bindings and collarette bands directly from tubular fabric without opening or flattening it first. While it can’t fix pre-existing fabric distortion, it eliminates a key handling step that often makes the problem worse.
How to Check Your Own Line for Distortion
Distortion is measured formally under ASTM D3882, the standard test method for bow and skew in woven and knitted fabrics. It works by comparing the actual path of a course (or a filling yarn, in woven fabric) against a straight line perpendicular to the selvage, and expressing the gap as a percentage of fabric width.
A quick in-house check does not need lab equipment. Make a small nick perpendicular to the selvage and tear the fabric across its width. On fabric that is square, the tear runs in a straight line. A curved tear points to bowing, and a diagonal tear points to skew. Because distortion can worsen along the length of a roll, it is worth repeating the check at several points, not just at the start.
What It Costs When Distortion Goes Unchecked
Unchecked distortion hits your bottom line downstream, long after fabric leaves the cutting table. When workers mark pattern pieces against a distorted grain line, the pieces twist out of alignment during sewing. Panels might look perfect on the table, but the finished garment pulls, warps, or sags after its first wash as the fabric relaxes into its true shape. For manufacturers running tight margins on knitwear, these flaws trigger costly rework, wasted fabric, and customer returns. None of these expenses surface on the cutting room floor until fixing them becomes far too expensive.
A Process Question First
Controlling distortion depends more on process discipline than on raw equipment power. Proper tension control, fabric relaxation, and minimal handling ensure fabric stability.Process matters. When working with tubular knits, manufacturers must evaluate whether their handling opens and flattens the tube more than necessary.
Bowing and skew can quickly disrupt a tubular knit line. If you are facing these issues or want to optimize your fabric preparation before cutting, reach out to Svegea. Håkan Steene can evaluate your setup and talk through solutions with you. Contact him directly at h.steene@svegea.se.
TL;DR
Garment manufacturers can significantly reduce textile waste and improve fabric utilization by implementing advanced material optimization strategies. Traditional methods often cause material distortion and feeding errors, leading to high downstream rejects. Upgrading to advanced slitting and cutting systems with synchronized feeding—such as the Svegea CMS 1800A2 and Euro-Collarette series—ensures precision fabric cutting and minimizes costly edge scrap.
Material costs are the largest single expenditure in garment manufacturing, often accounting for up to 60% of total production expenses. Despite this financial weight, typical cutting room operations still generate substantial amounts of fabric scrap. When factories mismanage fabric utilization in garment manufacturing, they face a dual penalty: tight profit margins shrink further, and environmental footprints expand.
To break this cycle, forward-thinking manufacturers are moving away from passive handling. They are adopting active material optimization strategies instead. This shift requires an understanding of how raw textiles behave under mechanical stress. It also requires deploying advanced precision fabric-cutting hardware to prevent waste before it happens.
The True Cost of Downstream Fabric Waste
Many factory managers view fabric waste as an inevitable byproduct of the cutting room floor. However, a significant portion of this waste stems from mechanical inaccuracies during initial processing. When raw fabric rolls are sliced into component strips or binding bands, traditional machinery often pulls the material unevenly.
This tension creates minor distortions across the textile web. While these imperfections may seem negligible at first glance, they manifest as major defects during downstream sewing. Stretched or misaligned fabric strips cause skewed seams, puckering, and uneven collars. Consequently, quality control teams must reject the finished garments.
By addressing material distortion at the source, manufacturers can prevent these costly errors. According to industry studies on sustainable manufacturing from organizations like the Ellen MacArthur Foundation, optimizing raw material processing is the most effective way to eliminate industrial textile waste.
The Role of Synchronized Feeding in Fabric Utilization
How do modern production facilities achieve perfect alignment without wasting valuable material? The answer lies in automated, synchronized feeding mechanisms.
When a cutting system pulls fabric from a roll or fold without precise speed regulation, the material stretches. Knitted fabrics are especially vulnerable to this tension, which alters their natural relaxation state. High-yield textile machinery solves this issue by matching the feeding speed exactly with the cutting mechanism speed.
[Fabric Roll Supply] —> (Automated Speed Sync) —> [Precision Cutting Blade] —> Zero-Tension StripSynchronized feeding ensures the textile remains completely relaxed as it meets the blade. This precision eliminates the traditional “buffer zone”—the extra material managers typically add to accommodate fabric shrinkage or shifting. By removing this buffer, factories achieve tighter nesting patterns and significantly improve overall fabric utilization.
Engineering Precision into the Cutting Room
Achieving high-yield textile production requires mechanical stability and smart automation. Manual cutting processes are simply too variable to meet modern tolerance requirements. To achieve repeatable precision, manufacturers rely on specialized systems designed for specific cutting challenges.
Roll Slitting and Strip Cutting Efficiency
For operations that process woven or synthetic rolls into binding strips, the stability of the blade and carriage is critical. Advanced units utilize automated Programmable Logic Controller (PLC) systems to manage the knife carriage movement. This technology allows operators to pre-program exact dimensions, ensuring that every cut remains identical from the first meter to the last.
For example, equipment like the Svegea CMS 1800A2 Strip Cutter uses an enclosed knife carriage and digital settings to deliver clean cuts across widths ranging from 5 mm to 1800 mm. This versatility allows factories to maximize the use of every roll, converting edge scrap into usable product components.
Eliminating Waste in Tubular Knit Processing
Tubular knitted fabrics present unique handling challenges due to their inherent elasticity. Standard cutting methods often flatten and distort the tube, leading to uneven edges and wasted center sections.
Advanced options like the Svegea Euro-Collarette Series overcome this issue by utilizing specialized internal fabric guides and variable speed controls. Systems such as the fully automatic Euro-Collarette 200CS feature electronic soft start and stop functions. This feature prevents the initial fabric jerk that frequently ruins the first few meters of a run.
By maintaining uniform tension throughout the entire cutting cycle, these specialized collarette cutters allow manufacturers to extract maximum material value with virtually zero waste.
The Financial Impact of High-Yield Machinery
Upgrading to high-yield machinery alters the financial landscape of a garment factory. When you reduce textile waste by even a small percentage, the cumulative savings over a fiscal year can be substantial.
| Operational Metric | Legacy Cutting Systems | Advanced Optimized Machinery |
| Average Material Waste Rate | 8% – 12% | Less than 2% |
| Fabric Tension Control | Manual / Unsynchronized | Automated PLC / Speed Synchronized |
| Downstream Reject Rates | Moderate (due to strip distortion) | Exceptionally Low (consistent dimensions) |
| Setup and Changeover Time | High (manual scaling and resets) | Low (pre-programmed digital recipes) |
Minimizing waste also helps manufacturers comply with increasingly strict international environmental standards. The European Environment Agency continues to push for circularity and waste reduction within the textile sector. Adopting advanced cutting technology helps brands meet these regulatory demands while simultaneously lowering their raw material procurement costs.
Strategic Implementation for Factory Managers
Transitioning to an optimized, low-waste cutting room requires a systematic approach. Factory managers should begin by auditing their current waste streams to identify where the largest volume of scrap occurs. If the majority of scrap consists of uneven roll edges or distorted binding strips, the mechanical feeding system is likely the root cause.
Investing in machinery that features automated speed synchronization, robust blade guidance, and flexible width adjustments will solve these issues. Furthermore, choosing systems with intuitive digital interfaces ensures that operators can switch between different fabric profiles quickly and accurately, reducing human error during setup.
Optimize Your Production Yield
Reducing textile waste requires the right balance of mechanical precision and automated control. If you want to eliminate material distortion, improve your fabric utilization, and protect your manufacturing margins, upgrading your cutting room infrastructure is a critical next step.
For expert guidance on selecting the ideal slitting or collarette cutting configuration for your facility, contact Håkan Steene at h.steene@svegea.se to discuss your specific technical requirements.
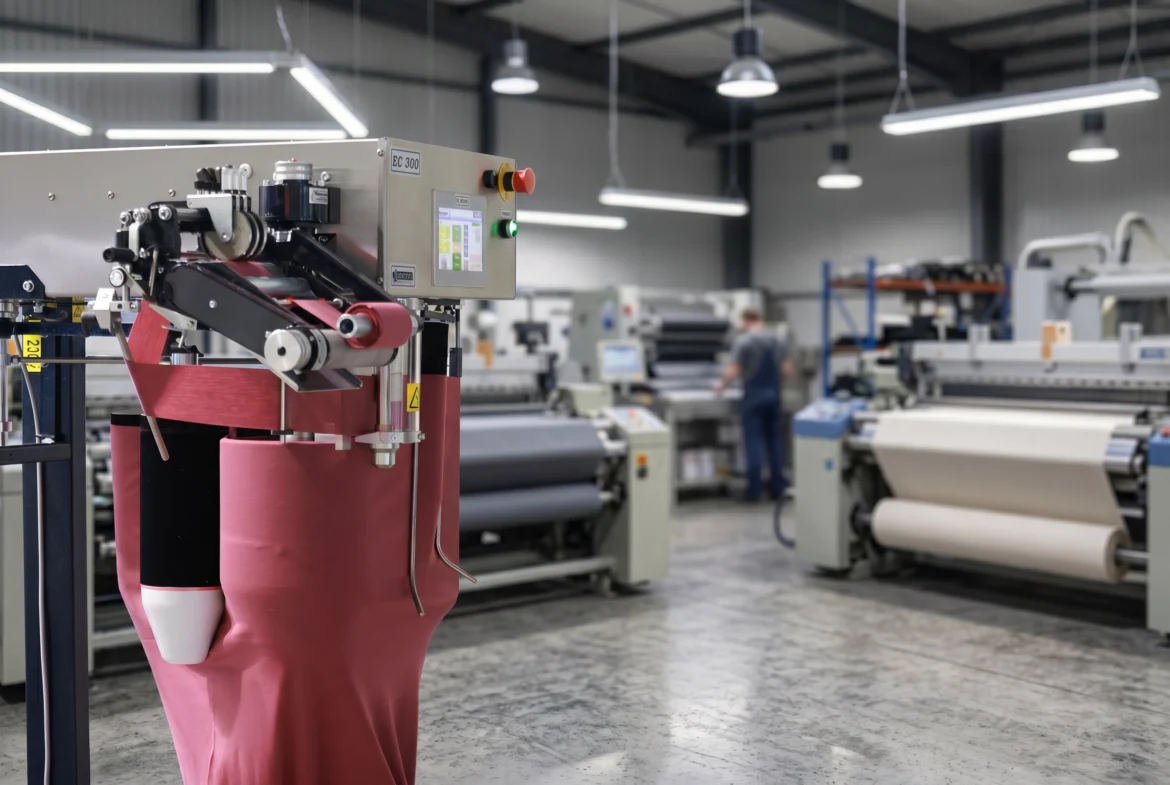
TL;DR
Single jersey and other technical knits curl and stretch the moment a blade touches them — it’s built into how the fabric is constructed, not a sign something’s broken. The real fix isn’t a slower line or a more attentive operator. It’s tensionless, synchronized feeding that lets the fabric arrive at the blade already relaxed, so the cut reflects the fabric’s true dimensions instead of a stretched, temporary one.
Every cutting room operator working with knits has seen it: the fabric looks fine going into the machine, then the cut edge curls, ripples, or comes out narrower than it should. It’s tempting to blame the operator, the blade, or the line speed. Usually, none of those are the real problem.
Curling Isn’t a Defect. It’s Physics.
Single jersey — the most common weft knit used in T-shirts, base layers, and casualwear — is built from loops, not interlaced threads like a woven fabric. The front face and back face of the loop structure sit under different tension. That imbalance is exactly what makes the fabric curl at a cut or unfinished edge. It’s a documented structural outcome of how the loops are formed, not a flaw in a specific roll of material.
Add tension during cutting, and the problem compounds. Research into how woven and knitted fabrics behave under bias and shear stress shows that fabric under load deforms elastically before it’s even cut. Meaning the shape you’re cutting isn’t the shape the fabric wants to hold once tension releases.
Cut it stretched, and it snaps back distorted the second it relaxes. For rib knits and technical tubular constructions, that snap-back doesn’t just cost a few millimeters of width — it throws off every downstream measurement that depends on that edge being accurate.
Where the Distortion Actually Comes From
Most knit distortion during cutting traces back to one of three points in the process:
- Manual tracking adjustments. An operator nudging the fabric to compensate for drift introduces exactly the kind of uneven pull that causes curling and skewed edges.
- Start-up jerk. The first few seconds of a run — before speed stabilizes — is when fabric gets yanked hardest, and it’s often where the worst distortion shows up.
- Unsupported tension zones. Any point where the fabric isn’t actively guided or supported is a point where it can twist, especially on tubular knits that want to roll along their own axis.
None of these are operator failures. They’re the predictable result of feeding elastic material through a system that isn’t built to account for how elastic material actually behaves.
Fabric under manual tension → cut applied → tension releases → edge curls / narrows / skewsWhat Tensionless, Synchronized Feeding Actually Fixes
The fix isn’t better technique. It’s removing tension from the equation before the blade ever touches the fabric.
Synchronized feeding locks the speed of the fabric source to the speed of the cutting head, ensuring the material moves through the system without pulling or holding back at any point. When you achieve precise synchronization, the fabric reaches the blade in a relaxed state—meaning the blade cuts the fabric’s true, unstressed dimensions. The material never snaps back after you make the cut, because the feed system never stretched it in the first place.
This system delivers the biggest impact on the exact materials that cause the most headaches on a conventional line: single jersey, rib knits, and tubular technical knits, where the fabric’s very construction bakes in tension differences between layers or directions.
Where the Euro-Collarette Series Fits
We built the Euro-Collarette Series specifically around this problem.
Its electronic soft-start eliminates the initial jerk at the beginning of a run. By bringing the fabric up to cutting speed gradually rather than abruptly, the system prevents distortion right where it usually starts.
We designed the band and fabric guides specifically for technical tubular knits. They support and align the material through the cut, stopping it from twisting or rolling on its own. Pair this layout with variable cutting speeds that adapt to different knit constructions. The machine easily balances the structural differences between a tricky single jersey and a heavy rib knit instead of running everything at a single speed.
You get an edge that holds its true dimension run after run. No operator manual adjustments required.
Why This Matters Before the Sewing Line Ever Sees the Fabric
A distorted edge doesn’t announce itself at the cutting table.
It shows up two or three stations later. A panel that measured perfectly on the cutting log suddenly refuses to align with its counterpart at the sewing machine. By then, the true cost skyrockets far beyond the price of the fabric itself. You’re paying for the labor to catch the defect, pull the ruined panel, and recut a replacement from fresh stock.
Fix the edge early. Getting it right at the cutting stage remains the cheapest place in the entire production chain to solve this problem. Everywhere downstream, that same fix costs more.
See the Euro-Collarette Series in Action
It steals your line speed. It drives up rework and triggers constant assembly rejects. If edge distortion on technical knits is costing your factory time and money, you need to change your process. See how synchronized feeding and precision band guiding handle your fabric differently.
Visit the Euro-Collarette Series page for full specifications. Or reach out to Håkan Steene at h.steene@svegea.se to talk through your specific fabric and production setup.
TL;DR
Cutting rooms routinely lose 10-15% of raw material to scrap, and some estimates run even higher. Active material optimization tackles this head-on. Synchronized feeding, precision fabric cutting, and tight tension control let facilities keep more of the fabric they pay for. The payoff isn’t just a smaller waste pile — it’s fewer downstream rejects and a healthier margin on every roll.
Material costs eat up more than half the total production budget in apparel manufacturing. Yet the cutting room — the single biggest opportunity to control that cost — is still where factories lose the most. Manual layouts, inconsistent tension, and operator guesswork have turned scrap into something everyone accepts.
That tolerance is getting harder to justify. Researchers tracking cut-and-sew waste across the apparel supply chain put the number at roughly 10-15% of fabric discarded before it ever becomes a garment. This figure traces back to sustainability researcher Timo Rissanen and has held up across more recent industry reviews. A separate fact sheet on clothing and textile waste puts a similar figure on how much delivered fabric ends up on the cutting room floor (resource.stopwaste.org/fact-sheet/clothing-and-textiles). Multiply either number across a full production run, and the math stops being a rounding error.
Active material optimization is how factories claw that margin back. It pairs automated material handling with precision cutting technology so scrap gets designed out of the process instead of cleaned up after the fact.
What Fabric Scrap Actually Costs You
Every offcut and rejected panel costs a factory twice. First, you’ve already paid for material that never becomes a finished garment. Second, someone still has to handle and dispose of it — that’s labor and disposal fees on top of the wasted fabric itself.
The bigger issue is what bad cutting does further down the line. When tension drifts during cutting, panels warp slightly — not enough to catch in a quick inspection, but enough to pull unevenly once stitched. That mismatch shows up at the sewing stage as a reject, and now you’re paying to recut from fresh stock and eating the labor twice.
What “Active” Optimization Actually Means
Most cutting rooms run reactively: feed the roll in, let the operator adjust for wrinkles or tension shifts as they show up. Active material optimization flips that. Instead of reacting to problems after they appear, automated systems monitor and stabilize the material continuously through the cut.
Getting there means controlling three things at once:
- Mechanical alignment — keeping material square (or precisely on the bias) relative to the blade
- Tension control — preventing the stretch or compression that rollers introduce as fabric moves through the line
- Dimensional consistency — the same component width from the first meter of a roll to the last
Nail these three, and you can tighten margins between components, compress nesting layouts, and cut wide-trim waste dramatically.
Synchronized Feeding: Where Tension Control Actually Happens
Knitted and elastic fabrics are the hardest to get right. They stretch under the slightest pull, and if a blade cuts fabric while it’s under tension, the material snaps back to its relaxed shape the moment it’s released — and that snap-back is where dimensional errors come from.
Fabric under tension → cut applied → fabric relaxes → dimensional inaccuracy / scrap
Synchronized feeding solves this by locking the speed of the fabric source — a turntable, a roll support — to the speed of the cutting head itself. Svegea’s True-Drive II system, for example, uses electronic synchronization to remove physical pull on the material entirely, so fabric reaches the blade already relaxed. Cut on true dimensions instead of stretched ones, and the downstream warping that ruins components simply doesn’t happen.
Precision Fabric Cutting, By Machine Design
High-yield cutting machinery is the most direct lever a factory has for pulling waste out of the cutting room. It replaces manual guesswork with mechanical consistency.
The Svegea CMS 1800A2 Strip Cutter is a good example of what that looks like in practice — a PLC-controlled knife carriage paired with an integrated dust grinding unit, holding tight tolerances across a working width of up to 1650 mm. That consistency is what lets a machine extract more usable product from every roll, run after run.
The Svegea Euro-Collarette Series solves a related but different problem: guiding technical tubular knits, single jersey, and rib fabrics through variable cutting speeds without distortion. Its electronic soft-start eliminates the jerking motion that typically wastes fabric in the first few seconds of a run — a small detail, but one that adds up over hundreds of production cycles.
Traditional workflow:  manual feed → tension shifts → inconsistent widths → high scrap rate
Optimized workflow:    synchronized feed → controlled tension → precision cut → minimal waste margin
Waste Reduction Has to Live in the Workflow, Not Just the Machine
New equipment only gets you halfway. The other half is how the floor actually operates day to day, especially when dimensions change between orders.
In a lot of factories, changing cut dimensions still means stopping the line, manually adjusting blades, and running test cuts until the new size checks out — burning both time and fabric in the process. Flexible cutting systems with tool-free width adjustment and precise mechanical scales cut that changeover down to minutes, and the first cut of a new run comes out usable instead of scrap. That matters most for smaller, custom orders, where setup waste can otherwise eat the whole job’s margin.
Keeping It Working: A Few Habits Worth Building In
Optimization isn’t a one-time upgrade — it holds up better with a bit of ongoing discipline:
- Run a waste audit. Track scrap weight per shift against total fabric used to find where losses actually concentrate.
- Trace downstream rejects back to their source. When a sewn component gets rejected for distortion, follow it back to the original cutting or tension issue.
- Calibrate on a schedule. Blades and synchronization sensors drift over long runs — a routine maintenance schedule catches that before it shows up as scrap.
None of this is glamorous work, but it’s the difference between a cutting room that quietly bleeds margin and one that doesn’t.
Optimize Your Textile Cutting Efficiency
Curious how precision Swedish engineering could tighten up your cutting room, stabilize material tension, and cut fabric waste? For technical guidance, machinery specs, or a conversation about your production layout, reach out to Håkan Steene at h.steene@svegea.se or visit svegea.se.
A production line can look busy and still be losing time. Operators are cutting, sewing machines are running, and yet the order will not ship on schedule. When a plant manager traces the delay back far enough, it rarely starts at the sewing station. It starts earlier, in the unglamorous steps where tubular fabric gets slit, trimmed, and turned into usable binding or panels.
These early-stage bottlenecks are easy to miss because no single step looks like the problem. Each delay is small. Multiplied across a production run, though, three specific bottlenecks quietly decide whether a Q3 deadline gets hit or missed.
TL;DR: Garment manufacturing bottlenecks rarely announce themselves. They build up in manual trimming, inconsistent slitting speeds, and slow changeovers between fabric widths. Fabric slitting efficiency, achieved through tension control, automated edge tracking, and faster setup, directly addresses all three. Textile automation does not replace skilled operators; it protects their time for work that actually needs judgment.
Bottleneck One: Manual Trimming That Drifts Over a Shift
Most garment factories still ask operators to guide, align, or trim tubular fabric by hand at some point in the process. It is a reasonable setup for low volume. It becomes a liability at scale.
Human attention is not constant. A worker who trims fabric accurately at 8 a.m. will produce slightly uneven widths by 3 p.m., simply because sustained repetitive tasks wear down hand-eye precision. This is a well-documented feature of manual, repetitive work, not a comment on any individual operator’s skill.
The output of that drift shows up downstream, not on the cutting table. A binding strip that is a millimeter too narrow gets flagged during quality control. A neckline collarette that is slightly off-width causes a stitching problem on the sewing floor. By the time the issue is traced back to its source, the fabric has already been wasted, and the schedule has already slipped.
Bottleneck Two: Slitting Speed and Tension That Fight the Fabric
Tubular knit fabric holds tension from every process it has already passed through: knitting, dyeing, finishing, and winding. That stored tension does not disappear on its own. McKinsey research on apparel manufacturing notes that many apparel companies still run long, laborious, and largely linear production processes, which puts them at a real disadvantage as automation reshapes the competitive landscape. Slitting is one of the clearest places that disadvantage shows up on the factory floor.
When a slitting line pulls fabric through too fast or unevenly, the material stretches. It relaxes later, after cutting, and the panel or strip distorts. This is why some factories build in an oversized safety margin: cutting a little extra fabric so a distorted edge still falls within tolerance.
That margin is not free. It is fabric that gets bought, transported, stored, and then thrown away. Left unmanaged across a full production run, inconsistent tension is one of the more expensive garment manufacturing bottlenecks, because it hides inside a cost line that looks like normal waste rather than a fixable process problem.
TL;DR: Uneven slitting tension does not just create scrap. It creates fabric that appears usable, gets cut, and only reveals its distortion once it reaches the sewing line, where the cost of correction is much higher than the cost of the fabric itself.
Bottleneck Three: Changeovers That Stall the Whole Floor
Few factories run one fabric width all day. Between garment sizes, colorways, or contract specifications, a slitting or collarette line usually needs to stop, get manually readjusted, and start again. That changeover routine, if done by hand, can take a meaningful chunk of a shift.
The effect compounds when slitting and the next process, such as collarette or binding cutting, run as separate, disconnected stations. Rolls move between machines by hand, which adds handling time and introduces a real risk of stretching or damaging fabric that was already tensioned correctly.
Supply chain researchers have flagged a related pattern at the macro level. NetSuite’s 2025 apparel industry report found that most fashion supply chain leaders report ongoing operational challenges, and that companies often take far longer to plan and execute a response than their sales cycle allows. A factory floor with slow, manual changeovers is essentially running the same problem in miniature, order after order.
Why Fabric Slitting Efficiency Is the Fix, Not Just a Buzzword
“Textile automation” gets used loosely, so it helps to be specific about what actually resolves the three bottlenecks above. Three mechanical questions tend to matter most:
- Edge tracking: Does the machine follow the fabric edge automatically using a sensor or photocell, or does accuracy depend on an operator’s eye?
- Tension control: Is fabric fed at a controlled, even tension, or pulled through at whatever speed the line happens to be running?
- Changeover speed: Can width or size changes happen in minutes, or does every changeover mean a near-total teardown of the cutting head?
Answering these three questions honestly is a more useful audit than asking whether a factory is “automated” in general. McKinsey’s analysis of fashion sourcing trends points out that apparel-manufacturing automation is still developing overall, but that the technologies already available show real potential to offset cost and speed disadvantages, particularly at the fabric preparation stage where manual variation does the most damage.
What This Looks Like on a Real Production Line
Machines built specifically for tubular knit processing offer a useful reference point. Svegea’s Euro-Collarette Series, for instance, is designed around the same three questions raised above: automated fabric guides and variable cutting speed compensate for changes in fabric tension instead of fighting them, and width adjustments on the semi-automatic models can reportedly be made in minutes rather than requiring a full mechanical reset.
This is not a claim that one machine line solves every bottleneck in every factory. Fabric type, order volume, and existing floor layout all change the calculation. The point is that tension control, edge tracking, and fast changeovers are achievable engineering targets, not aspirational ones. Any tubular knit slitting or collarette cutting setup, regardless of manufacturer, can reasonably be measured against them.
Building a Simple Bottleneck Audit
For a plant manager trying to hit a strict Q3 deadline, a full equipment overhaul is rarely the first move. A short audit usually is:
- Track how often quality control rejects panels or bindings for width or edge inconsistency over one week.
- Time an actual changeover, start to finish, rather than relying on the estimate everyone assumes is true.
- Check whether fabric tension is actively controlled during slitting or simply a byproduct of line speed.
These three data points, collected honestly, usually indicate whether the bottleneck lies in equipment, training, or workflow design before any purchasing decision is made.
TL;DR: Garment manufacturing bottlenecks are solvable, but only once they are correctly located. Manual trimming, uncontrolled slitting tension, and slow changeovers are the three most common causes. Fabric slitting efficiency, built on edge tracking, tension control, and fast setup, addresses all three directly.
Talk Through Your Specific Setup
Every factory floor is different, and the right fix depends on fabric type, order volume, and current layout. If it would help to talk through where your bottlenecks are actually coming from, Håkan Steene can walk you through the specifics. Reach him directly at h.steene@svegea.se.
Key Takeaways: The modern apparel manufacturing floor is experiencing a massive digital transformation. Global shifts toward fast-turnaround production, volatile material costs, and rising sustainability mandates are forcing textile brands to rethink old processes. Historically, the cutting room relied almost entirely on manual calculations, mechanical setups, and historical operator intuition.
Today, the concept of the “Smart Factory” has moved from a buzzword to an essential operational strategy. At the core of this technical evolution is the integration of Industry 4.0 infrastructure. Cyber-physical systems, real-time cloud data, and automated textile machinery are changing how garments are constructed. For facilities specializing in underwear, sportswear, and basic apparel, optimizing the automated cutting of components like bindings and waistbands is critical to maintaining a healthy bottom line.
The Operational Bottleneck in Traditional Binding and Trim Production
In high-volume garment lines, small design elements often dictate overall production efficiency. Structural rib-knit bindings, waistbands, and collarette edges are perfect examples. These essential trims ensure elastic durability and structural integrity in everyday apparel. However, handling tubular knitted fabrics manually frequently creates major operational bottlenecks.
When factory operators rely on mechanical cutting tables or older, semi-automatic gear, maintaining precise tension is difficult. Tubular knit fabrics naturally stretch, curl, and warp depending on ambient room humidity and yarn composition. If tension fluctuates even slightly during the slitting process, the width of the cut binding varies.
The negative effects of inaccurate slitting ripple straight through the assembly line. Inconsistent strip widths lead to downstream sewing machine jams, broken needles, and misaligned seams. According to data tracked by the World Textile Information Network (WTIN), quality-related rejects and fabric reworks can drain up to 5% of a manufacturer’s annual revenue.
How a Modern Collarette Cutting Machine Fits Into the Smart Factory
A smart factory operates on a basic principle: every piece of machinery should function as an intelligent, data-driven node. A modern, automated collarette cutting machine addresses traditional trimming issues by replacing manual intervention with digital precision. Instead of treating fabric slitting as an isolated step, smart systems view trimming as an integrated part of the broader manufacturing workflow.
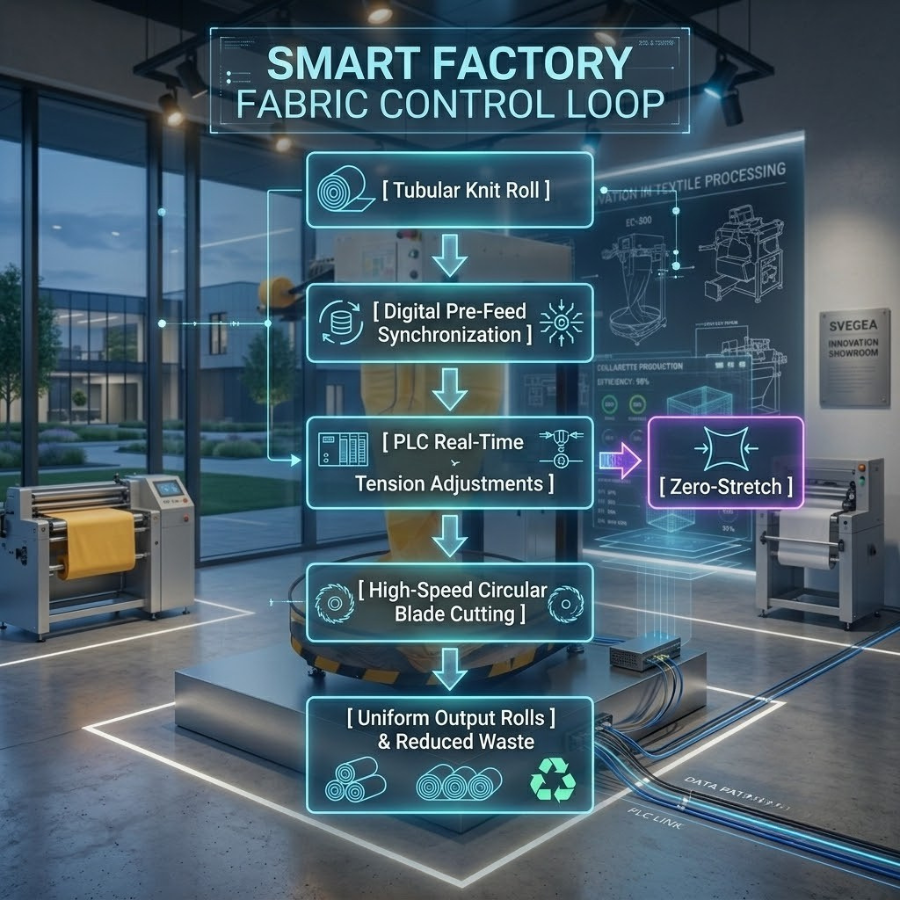
Modern automated cutters use Programmable Logic Controller (PLC) systems linked directly to internal network interfaces. This connectivity allows production managers to load cutting patterns and specifications instantly from central databases. The machinery automatically recalibrates for varying fabric weights or multi-band adjustments, minimizing human error during changeovers.
Furthermore, these smart systems rely on electronic speed synchronization. By coordinating the fabric turntable directly with the cutting drive, the material is fed to the circular blades at a perfectly consistent tension. This active control avoids the pulling and stretching that typically distort tubular textiles, ensuring uniform strips from the first meter to the last.
Reducing Textile Waste and Lowering Total Cost of Ownership
Material cost represents the largest percentage of an apparel factory’s operating expense. In traditional trimming rooms, scrap fabric—frequently referred to as “cabbage”—can average 15% to 20% of the total raw material roll. This volume of waste hurts profitability and directly conflicts with strict global sustainability criteria, such as standards outlined by the Sustainable Apparel Coalition (SAC).
Implementing automated cutting systems allows facilities to capture immediate material savings:
- High-Precision Edge Slitting: Automated guides minimize margin requirements, maximizing the usable width extracted from each tubular roll.
- Active Material Optimization: Synchronized feeding eliminates distorted fabric, saving material that would otherwise be discarded due to tension defects.
- Fewer Downstream Rejects: Delivering uniform, accurately cut strips directly to the sewing department prevents structural stitching errors and component scraps.
By minimizing fabric waste from 15% down to under 5%, high-capacity manufacturing lines can save tens of thousands of dollars annually on raw materials alone. Additionally, transitioning operators from tedious manual handling to managing advanced PLC interfaces creates a safer, more productive work environment.
Engineering Highlight: The Euro-Collarette Series
Engineers who want to bring these smart efficiencies onto their production floor often evaluate specialized Swedish machinery. The line of fully automatic cutters developed by Svegea of Sweden illustrates how automated design principles improve daily factory metrics.
For example, systems like the Euro-Collarette 300 Fully Automatic (EC 300) are engineered to handle high-demand production lines while maintaining tight tolerances. The equipment features integrated electronic speed synchronization and advanced touch-screen controls, allowing operators to quickly update parameters for multiple simultaneous bands.
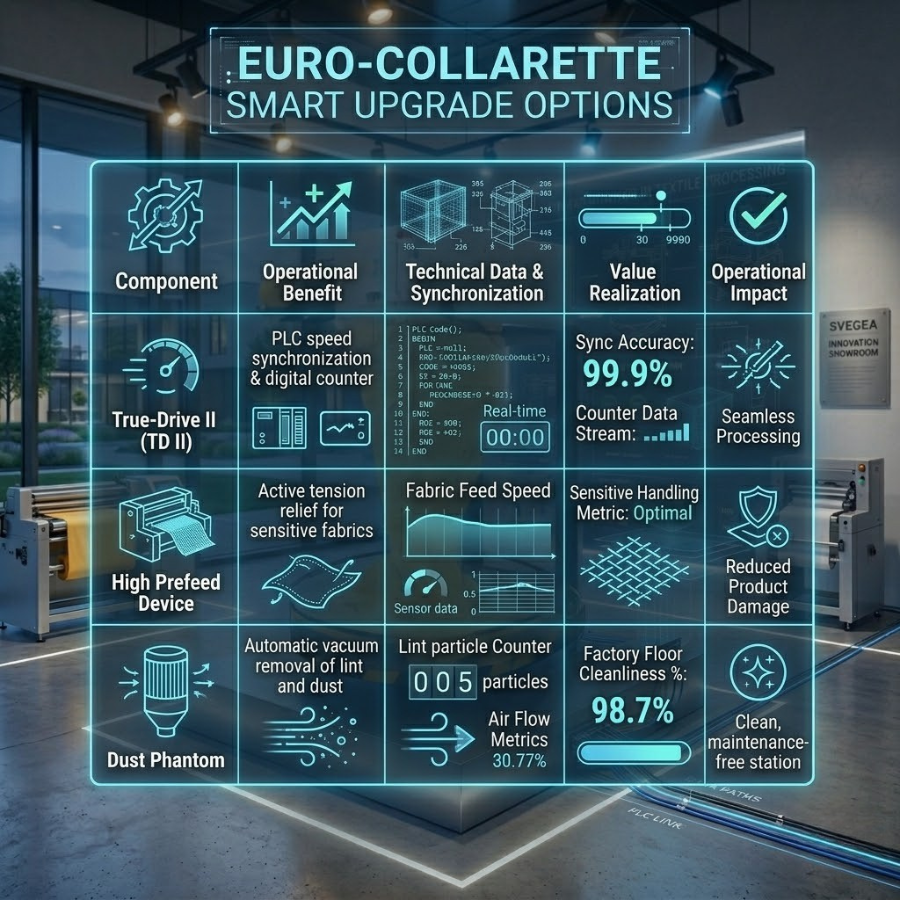
These configurations use advanced control add-ons like the True-Drive II (TD II). This system uses a dedicated PLC interface and integrated digital yard counters to ensure fabric synchronization. Additionally, accessories like the Dust Phantom vacuum system keep the cutting environment free of lint and debris, protecting sensitive electronics and creating a cleaner workspace.
Integrating Intelligent Cutting Automation into Your Supply Chain
Transitioning to a smart factory framework does not require replacing an entire facility’s equipment overnight. Instead, smart scaling involves identifying and upgrading the specific production points where material waste and labor bottlenecks cause the highest financial losses.
When looking at waistband fabrication and binding preparation, updating to a modern automated cutting system represents a highly reliable process improvement. Protecting fabric margins before material enters the sewing assembly line ensures that downstream automated sewing blocks function continuously without unexpected disruptions.
As digital automation continues to shape global apparel manufacturing, companies using connected, precise machinery will maintain a distinct advantage. Embracing smart textile engineering protects your margins, reduces factory floor waste, and keeps your production schedules predictable in a competitive market.
Optimize Your Production Floor Architecture
To learn more about how automated cutting systems can integrate with your facility’s workflows, contact Håkan Steene at h.steene@svegea.se for technical consultation, detailed equipment specifications, or calculated ROI assessments.
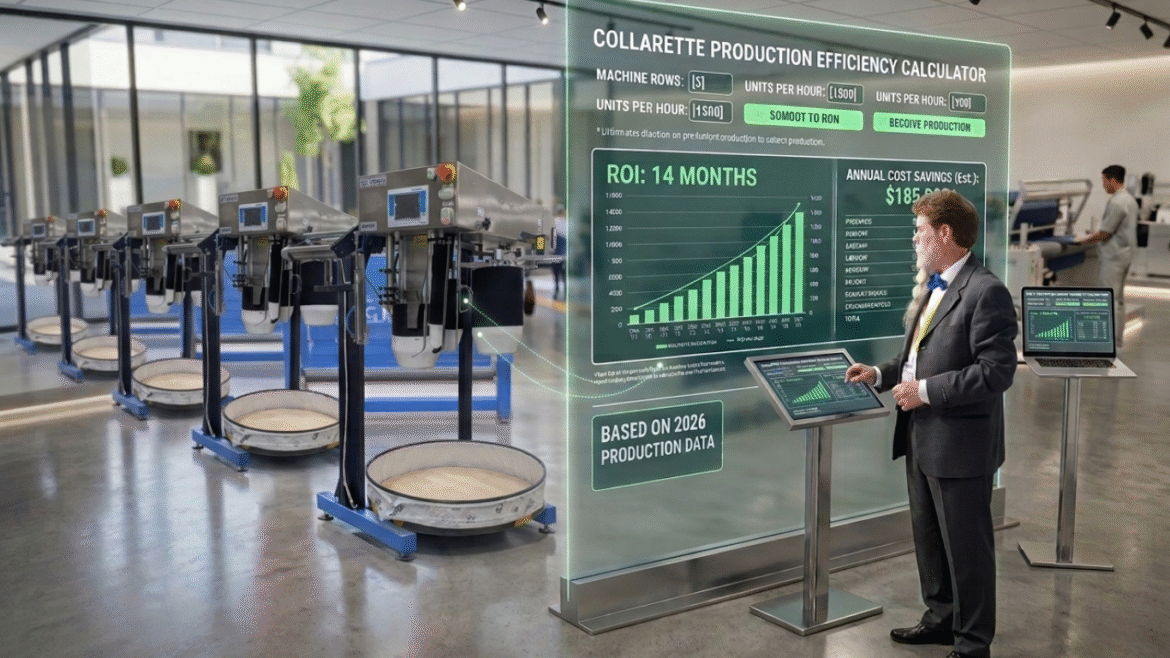
Profit margins in the textile industry often depend on the smallest details. In a high-volume garment factory, every centimeter of fabric and every second of labor counts toward the bottom line. As we move through 2026, CFOs and procurement officers are looking beyond the initial price tag of machinery. They are now focusing on a more critical metric: Textile slitting machine ROI.
While manual slitting has traditionally kept upfront costs low, it often hides “invisible” expenses that erode profitability. In contrast, automated systems provide a path toward altruistic manufacturing—where efficiency and worker well-being go hand-in-hand. This guide breaks down the financial logic of upgrading your cutting room.
TL;DR: The Financial Impact of Automation
-
- Direct Savings: Automated slitting reduces fabric waste by an average of 15% through precision edge-sensing.
- Labor Efficiency: One automated system typically replaces the output of three manual stations, reallocating labor to higher-value tasks.
- The ROI Formula: Annual Savings = (Manual Labor Cost + Waste Value) – (Automated Labor Cost + Maintenance).
- Payback Period: Most high-volume manufacturers achieve full ROI within 12 to 18 months.
The Hidden Costs of Manual Slitting
Many manufacturers view manual slitting as a flexible, low-risk operation. However, human variability introduces financial leaks that are difficult to track without granular data. Manual operators, regardless of their skill level, experience fatigue. This leads to inconsistent roll tension and slight cutting deviations.
When a roll is slit inaccurately, the downstream effects are costly. Inconsistent widths cause jamming in sewing machines or misaligned seams in the final garment. According to the World Textile Information Network (WTIN), quality-related rejects can cost a factory up to 5% of its annual revenue. By switching to a system with automated tension control, you essentially “plug” these financial leaks.
Quantifying the Efficiency Gap: Manual vs. Automated
To understand the textile slitting machine ROI, we must look at the hard data. Below is a comparison based on standard 2026 production metrics for mid-to-large-scale garment facilities.
| Metric | Manual Slitting Operation | Automated Slitting (Svegea) |
| Output per Hour | 40 – 60 Meters | 150 – 250 Meters |
| Material Waste % | 18% – 22% | 3% – 5% |
| Operator Hours | 3 Operators | 1 Technician |
| Rejection Rate | Moderate (4%+) | Minimal (<1%) |
| Safety Risk | High (Manual blades) | Low (Enclosed PLC) |
The table illustrates that automation isn’t just about speed. It is about the drastic reduction in material waste. In an era where fabric costs represent nearly 60% of the total garment cost, a 15% reduction in waste directly impacts the gross margin.
A “Plug-and-Play” ROI Formula for CFOs
Calculating the return on investment doesn’t have to be a complex task. You can use this simplified formula to estimate your potential annual savings:
Total Annual Savings = [(Lh × Rh) + (W% × Fm)] – Am
- Lh: Reduction in manual labor hours per year.
- Rh: Hourly labor rate (including benefits).
- W%: Percentage of fabric saved through precision cutting.
- Fm: Total annual fabric spend.
- Am: Annual maintenance and power cost of the new machine.
For example, a factory spending $1M annually on fabric that reduces waste from 15% to 5% saves $100,000 on material alone. When you add the reduction in labor hours, the machine often pays for itself in just over a year.
Sustainability as a Financial Asset
The International Finance Corporation (IFC) highlights that resource efficiency is now a core requirement for textile financing and global trade compliance. Automated slitting supports this by ensuring “Right-First-Time” production.
Beyond the immediate cash flow, automated systems help factories align with the UN Sustainable Development Goals for responsible consumption and production. For a CFO, this means better access to “green” credit lines and more robust partnerships with global brands that prioritize audited, sustainable supply chains.
Featured Tech: The Svegea EC-300 Collarette System
The Svegea EC-300 serves as a benchmark for this financial transition. It is not just a cutter; it is a profit-recovery tool. Designed with an advanced PLC (Programmable Logic Controller), it allows for rapid changes in slitting widths with zero downtime.
What makes the EC-300 a strategic choice is its durability. High-quality Swedish engineering ensures that the machine maintains its precision over a decade of use, rather than degrading after a few years. This longevity is a key factor in calculating the long-term textile slitting machine ROI. It allows procurement officers to amortize the cost over a longer period, improving the balance sheet.
The Human Element: An Altruistic Transition
Investment in automation is often misinterpreted as a move to eliminate the workforce. However, leading manufacturers are using automation to solve the “Labor Gap.” Finding skilled manual cutters is increasingly difficult.
By implementing automated slitting, you provide your employees with a safer, tech-forward environment. This reduces turnover and training costs—another “soft” ROI factor that often goes uncounted. Workers transition from physically demanding roles to managing sophisticated PLC systems, which increases their own professional value within the industry.
Moving Forward with Data
The decision to upgrade your cutting room should be based on transparency and data. In the current market, the cost of doing nothing—and continuing with manual waste—is often higher than the lease payment on a new, automated system.
By analyzing your current waste percentages and labor hours, you can create a customized roadmap for your factory’s evolution. Automation is the bridge between the traditional craft of garment making and the high-efficiency requirements of the modern world.
Evaluate Your Cutting Room Today
Maximizing your ROI requires a blend of the right technology and strategic planning. If you are ready to move from manual estimates to automated precision, professional insight can help you bridge the gap.
For a detailed ROI analysis or technical specifications, please contact Håkan Steene at h.steene@svegea.se.