The short answer: The EU Digital Product Passport (DPP) is a digital record that will travel with each textile product sold in the European Union. The brand that sells the product owns the passport, but much of the data inside it comes from the factory: what the fabric is, where it came from and how it was checked. The EU switched on the DPP Registry in July 2026, and textile rules are expected toward the end of 2027. That leaves manufacturers a short window to get their data in order.
Key Takeaways
- The EU launched the Digital Product Passport Registry on 20 July 2026. Rules written specifically for textiles are expected toward the end of 2027.
- Brands register the passports, yet they will rely on their suppliers for the data.
- Fabric that is inspected, relaxed, and measured before cutting is far easier to document.
- Factories that build clean, digital records now will become the suppliers EU brands trust first.
Picture a plain white T-shirt on a shop shelf in Stockholm a few years from now. A shopper scans the small code on its label. In seconds, her phone shows what the shirt is made of, where it was produced and how long it should last. Behind that simple scan sits a long chain of facts, and many of those facts start on your cutting floor.
That scene is the promise of the EU Digital Product Passport. For garment and textile manufacturers, it is also a quiet change in what customers will expect from you.
What Is the EU Digital Product Passport?
The Digital Product Passport is a digital identity card for a product. It comes from the Ecodesign for Sustainable Products Regulation (ESPR), the EU law that aims to make products more durable, repairable and recyclable. Each passport holds key information about a product, and a central EU registry links that record to a unique product ID.
On 20 July 2026, the European Commission launched the DPP Registry along with a testing environment. Businesses can register passports through a simple web interface or connect their own systems through an API. Customs authorities will also be able to check electronically whether imported goods carry a valid, registered passport. Textiles sit among the priority groups, alongside furniture, tyres, steel and electronics.
When Will Textiles Need a Passport?
Not yet, but soon. The registry is live; however, it does not make every garment subject to a passport today. A separate textile act must first set the exact data fields, scope and timeline, and trade reports expect it toward the end of 2027.
That might sound far away. In practice, it is not. Brands plan their collections well ahead, and they will want supplier data in place before the first passport is due. As a result, your customers may start asking questions long before any legal deadline.
Why Should Garment and Textile Manufacturers Care?
Legally, the duty to create and register a passport falls on whoever places the product on the EU market, usually the brand or importer. Still, brands cannot invent the facts. They will turn to the mills, factories and cut-and-sew partners who actually handled the fabric.
Another rule adds weight to this shift. Since 19 July 2026, large companies in the EU can no longer destroy unsold clothing, footwear or accessories, and a standard reporting framework follows in February 2027. Together, these rules reward brands that know exactly what they made, how much they made and why. Suppliers who can answer those questions quickly will become preferred partners. Those who cannot will start to look like a risk.
The Cutting Room: Where Good Data Begins
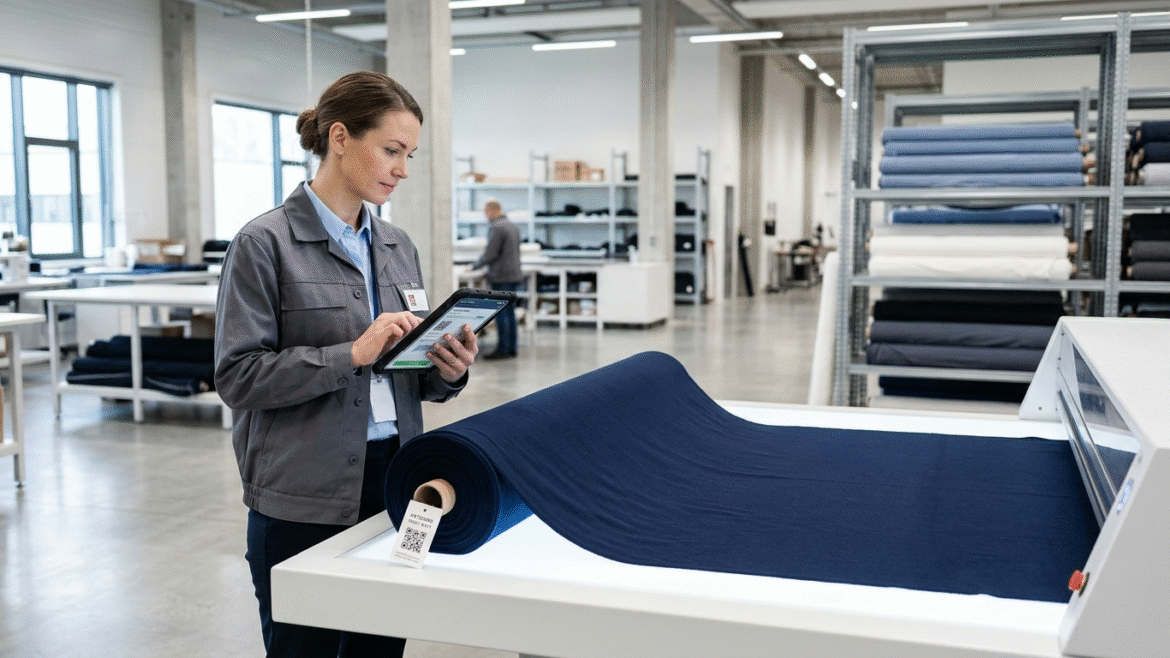
Every roll of fabric tells a story on its way to becoming a garment. It arrives, gets inspected, rests, gets measured and finally meets the blade. Each step creates useful facts, such as true length, real width, defects found and shrinkage after relaxing. Today, many of these facts live on paper or in a supervisor’s memory. Under the DPP, they become evidence.
Inspect before you cut
A recorded inspection gives every roll a history. Defects found at this stage stay out of finished garments, which means fewer rejects and less unsold stock. Just as important, the inspection log becomes proof of the care your team takes.
Measure what you actually received
Invoices state one width and length; the roll on your floor may tell a different story. Recording the real figures improves marker planning and gives brands accurate material data instead of estimates.
Relax first, then record
Knitted and stretch fabrics carry tension from knitting, dyeing and winding. Measure them too early, and the numbers drift once the fabric settles. Relaxing fabric before spreading gives you true measurements and garments that keep their size after washing. Svegea of Sweden’s CRX Air Relaxing Series, for example, measures fabric width automatically, controls length electronically and exports production data via USB, so the figures leave the machine already in digital form.
Five Steps to Get Passport-Ready Now
- Map your data. List what you already record for each roll and each order, and note where it lives.
- Give every roll an ID. Make sure that ID follows the fabric from receiving through inspection to cutting.
- Go digital at the source. Favour equipment that logs and exports data, so nobody has to retype numbers later.
- Talk to your EU customers. Ask what information they expect and in which format they want it.
- Watch for the textile act. Follow European Commission updates, since the final data fields will shape your records.
The Bottom Line
The Digital Product Passport is not just paperwork. It is proof. Factories that inspect, relax, measure and record fabric before the first cut will hand brands the data they need, and they will earn the trust that wins repeat orders. So when that shopper in Stockholm scans her white T-shirt, the story she reads could start in your cutting room.
Want to see how better fabric preparation fits your production line? Contact Svegea of Sweden or email Håkan Steene at h.steene@svegea.se to book a product demo.
Frequently Asked Questions
What is a Digital Product Passport for textiles?
It is a digital record linked to a garment or textile product through a unique ID, such as a QR code. Under the EU’s Ecodesign for Sustainable Products Regulation, it will store key product information to support transparency, repair, and recycling.
When will the Digital Product Passport become mandatory for textiles?
The EU Registry went live on 20 July 2026, but textiles still need their own delegated act. Trade reports expect it toward the end of 2027, and mandatory dates will follow from that act.
Who is responsible for the Digital Product Passport, the brand or the manufacturer?
The company that places the product on the EU market, usually the brand or importer, must create and register the passport. However, manufacturers supply much of the data, so brands will ask them for it.
How can garment factories prepare for the Digital Product Passport?
Start by recording roll-level data such as fabric type, true width, length and inspection results. Then assign each roll an ID, choose equipment that exports data digitally and agree on data formats with your EU customers.
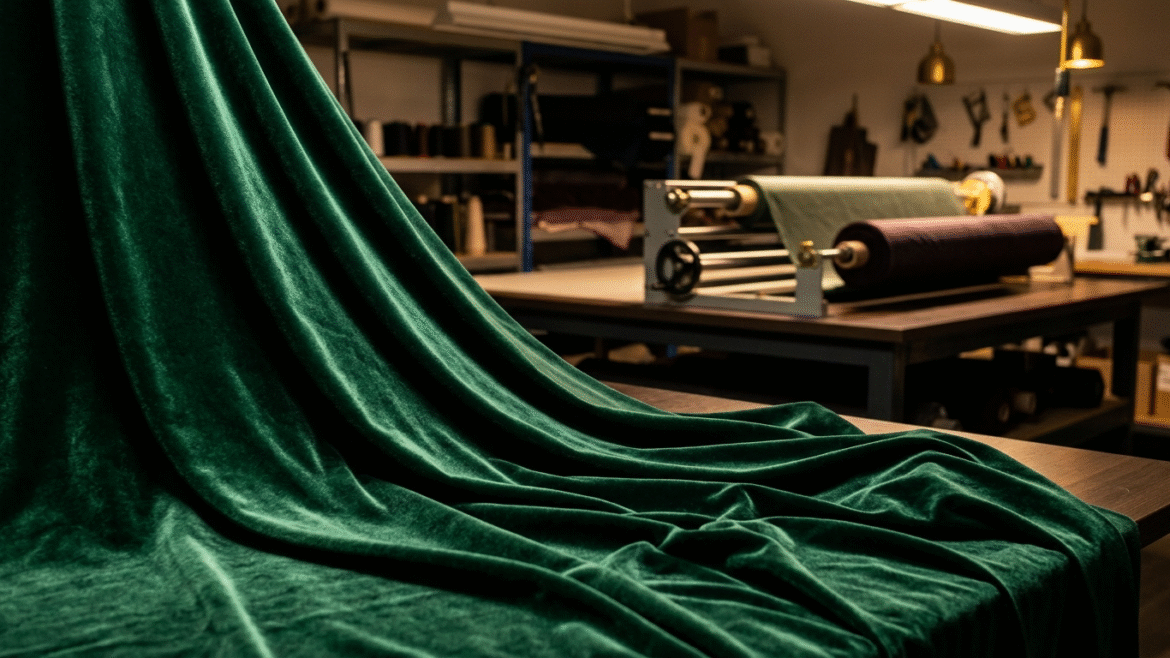
Walk into any store this December, and velvet will find you first. A plum party dress. An emerald blazer. Wide-leg trousers in deep chocolate brown. Velvet catches the light, feels like a small luxury, and makes even a simple outfit look ready for a celebration.
The runways saw it coming. Net-a-Porter’s fall/winter 2026 trend report named velvet the season’s key texture, with Alaïa, Khaite, and Ralph Lauren all showing tailored velvet looks. Meanwhile, Marie Claire spotted velvet trousers at Armani, Khaite, and Zimmermann.
For garment manufacturers, that popularity brings a real challenge. Velvet is gorgeous, but it is also one of the least forgiving fabrics on the factory floor.
So how do manufacturers handle velvet without crushing the pile? In short, they keep pressure, tension, and heat to a minimum at every stage. That means relaxing the fabric before cutting, inspecting every roll for flaws and shading, rewinding with little or no tension, and cutting every piece with the nap running the same way.
Key Takeaways
- Velvet leads the fall/winter 2026 and holiday collections, from party dresses to tailoring.
- Its pile flattens easily under pressure, heat, and moisture, and the damage can be permanent.
- The nap changes how velvet reflects light, so every piece must be cut in the same direction.
- Gentle relaxing, careful inspection, and tension-free rewinding protect velvet from roll to cut.
Why is velvet so difficult to manufacture?
Velvet gets its softness from a dense pile of tiny upright fibers. That pile gives velvet its glow. Unfortunately, it also makes the fabric fragile. According to Textile School, pressure, heat, and moisture can permanently flatten the pile. A tight roll, a heavy stack, or a careless press can leave marks that no amount of steaming will fix.
Then there’s the nap. The pile leans slightly in one direction, so the same fabric can look lighter or darker depending on how light hits it. Threads Magazine explains that velvet looks darker and absorbs light with the nap up, and looks lighter with the nap brushed down. Cut one sleeve the wrong way, and it can look as if it came from a different bolt.
Where does velvet get damaged in production?
Most problems start long before the sewing line. Here are the usual suspects:
- Tight winding. Rolls wound under heavy tension press the pile flat, especially near the core.
- Stored tension. Stretch velvet holds tension from knitting, dyeing, and winding, so cut panels can shrink later.
- Hidden flaws. Crush marks, bald spots, and shade differences are easy to miss until the garment is finished.
- Mixed nap. Pieces cut in different directions create visible color differences on the same garment.
Consequently, the best protection is a gentle, consistent process from the moment a roll arrives to the moment it reaches the cutting table.
How can factories protect velvet from roll to cut?
Relax it first. Stretch velvets need time to settle before spreading. Air-assisted relaxing machines, such as Svegea’s CRX Air, float the fabric on a cushion of air to release tension without pressing the surface.
Inspect every roll. A fabric inspection machine helps your team spot crush marks, shading, and pile defects before cutting begins, when they still cost the least to fix.
Rewind gently. When velvet needs rewinding, tension control matters. A tension-free rewinder like the W 2100S helps keep the pile upright from the outer layers right down to the core.
Cut with the nap. Mark the nap direction on the reverse side, and lay every pattern piece the same way. This layout uses more fabric, but it protects the finished look.
Finally, store rolls with care. Avoid stacking heavy rolls on top of velvet, and keep the storage area cool and dry.
Why does this matter for holiday orders?
Holiday collections run on tight deadlines. Brands want velvet dresses and blazers on the shelves by late November, and there is little time to remake rejected pieces. A crushed panel or a mismatched sleeve doesn’t just waste fabric. It can delay an entire delivery.
On the other hand, factories that handle velvet well become partners that brands trust. And when a buyer finds a supplier that delivers flawless velvet season after season, that buyer tends to come back.
Make This Velvet Season Your Best Yet
Velvet rewards patience and precision. Give it a gentle process, and it will give your customers that unmistakable glow. To find the right relaxing, inspection, or rewinding machine for your production, contact Svegea of Sweden or email Hakan Steene at h.steene@svegea.se to book a product demo.
Frequently Asked Questions
What is the nap of velvet?
The nap is the direction the pile leans. It changes how the fabric reflects light, so manufacturers cut all pieces of a garment in the same direction.
Can crushed velvet pile be restored?
Light marks may lift with gentle steam from the wrong side. However, heavy or long-term pressure can flatten the pile permanently.
Why does stretch velvet shrink after cutting?
It holds tension from knitting, dyeing, and winding. Relaxing the fabric before cutting lets it return to its natural dimensions.
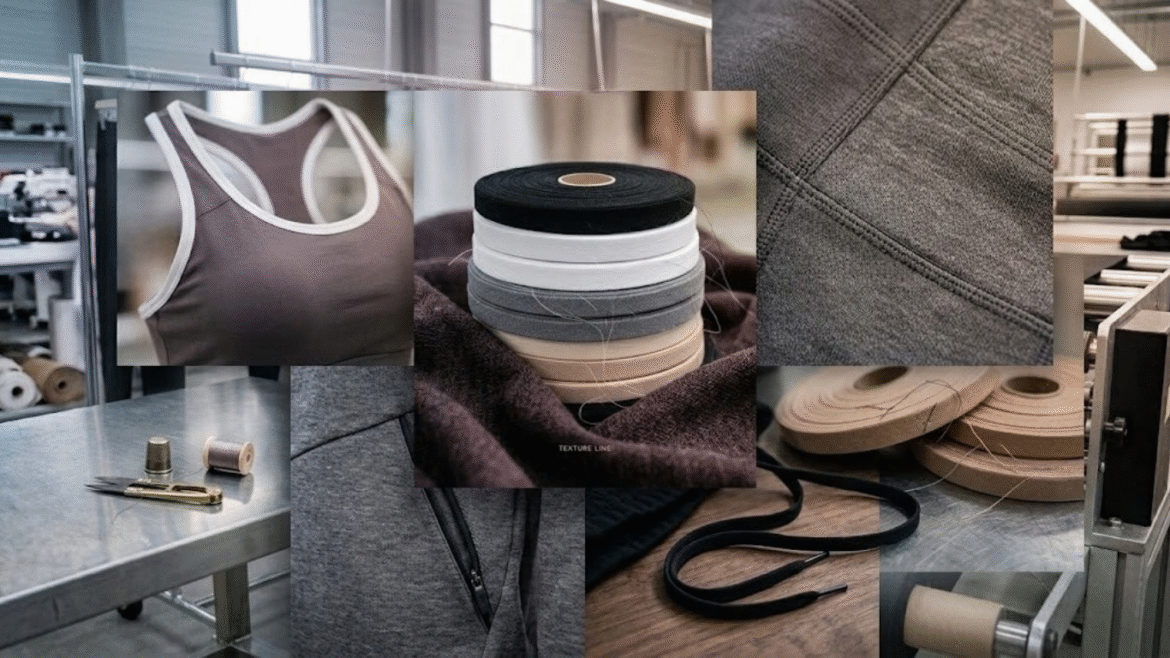
Look closely at any modern garment, and you will find strips everywhere. A soft waistband on joggers. Binding along a sports bra. Piping on a jacket pocket. Clean edging on a pair of leggings. These narrow components rarely get attention, yet they decide how a garment fits, feels, and lasts.
For 2027, that small detail is becoming a big production question. Brands want more stretch, more comfort, and more variety, and they want it faster. As a result, the strip cutting machine has moved from a back-room tool to a key part of the cutting floor.
So what is changing in strip cutting for 2027? In short, manufacturers now need to cut more trim widths, in shorter runs, from a wider mix of stretch and technical materials. Strip cutting technology is adapting with stored cut programs, servo-driven precision, automatic blade care, and enclosed cutting for operator safety. Factories that match the right machine to their volume can switch styles faster and waste less fabric.
Key Takeaways
- Demand for elastic and narrow trims keeps rising, driven by activewear, intimates, and medical textiles.
- Factories face more trim widths, more materials, and shorter production runs.
- Modern strip cutters answer with preset cut programs, ±0.01 mm accuracy, and automatic blade sharpening.
- The right machine depends on roll size, volume, and how often you change widths.
Why is elastic and trim demand shifting in 2027?
Comfort has become a buying habit, not a trend. Shoppers now expect stretch in almost everything, from office trousers to school uniforms. That expectation pulls elastic waistbands, stretch binding, and flexible edging into far more product lines than before.
The numbers support this. According to Research and Markets, the global elastic narrow fabric market is projected to grow from about USD 912 million in 2026 to USD 1.21 billion by 2032, a compound annual growth rate of 4.8%. The report links that growth to sportswear, medical products, automotive uses, and specialized industrial applications.
Several forces stand behind this shift:
- Activewear and athleisure keep growing. Leggings, sports bras, and joggers all rely on soft, even trims that move with the body.
- Intimates and shapewear demand precision. Narrow bindings and edgings must sit flat against the skin, with no rough or wavy edges.
- Medical and compression textiles are expanding. These products need consistent widths for both comfort and function.
- Brands order more styles in smaller batches. Each new style can bring a new trim width, colour, or material.
Moreover, sustainability pressure has changed how buyers view waste. Every off-width strip is fabric the factory paid for and cannot sell. Consequently, cutting accuracy now affects margins and environmental targets at the same time.
What’s the difference between the FA350, FA500 and CMS series?
Svegea of Sweden builds several strip cutters, each suited to a different production profile. The table below compares four models using the specifications listed on svegea.se.
| Model | Automation | Max. width | Max. roll diameter | Cut presets | Best for |
|---|---|---|---|---|---|
| FA 350 | Fully automatic, PLC controlled | 2000 mm | 300 mm | Up to 3 cut widths, 3 programs | Precision trims across mixed materials |
| FA 500 | Heavy-duty fully automatic, PLC servo (X & Y) | 2000 mm | 400 mm | Up to 6 cut widths with recipe storage | High-capacity runs on large rolls |
| CMS 1800 A3/A4 | Fully automatic blade forwarding and carriage | Wide-format rolls | On request | Multi-preset touchscreen with memory | Continuous, high-volume slitting with little operator input |
| CMS 1850A | Automatic, step-motor controlled | 1630 mm | 250 mm | Up to 5 preset widths | Small to mid-sized cutting rooms on a budget |
Specifications from svegea.se. Contact Svegea for full CMS 1800 A3/A4 dimensions.
The FA 350 handles a wide range of materials, from open knits and wovens to PVC, vinyl, satin, and non-wovens. It cuts with ±0.01 mm accuracy, sharpens its own blade, and stays fully enclosed during each cut cycle.
The FA 500 takes the same idea further. Its larger 500 mm blade and 400 mm roll capacity suit factories that run long jobs on big rolls. PLC servo positioning and recipe storage let operators recall up to six cut widths for repeat orders, saving setup time on recurring jobs.
The CMS 1800 A3/A4 focuses on continuous output. Automatic blade forwarding and carriage positioning reduce manual work, while dual electronic speed control lets operators match blade and roll speeds to each material. A full safety hood covers the cutting area.
The CMS 1850A offers an economical entry into automatic strip cutting. It stores up to five preset widths and electronically adjusts blade and roll speeds, making changeovers simple for growing factories.
How do you choose the right strip cutting machine?
Start with your rolls, not the brochure. Roll diameter and width set the first limit. If your suppliers deliver large rolls of stretch fabric, a machine with a 400 mm roll capacity will reduce reloading and downtime.
Next, look at how often you change widths. A factory that cuts the same binding all week needs speed above everything else. In contrast, a factory that switches between six trim widths a day needs fast recall of stored presets.
Then consider your materials. Elastic and stretch fabrics shift under the blade, so precise speed control and a sharp, cool blade matter. Automatic sharpening keeps edges clean through long shifts, and an optional blade cooling system helps with heat-sensitive synthetics.
Finally, think about your people. Enclosed cutting cycles protect operators, and touchscreen controls shorten training for new or seasonal staff. Together, these features help a factory keep quality steady even when the team changes.
Get Ready for 2027 Demand
Elastic and trim demand will not slow down in 2027. Brands will keep asking for more comfort, more variety, and less waste, often on tighter deadlines. The factories that win those orders will be the ones that can cut any width, from any roll, with the same precision every time.
Ready to find the strip cutter that fits your production line? Explore Svegea’s roll slitting machines, contact Svegea of Sweden, or email Hakan Steene at h.steene@svegea.se to book a product demo.
Frequently Asked Questions
What is a strip cutting machine?
A strip cutting machine, also called a roll slitter, cuts a full roll of fabric into narrow strips of equal width while the roll turns. Factories use these strips for binding, piping, elastic trims, and other narrow components.
How is strip cutting changing for 2027?
Manufacturers want more trim widths, shorter runs, and less waste. As a result, strip cutters now focus on stored cut presets, servo precision, automatic blade care, and safer enclosed cutting.
What is the difference between the FA350 and FA500?
Both are fully automatic and cut rolls up to 2000 mm wide with ±0.01 mm accuracy. The FA500 is the heavy-duty model, with a 400 mm roll capacity, a larger 500 mm blade, PLC servo positioning, and up to six preset cut widths. The FA350 takes rolls up to 300 mm and stores up to three presets.
Which strip cutter suits a small or mid-sized factory?
The CMS1850A suits smaller cutting rooms. It is economically priced, works with rolls up to 1630 mm wide and 250 mm in diameter, and stores up to five preset cut widths.
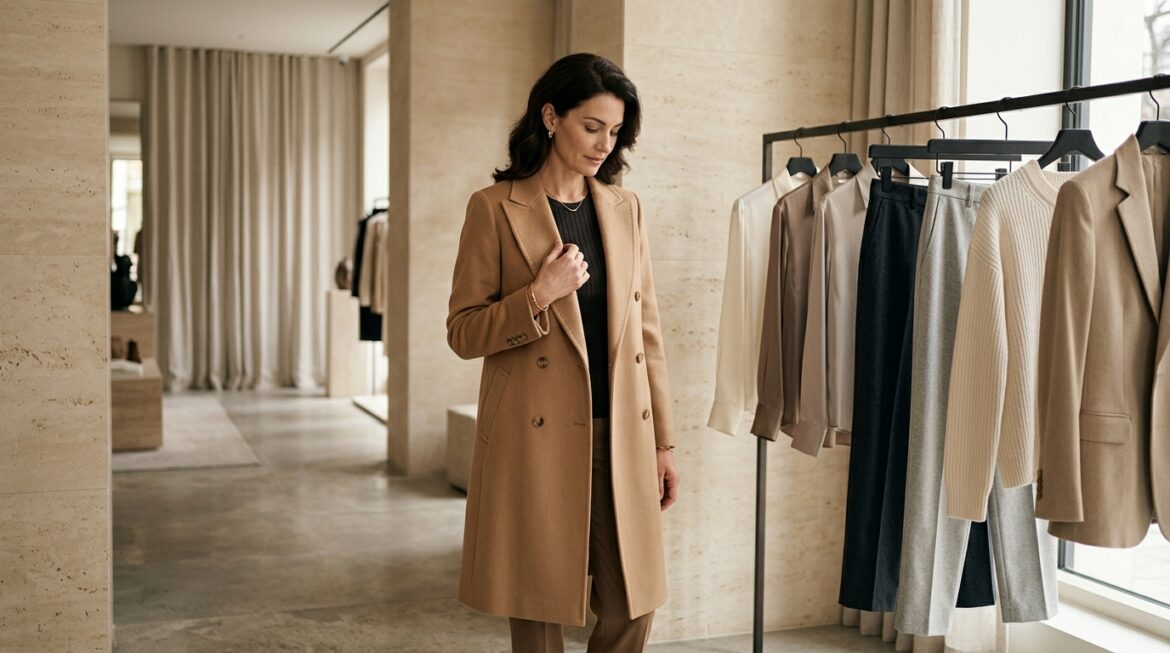
A camel coat with no logo. An ivory silk shirt with no visible branding. A plain wool trouser that costs more than a month’s rent. This is quiet luxury, and it has changed what shoppers notice.
When a garment has no logo to speak for it, the fabric does all the talking. Shoppers run their hands over the cloth, hold it up to the light, and study the seams. A small slub, a faint shade band, or a pulled thread has nowhere to hide. For garment manufacturers, quality control can no longer start at the sewing line. It has to start with a fabric inspection machine, long before the first cut.
So how do garment manufacturers inspect fabric for defects? In short, operators run each roll across a lit inspection table, check it for flaws as it moves, mark every defect, and measure the roll’s true length. Most factories then grade each roll with a point system and decide whether to use it, return it, or cut around its flaws.
Key Takeaways
- Quiet-luxury garments rely on flawless fabric because there are no logos or prints to hide defects.
- Fabric inspection catches flaws before cutting, when they cost the least to fix.
- Much of the industry grades fabric with the four-point system in ASTM D5430.
- The right inspection machine depends on fabric width, speed, and where rolls go next.
Why Quiet Luxury Raises the Bar
Loud fashion has its uses. Bold prints, heavy embellishment, and large logos pull the eye away from the cloth underneath. Quiet luxury does the opposite. It strips a garment back to cut, colour, and material.
That shift puts pressure on every stage of production. A neutral coat or a pale knit shows every irregularity. Moreover, buyers of these pieces expect them to last for years, so they examine them closely before they pay. One visible flaw can turn a premium price into a return, a markdown, or a lost wholesale account.
For suppliers, the message is simple. If the brand promises perfection, the fabric must deliver it first.
The Cost of Finding Flaws Too Late
A defect costs the least while it is still on the roll. Once the fabric is spread and cut into panels, the same flaw can spoil several pieces at once. If it slips past sewing, the factory pays for labour, thread, and finishing on a garment that may never sell.
Late detection also hurts relationships. Many luxury buyers run their own checks when goods arrive. When they find defects, they may reject a whole shipment, not just the faulty pieces. As a result, a few missed flaws can delay an entire order and damage trust that took years to build.
Inspection before cutting turns unknown risks into known facts. The factory knows exactly what it has, where the flaws sit, and how much usable fabric remains.
How Garment Manufacturers Inspect Fabric for Defects
Most factories follow a similar routine:
- Load the roll onto a fabric inspection machine.
- Run the fabric over a lit inspection table at a steady, controlled speed.
- Check the full width for holes, stains, slubs, shade variation, and knitting or weaving faults.
- Mark each defect at the selvedge so cutters can avoid it.
- Record the true length and width of the roll.
- Grade the roll with an agreed point system.
The most widely used grading method is the four-point system, set out in ASTM D5430, the standard test methods for visually inspecting and grading fabrics. Inspectors give each defect one to four penalty points based on its size, then work out the total points per 100 square yards. Buyers and suppliers agree in advance how many points a roll may carry before it counts as second quality.
What Good Fabric Defect Detection Looks Like
Good fabric defect detection depends on three things: light, speed, and control.
First, the inspection area needs bright, even light, so faint shade bands and fine slubs stand out. Second, speed must suit the fabric. A plain cotton can move faster, while a fine silk or fine-gauge knit needs a slower pass. Finally, the fabric should move smoothly, without stretching or drifting to one side. Uneven tension can distort knits and hide flaws, and a wandering edge slows the operator down.
Accurate measuring matters too. Rolls do not always match the length on their labels. A reliable meter or yard counter shows what the factory really received, which protects both costing and supplier claims.
Choosing the Right Inspection Setup
Not every factory needs the same machine. Fabric width, daily volume, and the way rolls move to the next stage all shape the choice.
For standard widths, a compact roll-to-roll machine often covers daily needs. Svegea of Sweden’s CMI 180 and CMI 180E, for example, handle fabric up to 1800 mm wide at speeds of up to 45 m/min. For wider goods, the CMI 210 R and CMI 210 ZR take fabric up to 2100 mm and add photocell edge alignment, electronic tension adjustment, and an electronic meter counter. The CMI 210 ZR can also deliver fabric roll to roll or roll to flat, which helps when inspected fabric goes straight to spreading.
Whatever the model, the goal stays the same: know your fabric before you cut it. You can compare the full range on the fabric inspection machines page.
Quick Tips for Flawless Fabric
- Inspect every roll, not just samples. Premium buyers expect the same quality across the whole order.
- Slow down for delicate fabrics. Fine silks, wools, and knits reveal more flaws at lower speeds.
- Check shade from roll to roll. Compare a strip from each roll to catch colour differences between batches.
- Mark defects clearly. Use stickers or tags at the selvedge so cutters spot them at once.
- Relax knits first. Tension can stretch knitted fabric and hide its true width, so a fabric relaxing machine is a useful step before inspection.
Frequently Asked Questions
How do garment manufacturers inspect fabric for defects?
They run each roll through a fabric inspection machine, check it under bright light as it moves, mark every defect, measure the roll, and grade it, usually with the four-point system.
What is the four-point system in fabric inspection?
It is a grading method described in ASTM D5430. Inspectors give each defect one to four penalty points based on its size, then compare the total per 100 square yards with an agreed limit.
What defects does fabric inspection detect?
Common examples include holes, stains, slubs, broken yarns, shade variation, and differences in width or length.
Why is fabric inspection important for luxury brands?
Quiet-luxury garments rely on plain, premium fabric. With no logos or prints to distract the eye, even small flaws are visible, so inspection protects both the garment and the brand’s reputation.
Ready to Inspect Smarter?
Luxury starts long before a garment reaches the shop floor. It starts with the roll. To find the right fabric inspection machine for your production, contact Svegea of Sweden or email Hakan Steene at h.steene@svegea.se to book a product demo.
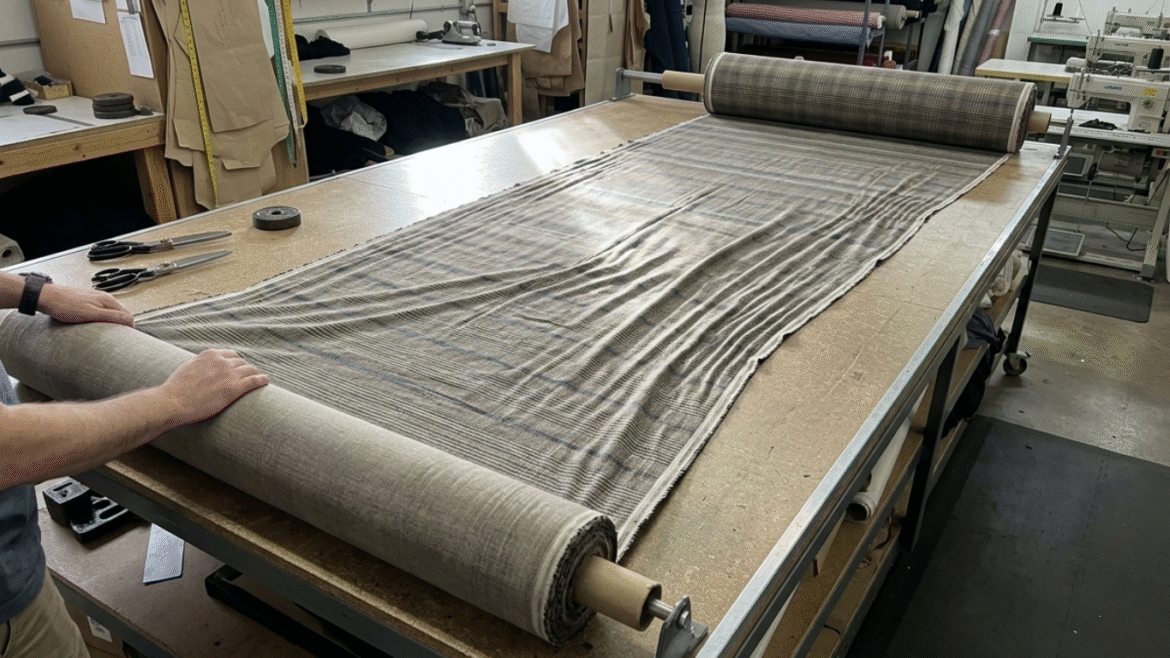
Sustainable Fabric Cutting Technology
Fabric relaxing is a pre-cutting step that lets rolled fabric rest under controlled, tension-free conditions before it reaches the cutting table. A fabric relaxing machine unwinds the roll, releases the internal stress built up during knitting, dyeing, or transport, and lets the material settle into its true dimensions. This one step cuts pattern distortion, lowers reject rates, and reduces textile waste in manufacturing. Heading into 2027, it’s one of the more practical sustainability upgrades a cutting room can make.
What causes fabric waste in cutting rooms?
Knitting, dyeing, and transport all put significant tension on rolled fabric. Winding a roll tightly, dyeing it under heat, or shipping it across the country all pull and stretch the material in ways the eye can’t see. The fabric holds this tension until something releases it. If nothing does, the release happens on the cutting table — or worse, after workers sew the garment.
Here’s the practical problem this creates. A cutter lays fabric flat and cuts it to a pattern while the material is still under tension. Once it’s off the table, the fabric relaxes and pulls back toward its natural shape. Panels that looked perfect during cutting shrink, skew, or twist. Seams no longer align. The finished garment may pucker, sag, or fit incorrectly after its first wash, and none of this shows up until it’s expensive to fix.
Knit fabrics and stretch wovens with spandex or Lycra content are especially prone to this problem, because their fibers hold tension longer than rigid wovens do. Circular knits add another layer of risk: cutting teams slit the tube open and spread it flat before cutting, and that extra handling step introduces skew on top of existing distortion.
The financial impact is larger than most cutting rooms assume. Fabric waste in cutting rooms typically runs 10% to 20% of total material, according to Lectra, and fabric alone often accounts for more than half of a garment’s total cost. Even a small improvement in fabric utilization translates directly into lower material spend and less waste headed to landfill or recycling.
How does fabric relaxing reduce waste?
A fabric relaxing machine addresses the problem at its source, before the fabric ever reaches the marker table. Instead of cutting a stressed, distorted roll and hoping for the best, the fabric first travels through a relaxing unit that unwinds it slowly, removes tension through mechanical rollers or controlled airflow, and lets the fibers settle back into their natural, balanced state.
Once the fabric relaxes, its true dimensions return, and cutters can follow the fabric’s actual grain instead of a stretched, temporary one. That single change has a ripple effect across the whole production line:
- Fewer distorted panels means fewer rejected pieces and less scrap fabric.
- Consistent dimensions mean tighter marker efficiency, so planners can nest patterns closer together without leaving a safety margin for shrinkage.
- Fewer post-wash surprises mean fewer returns and less rework, which saves fabric that would otherwise go into a second cut.
- Stable, tension-free feeding protects delicate or elastic fabrics from stretching, snagging, or fraying at the edges.
In short, fabric waste drops when cutting rooms remove tension before the fabric reaches the marker table, and manufacturers get more usable garment pieces out of every roll they buy. Operators feed a well-relaxed roll into the spreader without added stress, so what a planner sees on the marker is what the sewing line actually gets.
Which fabric relaxing machine fits my production volume?
Svegea builds fabric relaxing machines for a range of production volumes and fabric types, from standard knit-and-woven operations to high-speed, air-assisted lines handling delicate stretch textiles. The table below compares the current lineup so you can match a machine to your cutting room’s needs.
| Model | Best for | Relaxing method | Key feature | Learn more |
| CR210 | Standard-volume cutting rooms | Stepless electronic speed control with an oscillating fold system | Photocell loop control for smooth, tensionless feeding | svegea.se/product/cr210-fabric-relaxing-machine/ |
| CR210A | Higher-precision cutting rooms needing tighter edge control | Same tensionless feeding as the CR210, plus automatic edge alignment | Integrated automatic edge alignment device | svegea.se/product/cr210a-fabric-relaxing-machines/ |
| CRX Air Relaxing Series | High-speed lines and delicate stretch fabrics (jersey, lycra, technical textiles) | Dual independent air-flotation zones instead of mechanical rollers | PLC control, automatic width measurement, speeds up to 40 m/min | svegea.se/product/fabric-relaxing-machine-crx-air/ |
The CR210 suits standard-volume cutting rooms that need dependable, tensionless feeding without a large equipment footprint. The CR210A builds on that same platform and adds an automatic edge alignment device for manufacturers who need tighter tolerance control on wide or high-value fabric runs. The CRX Air Relaxing Series runs on controlled airflow instead of mechanical rollers, which makes it the better fit for lightweight knits, lycra blends, and other fabrics that stretch or curl easily under physical contact.
A quick note on model selection: Svegea’s current fabric relaxing lineup covers these three machines. If you were comparing a “CR205” model, double-check the spec sheet or brochure you’re working from — it doesn’t currently appear as an active model on svegea.se, and the closest equivalent for lighter, standard-volume applications is the CR210.
Sustainability impact
The stakes go beyond one cutting room. The fashion industry loses the equivalent of one garbage truck of textiles to landfill or incineration every second worldwide, and recyclers turn less than 1% of clothing back into new garments, according to the Ellen MacArthur Foundation. Preventing waste at the cutting stage keeps material out of that stream entirely.
Regulation is starting to reflect this. In Europe, manufacturers and retailers destroy an estimated 4% to 9% of the textile products they place on the market before anyone ever uses them, according to the European Environment Agency. That data helped shape the EU’s Ecodesign for Sustainable Products Regulation (ESPR), which bans large companies from destroying unsold textiles starting in July 2026. Manufacturers who cut waste upstream, at the cutting table, stand in a stronger position for this kind of policy shift than those relying on downstream fixes.
Fabric relaxing also supports a “cut it once” mindset. When pattern pieces hold their shape after cutting, fewer garments need rework, fewer rolls need re-ordering to cover shrinkage losses, and manufacturers waste less packaging, transport, and processing on fabric that never becomes a finished product. For a fashion industry under growing pressure to show measurable sustainability progress by 2027, this kind of upstream fix is one of the more cost-effective places to start.
Not inevitable
Cutting-room waste isn’t inevitable — it’s largely a tension problem, and tension is solvable before the fabric ever meets the blade. A fabric relaxing machine gives manufacturers a practical, proven way to stabilize material, protect pattern accuracy, and reduce textile waste in manufacturing without slowing down production.
To see the full fabric relaxing lineup, product brochures, and specifications, visit our Fabric Relaxing Series page. For more on fabric shrinkage and pre-cutting prep, read svegea.se/prevent-fabric-shrinkage/. Contact us for a product demo!
FAQ
What is fabric relaxing in textile manufacturing?
Fabric relaxing is a pre-cutting process that removes internal tension from rolled fabric so it can settle into its natural, stable dimensions before spreading and cutting.
Why does fabric shrink after cutting if it was measured correctly?
Most likely, the fabric went through cutting while still under tension from knitting, dyeing, or transport. Once it’s off the cutting table, that tension releases, and the material shrinks or shifts out of shape.
How much fabric waste can a relaxing machine actually prevent?
Results vary by fabric type and production setup, but since cutting-room waste typically runs 10% to 20% of total material (www.lectra.com), even a modest reduction in distortion-related waste can meaningfully lower material costs.
Do all fabric types need relaxing before cutting?
Knit fabrics and stretch wovens with spandex or Lycra content benefit the most, since their fibers hold tension longer. Rigid wovens still benefit, but usually need shorter relaxing cycles.
What’s the difference between fabric relaxing and pre-shrinking?
Pre-shrinking uses washing or steaming to shrink fabric before cutting, which works but takes time and adds cost. Relaxing lets the fabric settle naturally, without added moisture or heat, which is faster and gentler on delicate materials.
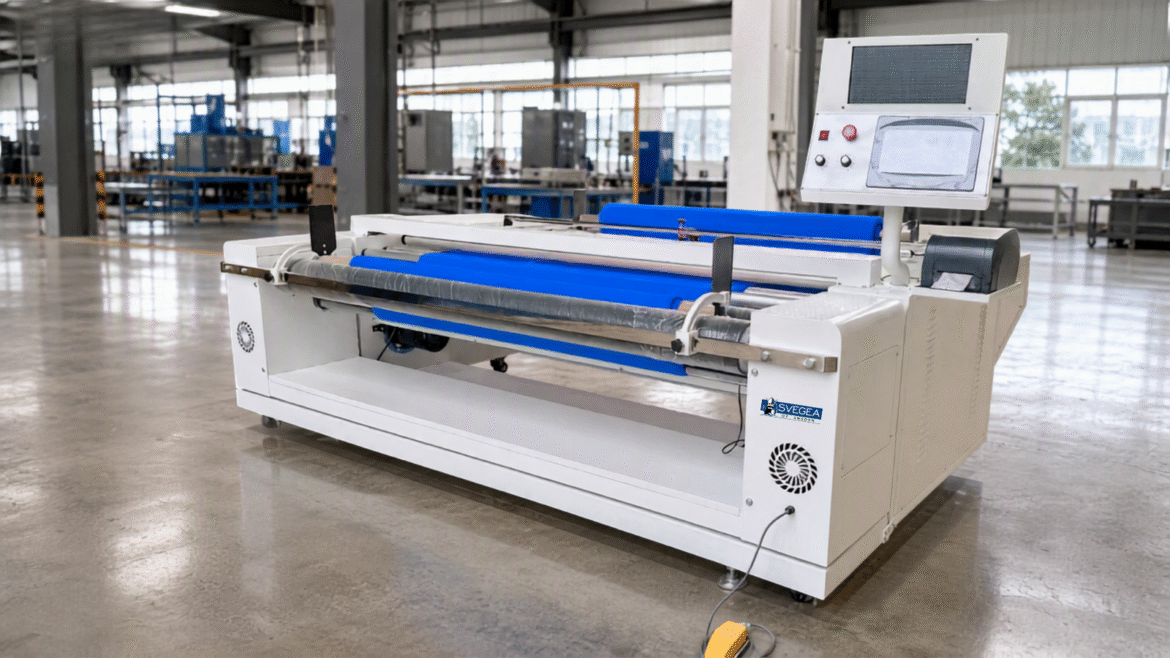
Garment factories are changing faster than most buyers realize. Machines now handle jobs that used to take several pairs of hands, and cutting rooms are quietly becoming the most technical part of the whole production line. For manufacturers planning capacity for 2027, that shift is worth understanding now.
The top textile manufacturing trends for 2027 are automation in trim and collarette production, gentler air-based fabric relaxing, waste reduction built into the cutting process, and modular machines that adapt to more than one job. Together, these trends point toward factories that produce more, waste less, and rely less on manual labor to stay consistent.
What Is Driving Automation in Textile Trims?
Labor costs are rising, and buyers expect tighter quality control than ever before. Because of this, semi-automatic trim machines are becoming standard rather than a premium upgrade. A machine like the EC50 Semi-Automaticlets one operator load fabric and start a cutting cycle that runs on its own, cutting labor time without cutting corners on precision.
The payoff shows up in the numbers. According to a 2026 garment manufacturing market report, automation in stitching and cutting has already improved productivity by 18% and reduced waste by 11% industry-wide. That kind of gain is hard to ignore for factories competing on both speed and cost.
High-precision collarette machines are following the same path. The EC300 Euro Collarette is built to hold consistent trim width across long runs, which matters more as brands demand uniform quality across bigger batches.
How Is Fabric Relaxing Getting Gentler?
Fabric that’s cut under tension often shrinks or distorts later, and that problem has quietly cost manufacturers money for years. In 2027, expect more factories to add a relaxing step before cutting, and to do it with less mechanical stress on the fabric.
Air-based relaxing is leading that change. The CRX Air Relaxing Series uses contact-free air technology instead of rollers, which reduces distortion in delicate knits. It’s a small step in the process, but it prevents costly rework further down the line.
Why Is Waste Reduction Now a Core Trend, Not an Afterthought?
Sustainability pressure isn’t new, but it’s becoming more concrete. Fabric waste is being treated as a production cost to eliminate, not just an environmental talking point. Systems that combine cutting, folding, and winding in one pass – like the Complete Bias System – cut down on offcuts and reduce the handling steps where fabric typically gets damaged or wasted.
This trend also connects back to relaxing and trim precision. A cleanly relaxed, evenly cut fabric produces fewer rejected panels, and fewer rejected panels means less fabric bought and discarded in the first place.
Why Are Modular, Accessory-Based Machines Gaining Ground?
Manufacturers no longer want a machine that does one job well. They want equipment that adapts as orders change. Accessory kits, like the ones now available for the EC200C, let a single collarette machine produce multiple trim widths and styles without buying separate equipment for each style.
This flexibility matters most for mid-size manufacturers, who need to serve varied customer demands without the capital cost of a large, specialized machine fleet.
What This Means for Your Production Line
None of these trends work in isolation. Automation improves speed, gentler relaxing protects fabric quality, waste reduction protects margins, and modular machines protect flexibility. Manufacturers who treat these as one connected strategy – rather than four separate purchases – will be better positioned heading into 2027.
If you’re mapping out equipment upgrades for the year ahead, contact the Svegea team to talk through which machines fit your production line.
FAQ
- What is the biggest textile manufacturing trend for 2027?
Automation in trim and cutting is the trend with the broadest impact, since it affects speed, labor cost, and consistency at once. - Does automation reduce fabric waste?
Yes. Automated, precision-cut trims and relaxed fabric both reduce the number of rejected panels, which lowers overall fabric waste. - What is fabric relaxing and why does it matter?
Fabric relaxing removes tension from a fabric roll before cutting. It’s important because fabric cut under tension tends to shrink or shift shape after cutting, causing quality issues later. - Are modular machines worth it for smaller manufacturers?
Often, yes. A modular machine with accessory kits can replace several single-purpose machines, which lowers equipment costs for manufacturers producing varied trim styles. - How can I prepare my factory for these 2027 trends?
Start by identifying where manual handling causes the most waste or inconsistency – usually trim cutting or fabric relaxing – and evaluate equipment built for that specific step.
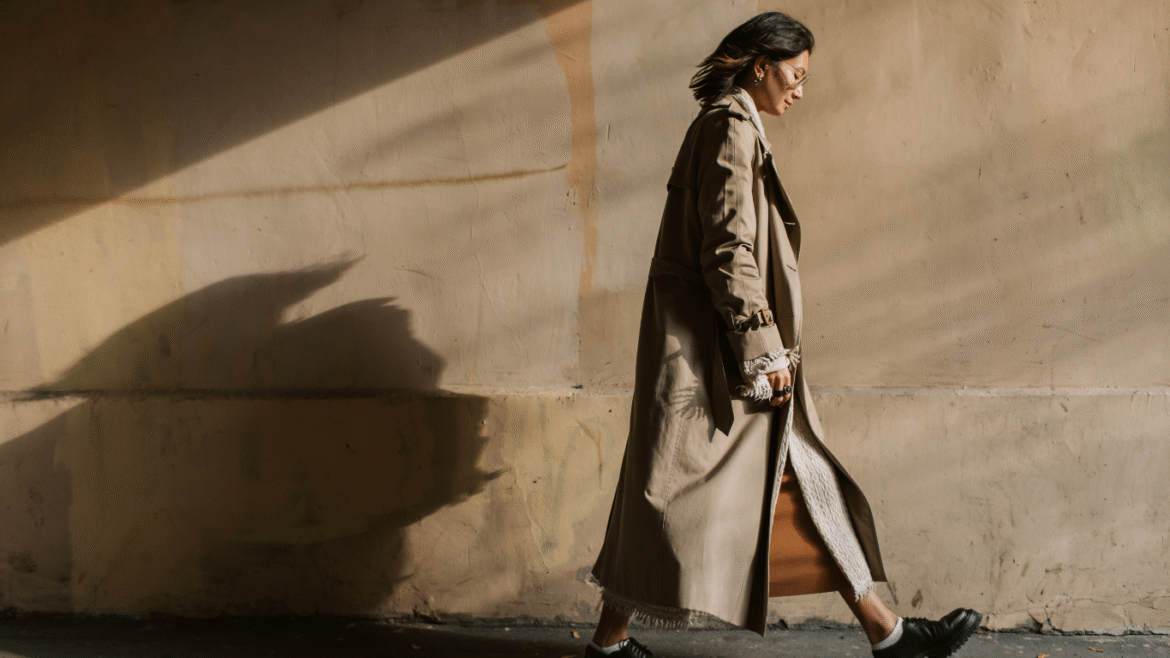
Autumn is creeping back in, and with it, the trench coat is coming out of storage again. Scroll through any fashion feed right now and you’ll see it: belted, oversized, thrown over a slip dress or buttoned up over a suit. It never really goes away, but every September it seems to reintroduce itself as the season’s must-have layer.
We’ve watched this coat cycle through fashion for years from our side of the industry — the manufacturing side. And here’s the thing most style articles won’t tell you: the reason a good trench coat still looks sharp after a decade of wear has almost nothing to do with the belt or the buttons everyone photographs. It’s buried inside the collar, the lapel, and the lining, in a set of narrow fabric strips most wearers never think about.
A Coat Built Like a Small Structure
Thomas Burberry patented gabardine back in 1879, engineering it specifically to be waterproof without the stiffness of rubberized rainwear. That original goal — weather resistance without bulk — is still what separates a real trench coat from a coat-shaped raincoat. But weatherproof fabric alone doesn’t explain why a well-made trench holds its collar stand or keeps its lapels from curling after years of use.
That comes down to internal reinforcement: collar stays, lapel interlining, and the strapping used for belts and epaulettes. Unlike a lightweight dress or blouse, a trench coat carries real structural weight. Heavy gabardine, dense twill, sometimes multiple bonded layers — none of it behaves the way thin fabric does under a sewing machine, and none of it forgives sloppy internal construction.
So while the outer fabric gets all the design credit, it’s these hidden strips of interlining and tape that decide whether the coat ages gracefully or starts sagging at the shoulders by its second winter.
What Those Hidden Strips Actually Do
A few things happen when a manufacturer gets this part right:
- The collar stands up crisply instead of collapsing, even on a heavy double-layered lapel.
- Belt loops and cuff straps stay straight and don’t twist over time.
- The fabric doesn’t fray internally where it’s under the most tension — shoulders, waist, collar edge.
- The coat keeps its shape wash after wash, season after season.
None of this shows up in a product photo. You notice it later, the first time you flip your collar up against a cold wind and it actually stays put.
Where Hand-Cutting Runs Out of Road
A skilled tailor working on a single bespoke coat can cut collar stays and waist strapping by hand, with shears and a steady eye. It works, at that scale.
It doesn’t work at factory scale. Once a manufacturer is producing thousands of coats a season, hand-slitting heavy rolls introduces the kind of inconsistency that ruins a production run: frayed edges from blade friction, strips that come out a millimeter or two off-width, automated sewing lines thrown out of alignment because the input material isn’t uniform. Multiply a small error by ten thousand units and it stops being small.
This is the point where most outerwear manufacturers move to dedicated slitting equipment. And it’s the part of the process we spend most of our time thinking about.
Where We Come In
At Svegea, we build roll slitting and band cutting machines designed around exactly this problem: cutting dense, heavy fabric into narrow, consistent strips without the fraying, stretching, or width drift that ruins a production batch.
A few things our machines are built to handle:
1. Consistent width across the whole roll. The strip you cut at meter one should match the strip at meter one thousand.
2. Clean edges on dense material. Automatic blade sharpening keeps friction and heat from fraying heavier fabrics like gabardine or bonded interlining.
3. Tension control that doesn’t distort the weave. Heavy woven fabric under the wrong tension stretches unevenly, and that shows up later as puckering.
We didn’t design this equipment with trench coats specifically in mind — it’s used across tailored blazers, technical rainwear, and industrial textiles too — but outerwear is where the margin for error is smallest. Dark, structured coats show every flaw in daylight.
The Part Nobody Photographs
There’s a reason this kind of detail rarely makes it into a fashion write-up. It’s not glamorous. Nobody’s Instagramming a roll of interlining tape. But it’s the difference between a coat that’s still in rotation a decade from now and one that’s in a donation bag by next spring.
If you’re on the manufacturing side and dealing with fraying, width inconsistency, or waste on heavy-fabric roll slitting, it’s worth a conversation — we’ve spent a long time solving exactly this problem. You can reach our engineering team through svegea.se, or explore the equipment lineup on the same site.
Either way, next time you flip up a trench coat collar against the wind, you’ll know what’s actually holding it there.
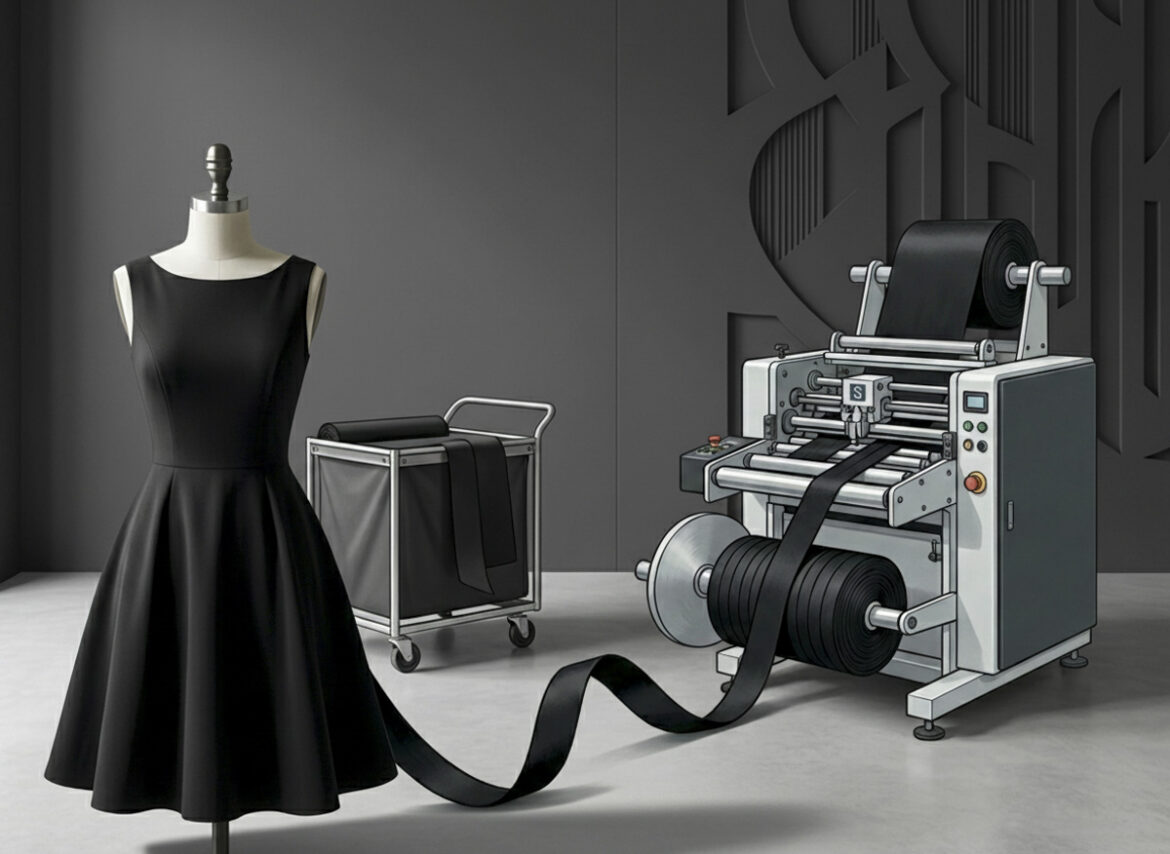
Little did Givenchy know that the little black dress he designed for Audrey Hepburn would become an essential piece in nearly every woman’s wardrobe, generations after Breakfast at Tiffany’s first hit the screen.
The Little Black Dress, or LBD, has since become fashion’s great equalizer — a single garment that flatters every shape, suits every occasion, and never goes out of style. It gets you through a chaotic morning, an unplanned dinner date, or a job interview with equal ease. Match it with a denim jacket and flats for class, add a statement necklace for a night out, or pair it with a tailored blazer to walk into an interview with confidence. Few garments do so much with so little.
But here’s what almost no one talks about when they praise the LBD’s timeless silhouette: why does a well-made black dress hold its shape, drape cleanly around the neckline, and outlast a decade of wear — while a cheaper version puckers, frays, and loses its form after a few washes?
The answer isn’t the fabric. It isn’t even the cut. It’s what happens at the edges.
The Finishing Technique You Never Notice — Until It’s Missing
Every curved seam, every clean neckline, every armhole that sits flat against the skin instead of gapping or rolling — all of it depends on a technique called bias binding.
Bias binding is a strip of fabric cut on the diagonal, or “bias,” of the material rather than along the straight grain. Cutting fabric this way gives the strip natural stretch and flexibility, which means it can wrap smoothly around curves — necklines, armholes, hems — without puckering or stretching out of shape. It’s the difference between a seam that looks handmade and one that looks engineered.
In garment manufacturing, bias binding does more than finish an edge. It:
- Reinforces stress points so seams don’t tear under movement
- Hides raw edges for a clean, professional interior finish
- Adds structure to curved lines that straight-grain fabric simply can’t follow
- Extends the garment’s lifespan, which is exactly why a well-made LBD from ten years ago can still look as sharp as the day you bought it
It’s a small detail with an outsized effect on perceived quality — the kind of thing a customer can’t always name, but instantly feels when they try on a dress that’s been finished properly.
From Sewing Room to Factory Floor
Home sewists can easily cut bias tape by hand. A simple fold, a quick press with an iron, and they’re done. But scale that up to a commercial factory. Imagine producing thousands of little black dresses every single season.
At that volume, manual cutting fails instantly. Speed drops. Fabric waste spikes. Consistency disappears completely. Manufacturers need a real engineered solution.
That’s where Svegea of Sweden enters the picture. We’ve spent decades perfecting industrial bias binding systems.
Engineers built Svegea’s Bias System specifically for garment manufacturing automation. At full production scale, it transforms massive fabric rolls into continuously sewn bias binding.
The process starts fast. First, the Tube Sewing Unit transforms open fabric into a continuous tubular piece. Next, the Bias Cutter and Winder opens and rewinds the material into an open-width roll. This prepares the fabric for precise slitting. The system handles everything smoothly, cutting delicate 6mm trims as easily as wide structural bindings for heavy fabrics.
The result? Perfect bias binding from the first meter to the ten-thousandth. No manual process can compete with that level of accuracy.
Why This Matters Beyond the LBD
Bias binding isn’t just for little black dresses. It shows up everywhere garments need clean, durable, curve-friendly finishes. You’ll find it on blouses, activewear, and children’s clothing. It even elevates non-apparel items like bags and home textiles.
Still, the classic LBD remains the ultimate quality test. Buyers expect to wear it for years. Its dark color exposes every single flaw in construction, leaving zero room for sloppy seams.
That’s what separates cheap clothing from true quality. One piece looks nice on a hanger. The other still looks pristine after fifty washes.
It all comes down to finishing. Top manufacturers rely on precision textile cutting systems to guarantee flawless results every time.
The same logic applies across the entire factory floor. Modern facilities deploy collarette cutters for waistbands and roll slitters for large fabric rolls. Precision machinery eliminates human error, keeps waste low, and guarantees consistent quality across every batch.
The Takeaway
The next time you slip into a little black dress that fits like a dream—just like the day you bought it—you’re rocking pure engineering genius. That pristine neckline and those crisp, fray-free seams surviving a decade in rotation don’t happen by accident. Every iconic silhouette relies on high-precision manufacturing, where seamless consistency turns basic threads into forever fashion.
Svegea’s Bias System and cutting machines give garment manufacturers a distinct competitive advantage through unmatched precision.
The cutting room rarely gets the credit it deserves. Dyeing, weaving, and finishing tend to dominate the sustainability conversation. Yet, the cutting stage quietly determines how much of every roll actually becomes a garment — and how much becomes trim on the floor. At Svegea, we have spent decades building the machines that sit at exactly that point in the process. Over that time, we’ve watched “zero waste” shift from a nice-to-have talking point to a real production target. This article walks through why that shift matters and what it looks like in practice.
The Hidden Cost of the Cutting Room
Textile waste is a big number, and it keeps getting bigger. According to the UN Environment Programme, the fashion industry generates roughly 92 million tonnes of textile waste every year. If nothing changes, that figure will climb past 134 million tonnes by 2030. The Ellen MacArthur Foundation puts it even more starkly: factories landfill or burn the equivalent of one garbage truck of clothing every single second.
Most of that conversation focuses on what happens after a consumer wears and discards a garment. Fair enough — that is where the largest volumes sit. But a meaningful share of textile waste never reaches a consumer at all. Factory floors generate this waste during cutting, trimming, and slitting, long before workers sew a single stitch. Offcuts, mismatched widths, and torn edges from tension problems all add up. Multiply that by thousands of meters a day, and the scrap bin becomes a genuine line item, not a rounding error.
What “Zero Waste” Actually Means on the Factory Floor
Zero waste doesn’t mean zero scrap. Realistically, some trim loss is unavoidable in any cutting process. Instead, it means designing the workflow so that you minimize waste at every step, measure it consistently, and — wherever possible — recover rather than bin it. For manufacturers, that translates into three practical questions:
- How much material do you lose to trim, misalignment, or edge damage during cutting?
- How repeatable is that loss across shifts, operators, and fabric types?
- Where can better equipment, not just better habits, close the gap?
That third question is where the technology conversation begins, and it is the one we spend most of our time thinking about.
Where Precision Cutting Technology Makes the Difference
Fabric doesn’t behave the same way twice. Tension varies by fibre, roll, humidity, and even the time of day. When a machine can’t compensate for that variability, the operator ends up compensating instead — usually by cutting a little wide “to be safe.” That habit, repeated across a full production run, is one of the most common sources of avoidable scrap in a cutting room.
Automated, electronically controlled cutting systems close this exact gap. Precise tension regulation keeps fabric feeding evenly, so the blade meets the material at a consistent width instead of a guessed one. Preset cut-width recipes remove the manual recalibration that eats into a shift’s productive time. Meanwhile, photocell edge alignment catches drift before it turns into a rejected panel. On the slitting side, PLC-controlled systems with stored cutting programs mean a changeover doesn’t require re-learning the machine from scratch. This cuts down on the “test cuts” that used to go straight into the scrap pile.
None of this is theoretical for us. It is the engineering problem we have worked on since 1952, first with collarette band-cutting machines and later across bias binding and roll-slitting equipment. Every refinement — a floating tension arm here, an automatic blade sharpener there — exists because a manufacturer somewhere told us their waste percentage was too high and asked what we could do about it.
Practical Steps Manufacturers Can Take This Quarter
Reducing cutting-room waste doesn’t require a full equipment overhaul to start. A few steps tend to produce results quickly:
1. Audit trim loss by fabric type, not just by line. Knits, wovens, and bias-cut materials behave differently, and averaging them together hides where the real losses sit.
2. Track waste as a percentage of output and review it weekly rather than quarterly. You can catch small drifts more easily — and fix them more cheaply — before they become the new normal.
3. Standardize cut-width settings across shifts so the outcome doesn’t depend on which operator runs the machine that day.
4. Service blades and tension systems on a schedule, not just when a problem shows up. A dull blade or a slack tension arm is a slow, invisible source of scrap.
5. Treat offcuts as an input, not an ending. Even if you haven’t built recycling into the workflow yet, sorting scrap by fibre type keeps that option open for later.
Individually, these steps sound modest. Together, over a year of production, they tend to move the needle more than most manufacturers expect.
Looking Ahead
The pressure on manufacturers to reduce material waste isn’t going away. If anything, tightening EU extended producer responsibility rules and growing retailer sustainability requirements are turning it into a compliance issue as much as a cost issue. Organizations like Textile Exchange continue to push the industry toward circularity. The manufacturers who get ahead of that curve, rather than reacting to it, tend to be the ones with cutting-room data already in hand.
We don’t think there’s a single fix for textile waste — it is a supply chain problem, and it needs supply chain-wide solutions. But the cutting room is one of the few places where a manufacturer has direct, immediate control over how much material becomes product versus how much becomes scrap. It is worth treating that way.
If your team is looking at cutting-room waste numbers and wondering what is realistic to improve, we are happy to talk through it. Reach out to Håkan Steene at h.steene@svegea.se for a waste-reduction consultation — no pitch, just a conversation about where the losses might be coming from.
—
Svegea of Sweden has designed and manufactured band-cutting, bias binding, and roll-slitting machinery since 1952. Learn more at svegea.se.
The Silent Language of Textiles
TL;DR: Touch is the first sense you ever develop, and fabric never stops talking to it. Long after you’ve stopped noticing color or cut, texture is still quietly running the show, calming a classroom, steadying a hospital ward, convincing a hotel guest they’ve arrived somewhere special. The science backs this up. So does the machinery that keeps a fabric’s feel consistent, batch after batch.
Touch Talks First, and It Never Really Stops
Run your hand across cashmere, then linen, then a coarse wool blanket. You don’t need a vocabulary lesson to know how each one makes you feel. Your body reacts before your brain finishes the sentence.
That’s not a coincidence. It’s a nine-month head start.
Touch is the first sense to develop in the womb, arriving around the eighth week of gestation, well before sight, hearing, or the ability to have an opinion about anything. Sensory receptors wake up first around the mouth and nose, then spread across the rest of the body over the following weeks. By the time a baby takes its first breath, touch already has months of practice logged. Fabric just keeps that conversation going.
Why Texture Beats Color to the Punch
Marketing teams love a good color story, and fair enough, color is loud and photogenic. But texture works in a quieter room: your nervous system, which reacts before your conscious mind gets a vote.
A 2024 study in PLOS ONE measured how tactile sensitivity shapes the way people rate fabric texture, confirming what mills have long suspected by feel alone: touch perception can be measured and predicted, not just guessed at.
Research published in the Spanish Journal of Marketing pushed the point further. After interviewing industry experts, the authors found that of the four qualities people notice by touch- texture, weight, temperature, and hardness- texture dominates how a product gets judged in someone’s hands. Shoppers decide with their fingertips. Their brains just write the caption afterward.
Where This Actually Plays Out
Picture a classroom in soft, breathable uniforms. Kids fidget less and focus more, because nothing scratchy is competing for their attention. Picture a hospital bed dressed in gentle linens instead of stiff, clinical ones. Shoulders drop a little faster. Picture a five-star hotel robe with real weight to it, sheets with a thread count you can feel before anyone announces the number. The room has already made its case before a single staff member says a word.
None of that happens by accident. It happens because someone understood that texture does emotional work whether a brand plans for it or not.
A World Woven in Texture
Travel far enough and texture starts speaking in dialects. Silk carries centuries of ceremony in Japan. Kente cloth, hand-woven in raised patterns across West Africa, tells stories of heritage and status that a photo alone can’t capture. Dense wool in Scandinavia is less a style choice than a survival strategy that eventually became culture, resilience spun into every fiber to get through a brutal winter.
These aren’t just materials. They’re identities, worn on the body and handed down.
The Blind Spot Nobody’s Solved Yet
E-commerce cracked color, cracked fit charts, mostly cracked video. It has not cracked touch. Researchers testing simulated haptic feedback in online apparel shopping found that screens still can’t replicate the confidence a customer gets from actually handling a fabric. Until touchscreens catch up, the only honest way to sell texture online is to describe it relentlessly: fiber content, weight, weave, finish, and photography that doesn’t oversell the hand-feel it can’t actually deliver.
The Unglamorous Part Nobody Photographs
Here’s the part that never makes the mood board: none of the feelings above survive an inconsistent production line. A designer can imagine the perfect hand-feel for a fabric, but if the machinery behind it drifts from batch to batch, that feeling never reaches the person wearing it.
That’s the role Svegea of Sweden plays, and it’s a deliberately unglamorous one. We don’t design the emotional experience of a textile; the manufacturers do that. What precision engineering does is make sure the texture a designer imagined is the texture that actually ships, consistently, so mills can spend their energy on the parts that require imagination instead of fighting variance on the floor.
The Actual Point
Stop designing only for how a fabric photographs. Start designing for how it will feel against skin, in the middle of an ordinary Tuesday, when nobody’s paying attention and the fabric is doing its job anyway. Texture is already telling a story. The only real choice is whether you’re the one writing it.
To talk through what consistent, imagination-ready production could look like for your line, reach out to Håkan Steene directly at h.steene@svegea.se, or visit www.svegea.se.